
What Is the Work of an Insert in CNC Turning Machine?
The insert in a CNC turning machine is the only part that touches the chip. It shears metal, breaks the chip, sets the surface finish and absorbs the heat. This page explains what that insert actually does, where its limits sit, and how to read a failure before it ruins a batch.
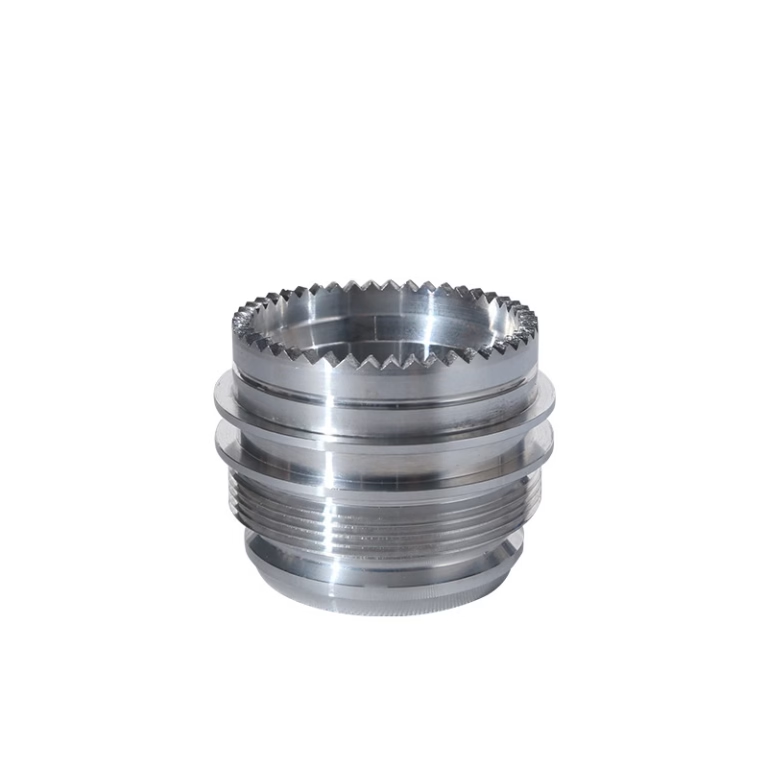
The insert in CNC turning machine does four jobs at once
A turning insert is a replaceable, usually indexable tip clamped into a tool holder. The holder gives it position and rigidity. The insert does the cutting. When the spindle rotates the workpiece, the insert is fed along a programmed path and shears material off as a chip. That single contact point sets the diameter, the surface finish and the cycle time on the part.
The first job is material removal. Flank and rake faces meet at the cutting edge, and the edge shears metal instead of scraping it. Cutting speed, feed and depth of cut decide how fast that happens. On a 6061-T6 aluminum shaft, 200–350 m/min and 0.15–0.25 mm/rev is a normal starting window. On 316 stainless, drop to 120–180 m/min or the edge will not survive the pass.
The second job is chip formation. A chip that curls tight and breaks short is a chip that leaves the cutting zone. A chip that runs long and stringy wraps the workpiece and stops the cycle. Chipbreaker grooves on the rake face are machined for exactly this reason, and they only work inside a feed range. Feed too light and the chip rubs. Feed too heavy and the breaker edge can chip.
The third job is surface generation. The nose radius and any wiper flat are copied onto the part as the tool feeds across it. A 0.8 mm nose radius at 0.2 mm/rev leaves a cleaner finish than a 0.4 mm radius at the same feed. The fourth job is heat management. Most of the heat leaves with the chip, but the edge still sees 700–1,000 °C in steel. The coating and substrate have to survive that, pass after pass.
How insert geometry and grade change the work
An insert is described by its shape, relief angle, tolerance class, fixing method and nose radius. A CNMG 120408 is an 80° rhombic insert, negative rake, 0.8 mm nose radius. A DCMT 070204 is a 55° rhombic, positive rake, 0.4 mm radius. The first is strong and suits roughing. The second has less material behind the edge and suits profiling and finishing where tool pressure must stay low.
Grade covers substrate and coating. A tough carbide substrate with a thin PVD coating resists chipping on interrupted cuts. A harder substrate with a thick CVD coating resists flank wear on continuous cuts at high speed. Pick wrong and you get either edge chipping or a wear land that grows faster than planned. Both show up as a size drift before the edge looks visibly broken.
Chipbreaker geometry is chosen with the depth of cut, not the material alone. A light-cutting breaker on a 3 mm depth of cut will not curl the chip. A heavy-duty breaker on a 0.5 mm finishing pass forces the chip into the edge. On bar work with a small diameter, the tool overhang also matters. Long overhang turns a stable insert into a chattering one.
Other insert materials exist for a reason. Ceramic inserts run dry at 400–800 m/min on cast iron and hardened steel. CBN handles hardened steel above 45 HRC. PCD is used on aluminum and composites where built-up edge is the main enemy. None of them replace carbide for general turning. They cover the cases where carbide wears out in minutes.
What wear on the insert tells you
Flank wear is normal. A uniform wear land of 0.2–0.3 mm on the flank is a sign the grade and speed match the job. When that land reaches 0.4 mm, the edge starts rubbing and the surface finish drops. Size begins to drift. Change the edge at the interval your shop has set, not when the part goes out of tolerance.
Crater wear is different. It eats the rake face behind the edge and is driven by heat and diffusion. It shows up at high cutting speed and in steels with a lot of titanium or nickel. The fix is lower speed or a more heat-resistant coating. If you only see crater wear, your speed is too high for that grade.
Chipping and thermal cracking are the other two common modes. Chipping comes from interrupted cuts, hard spots in the casting or a weak setup. Thermal cracks run perpendicular to the cutting edge and come from rapid heating and cooling, often when coolant is aimed at a hot edge on a heavy cut. On a cast iron face with a hard skin, take a first pass deep enough to get under the skin rather than skimming it.
Built-up edge is not wear, but it behaves like it. Aluminum and soft low-carbon steel can weld material onto the edge, then tear it away and take carbide with it. Higher speed, a sharper positive edge or a PCD insert usually clears it. If the finish looks smeared rather than torn, suspect built-up edge before you change the feed.
Matching the insert to the turning operation
Typical starting points for common turning cases
| Operation | Insert type | Speed range | Watch for |
|---|---|---|---|
| Rough OD turning, steel | CNMG 120408, CVD grade | 150–250 m/min | Flank wear and size drift |
| Finishing OD, stainless | DCMT 070204, PVD grade | 120–180 m/min | Notching and built-up edge |
| Aluminum shafts | Positive rake, polished, PCD option | 200–350 m/min | Built-up edge and smeared finish |
| Interrupted cast iron | Tough substrate, heavy breaker | 180–280 m/min | Chipping on the hard skin |
| Hardened steel above 45 HRC | CBN, negative rake | 100–200 m/min | Thermal cracking if cooled hard |
| Small diameter bar work | Positive rake, small nose radius | 20–40% below normal | Chatter from long overhang |
| Grooving and parting | Narrow grooving insert, ground edge | 40–60% of turning speed | Chip packing in the groove |
Pick by the cut, not by the catalog
If the cut is continuous and the priority is edge life, choose a harder grade with a thicker coating and run at the higher end of the speed window. If the cut is interrupted or the setup is weak, choose a tougher substrate with a positive edge and accept lower speed. One insert cannot do both well.
Turning insert questions engineers ask
How do I know the insert in a CNC turning machine is worn out?
Measure the flank wear land. Around 0.2–0.3 mm the edge is still cutting cleanly. Past 0.4 mm the edge rubs, the finish gets rougher and the diameter starts to drift.
Do not wait for a visibly broken edge. On a production run, a size drift of 0.02 mm usually appears before the insert looks bad in the holder.
Why does my chip come out long and stringy?
Usually the feed is too low for the chipbreaker geometry. Each breaker has a working feed range, and below it the chip slides along the rake face instead of curling.
Raise the feed in steps of 0.05 mm/rev until the chip breaks into short C or 6 shapes. If the breaker is wrong for the depth of cut, no feed change will fix it.
Can I use one insert grade for aluminum and stainless steel?
Not well. Aluminum wants a sharp positive edge and often a polished or PCD tip to stop built-up edge. Stainless wants a tougher substrate with a PVD coating and a stronger edge.
Keep separate inserts and separate holders for the two families. Swapping one edge between them usually costs more in scrap than the extra insert costs.
Does coolant help or hurt the insert?
On continuous cuts in steel, flood coolant helps edge life. On interrupted cuts or with ceramic inserts, it can cause thermal cracking.
If you see cracks running perpendicular to the edge, the coolant is the likely cause. Reduce it or run dry and let the chip carry the heat.
How many edges can I get from one insert?
It depends on shape. A CNMG 120408 has four usable corners. A DCMT 070204 has two. A triangle has three.
Track the number of parts per edge in your setup sheet. Once you know that number, edge changes become scheduled, not reactive.
When is a wiper insert worth the extra cost?
When the finish callout is Ra 0.8–1.6 μm and you want to reach it without a second pass at low feed. A wiper flat lets you keep the feed up and still hit the finish.
It is not worth it on roughing or on parts with interrupted surfaces, where the flat edge chips more easily than a standard radius.
Send us the drawing and the material
We turn prototypes and production runs on 127 CNC machines, with 100% inspection before shipment and no minimum order quantity.
12-hour quote100% inspectionNo MOQNDA on request
More from the shop floor
We publish setup notes, tooling trials and inspection data from the factory floor.











