Precision 5 Axis CNC Machining: What Engineers Should Check First
This guide is for design and sourcing engineers comparing quotes for precision 5 axis cnc machining. It covers the seven checks that decide whether a part comes back on print: tolerance, setup count, work envelope, tool access, inspection data, certifications and quote completeness. Read it before you send the RFQ.
In this article
- 1
- 2
- 3
- 4
- 5
- 6
- 7
- 8
- 9
Key takeaways
Which process fits your part
Use this when you are deciding between 3-axis, 4-axis and precision 5 axis cnc machining for the same geometry.
| Process | Best for | Limits | Setup count |
|---|---|---|---|
| 3-axis milling | Prismatic parts, one face per setup | No undercut access, deep pockets need long tools | 2–5 |
| 4-axis milling | Cylindrical parts with holes around the axis | Limited tilt, compound angles need fixtures | 1–3 |
| 5-axis indexed | Multi-face parts, tight hole-to-hole position | Tool axis fixed per cut, not for free-form surfaces | 1–2 |
| 5-axis simultaneous | Impellers, blades, contoured pockets, deep ribs | Higher programming cost, needs rigid fixturing | 1 |
| Mill-turn | Shafts and housings with turned and milled features | Smaller work envelope than a gantry mill | 1–2 |
The short version
Pick the shop that can explain its setup count, inspection method and quote breakdown. Machine specs are easy to list; a process plan is the only proof that precision 5 axis cnc machining will hold on your part.
Tolerance and how it is achieved
A printed tolerance of ±0.005 mm means nothing on its own. Ask what machine holds it and how the shop verifies it. On a simultaneous 5-axis center, the rotary axes introduce their own positioning error, so the machine has to be calibrated on a schedule, not once at install.
Temperature matters as much as the machine. A shop that machines aluminum in an uncontrolled bay will see the part grow as the spindle warms up. Look for a plant that keeps the finishing area stable and lets roughing parts cool before the final pass.
Check whether the tolerance applies to the whole part or only to a set of critical features. Many quotes list a general tolerance on the drawing and a tighter one for datum holes. That distinction changes the fixturing plan and the price.
For tight features, ask for the measurement method. A CMM with a stated uncertainty is a different claim from a caliper reading. If the shop cannot say which instrument is used, the number on the quote is a hope.
- 1±0.005 mm typicalHeld on critical features on calibrated 5-axis centers
- 2Datum strategyAsk which datums are machined in the same setup
- 3Thermal controlRough, cool, then finish to avoid growth error
Setup count and where the error comes from
Every time a part leaves the fixture, the new zero has to be established again. On a three-axis machine a housing with holes on four sides can take five setups. Each re-clamp adds positional error that no amount of machine accuracy can remove.
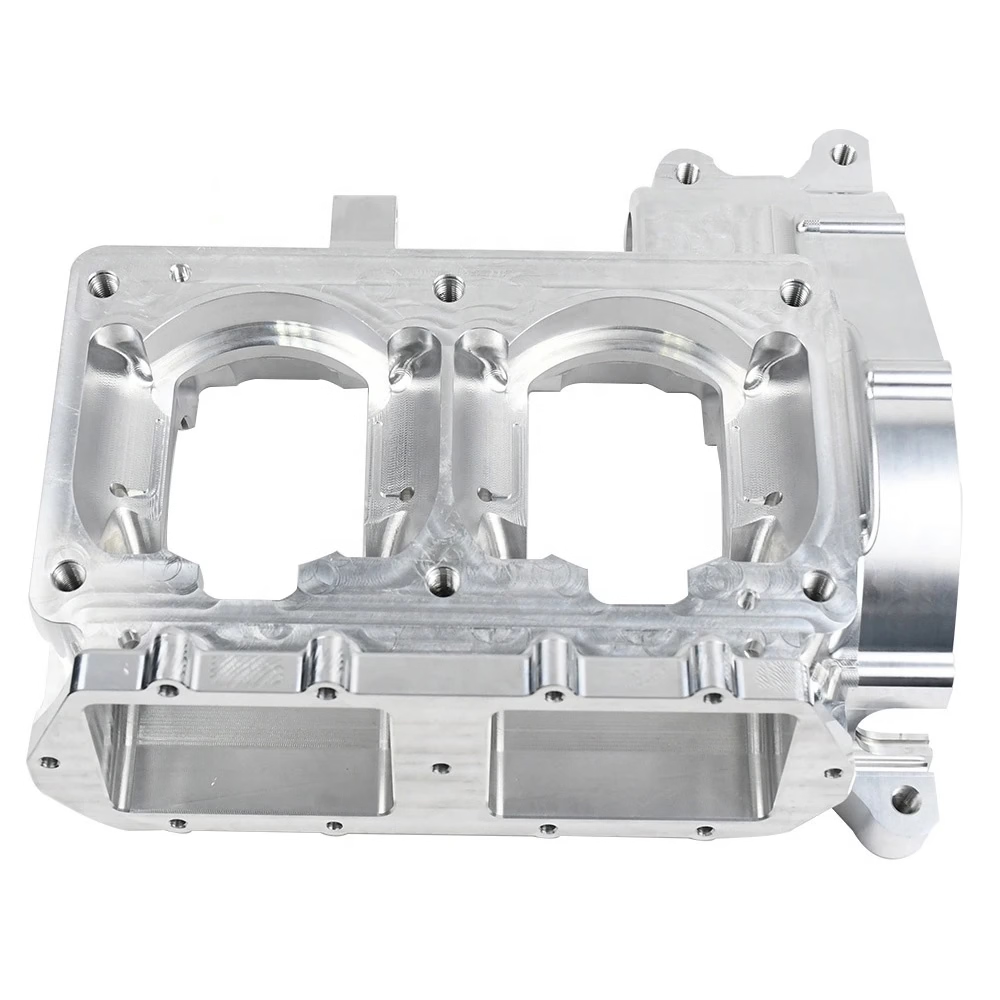
Precision 5 axis cnc machining collapses those setups into one or two. The rotary table presents a new face to the tool without unclamping. Datum features stay valid, and hole-to-hole position across faces becomes a function of the machine, not the operator.
In practice, the limit is tool access, not the number of axes. A deep bore that needs a long, thin tool will chatter regardless of the machine. The shop has to choose between a shorter tool and a different access angle, and that choice shows up in the process plan.
Ask the shop to list the setups in the quote. If the number is vague, you will find out at first article when the cross-face position is out.
- 1One setup when possibleKeeps datums valid across all machined faces
- 2Rigidity beats reachShort tools hold finish; long tools chatter
- 3Ask for the setup listA written plan exposes hidden re-clamping
Work envelope and part orientation
A machine spec of 4,000 × 400 × 150 mm describes linear travel, not the size of part you can cut. Once the part is tilted to reach an undercut, the corner of the stock can hit the table or the spindle head. The usable envelope shrinks.
Rotary table size is the other half of the answer. A Ø400 mm table suits parts up to roughly that diameter with clearance for the fixture. Larger parts need a trunnion or a different machine class, and that changes both price and availability.
For long parts, ask how the shop supports the overhang. A 4,000 mm travel machine still needs steady support or the part deflects under cutting load. Support strategy is a process decision, not a machine spec.
Send a 3D model, not a bounding box. A box that fits on paper can still fail when the tool has to reach an internal corner at a compound angle.
- 1Ø400 mm rotary tableSuits parts near that diameter with fixture clearance
- 2Tilted parts shrink the envelopeCheck clearance at the worst cutter angle
- 3Long parts need supportOverhang deflects even on a 4,000 mm machine
Tool access, surface finish and programming
Simultaneous 5-axis work lets the tool stay normal to a contoured surface. That keeps the step-over consistent and the finish even. On a sculpted surface, a fixed tool axis produces witness lines where the effective cutter contact changes.
The trade-off is programming time and verification. A simultaneous toolpath has to be simulated for collision against holder, table and part. Shops that skip simulation find crashes at the machine, and that risk is priced into the quote one way or another.
Surface finish ranges are a useful filter. As-machined finishes sit around Ra 1.6–3.2 μm. A high-quality machined finish lands at Ra 0.8–1.6 μm. Fine finishes down to Ra 0.2–0.8 μm usually need a separate finishing pass or a secondary operation.
If the drawing calls for a cosmetic surface, say so at quote time. A part that is dimensionally correct can still be rejected for tool marks, and rework on a finished contoured surface is expensive.
- 1Normal tool axisEven step-over on free-form surfaces
- 2Simulation is not optionalCollision checks on holder, table and part
- 3Finish bandsAs-machined Ra 1.6–3.2 μm; fine Ra 0.2–0.8 μm
Certifications, inspection and paperwork
Certifications tell you which process controls already exist. ISO 9001:2015 covers the general quality system. IATF 16949:2016 adds automotive process discipline such as PPAP-style documentation and traceability. ISO 13485:2016 covers medical device manufacturing, and ISO 27001:2022 covers information security for your files.
Inspection is the part buyers under-specify most often. Ask whether the shop inspects 100% of the lot before shipment, and whether raw material check, in-process monitoring and final inspection are separate steps. Reports on request are useful only if you actually request them.
Material traceability matters for aerospace, medical and automotive parts. Ask for the mill certificate and confirm the heat number follows the part through the shop. Without that link, a material substitution is invisible until it fails.
For confidential work, confirm that uploads are handled under NDA on request. Send the NDA before the model, not after the order.
- 1Four certificationsISO 9001, IATF 16949, ISO 13485, ISO 27001
- 2100% inspectionBefore shipment, with reports on request
- 3TraceabilityMill cert and heat number tied to the lot
Quote completeness, MOQ and lead time
A quote that lists only a price per part is not comparable to one that lists material, machining, finishing, inspection and freight separately. Ask for the breakdown so you can see what changes if you drop the anodize or relax a tolerance.
Minimum order quantity is a real filter. Some shops will not quote below a few hundred pieces, which makes prototype iteration slow. Others accept a single part and scale to 10,000+ runs. For a first article, the second model is far more useful.
Lead time has three parts: quote turnaround, production start and shipping. A shop that returns a quotation and free DFM analysis within 12 hours and can start production within 24 hours keeps a design loop short. Parts shipping in 3–5 days after that is a working rhythm, not a promise for every part.
Treat any delivery promise without a stated assumption as noise. Ask what the lead time assumes about material availability, finishing and fixture build.
- 1Line-item quotesMaterial, machining, finish, inspection, freight
- 2No MOQOne prototype up to 10,000+ part runs
- 3Fast loopQuote and DFM in 12 hours, start in 24 hours
Step by step: how to run the comparison
Use the same inputs for every shop so the quotes line up.
- 1Send a 3D model plus a 2D drawingThe model carries geometry; the drawing carries datums, tolerances and finish callouts. A model alone leaves the critical features to guesswork.
- 2State the critical featuresList the dimensions that actually control function, with their tolerance. Say which surfaces are cosmetic. This is where ±0.005 mm applies and where it does not.
- 3Ask for the setup count and process planOne or two setups for a multi-face part is a good sign. If the shop cannot describe the fixturing, the tolerance claim is thin.
- 4Confirm material and finish specificationGive the alloy grade, not just aluminum. 6061-T6 and 7075 machine differently. Name the finish thickness range, such as anodize type and color.
- 5Request inspection scopeAsk which features are measured, on what equipment, and whether a report ships with the lot. Add first article inspection for a new design.
- 6Compare quotes line by lineNormalize for quantity, material, finish and inspection. A low price with no inspection line is not the same product.
- 7Run one prototype before the production orderCheck the cross-face position and the surface finish on the real part. Fix the process on one piece, not on a thousand.
Questions engineers ask before ordering
When is 3-axis machining enough instead of 5-axis?
If all machined features are reachable from one or two orthogonal directions, a 3-axis machine with simple fixtures will hold tolerance and cost less.
Move to 5-axis when the part has compound angles, undercuts, deep contoured pockets, or features on several faces that must stay in position relative to each other.
Does more axes always mean a better part?
No. A simultaneous 5-axis toolpath is harder to verify and can produce a worse finish if the fixturing is not rigid.
The gain comes from fewer setups and better tool orientation. If the geometry does not need either, the extra programming cost buys nothing.
What tolerance can I realistically expect on a 5-axis part?
±0.005 mm is achievable on critical features when the machine is calibrated, the finishing area is thermally stable and the part is measured properly.
On long parts or thin walls, deflection and thermal growth dominate. Discuss the feature, not the general tolerance block.
How should I specify surface finish?
Give a numeric Ra range for functional surfaces: Ra 0.8–1.6 μm for a high-quality machined finish, Ra 1.6–3.2 μm as-machined.
Name cosmetic surfaces separately and say whether tool marks are acceptable. Vague notes like 'smooth' get interpreted differently at every shop.
Which certifications should I look for?
ISO 9001:2015 is the baseline for any supplier. Add IATF 16949:2016 for automotive parts, ISO 13485:2016 for medical devices, and ISO 27001:2022 if your drawings and models are sensitive.
Ask for the certificate scope, not just the logo. A certificate that does not cover your process is not evidence.
Can I order a single prototype?
Yes. A supplier with no minimum order quantity can run one part and then scale the same process to 10,000+ runs.
Use the prototype to verify datum strategy, finish and fit. Approving production tooling before the first article is the most expensive mistake in this workflow.
Send the model, get a process plan back
Share your 3D model and drawing. We return a quotation and free DFM analysis within 12 hours, with the setup and inspection plan written out.
12-hour quote100% inspectionNo MOQNDA on request
More from GreatLight
We publish setup notes, tooling trials and inspection data from the factory floor.