GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Nickel Superalloy Machining

Inconel CNC Machining for High-Temperature Parts

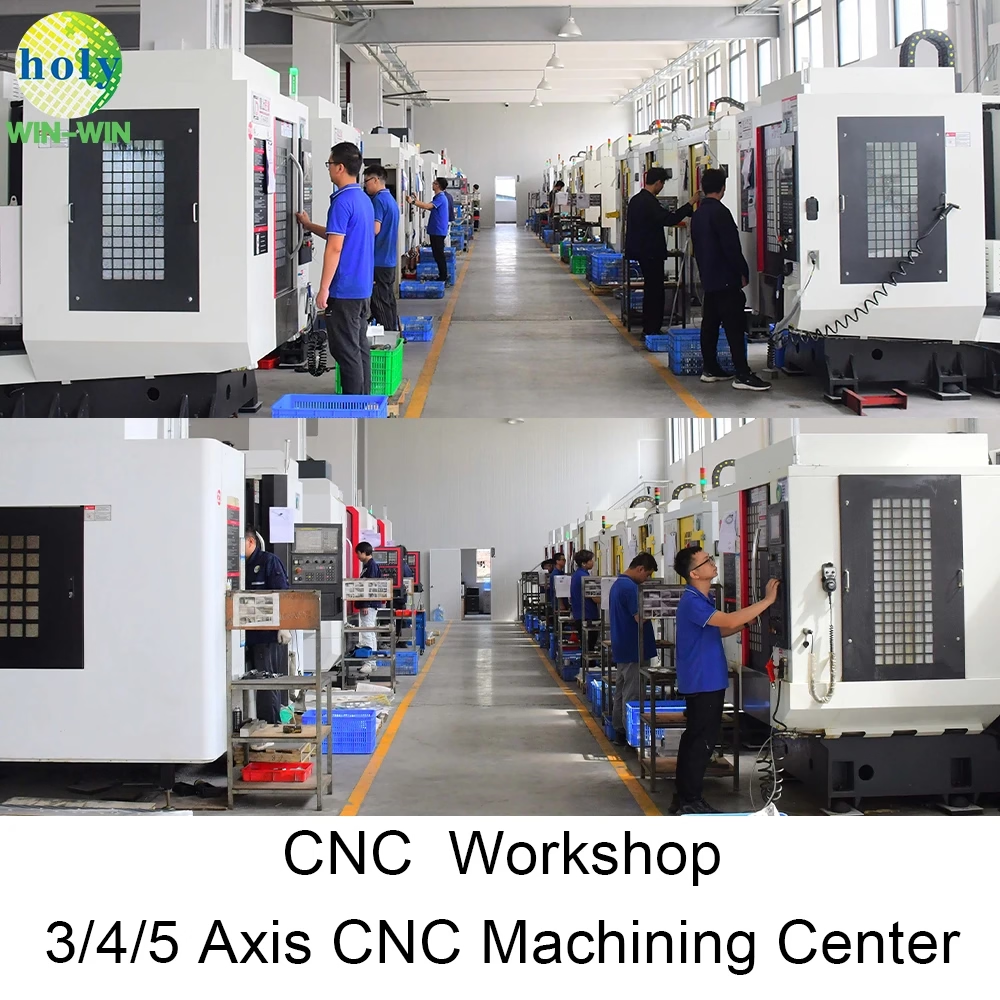
Inconel is a nickel superalloy that work-hardens fast and holds heat at the cutting edge. We machine it on 16 simultaneous five-axis centers with ceramic and carbide tooling, controlled ramp entries and heavy coolant. Prototype to 10,000+ parts, ±0.005 mm.

Inconel 625 / 71816 five-axis centers±0.005 mmRa 0.8–1.6 μmNo minimum order12-hour quote
inconel-cnc-machining
2011Machining nickel alloys since
16Simultaneous 5-axis centers
±0.005 mmAchievable tolerance
12 hQuote and free DFM analysis
Where superalloy jobs go wrong

Four Failure Patterns We See Every Week

If any of these are familiar, the problem is usually the process, not the drawing.

01

Tool life collapses after two parts

Inconel 718 work-hardens the moment the cutter rubs instead of bites. A light feed, a dwell in the cut, or a worn insert raises the surface hardness and the next pass destroys the edge. Ten inserts per part is a feed and speed problem, not a material problem.

02

Chatter on thin walls and flanges

Nickel alloys push back about twice as hard as 4140. A 1.5 mm wall on a turbine bracket will sing at the wrong radial engagement, and the finish turns into a witness-mark map. Most shops slow the spindle down, which makes it worse.

03

Holes come out undersize after cooling

Inconel holds heat in the chip and in the part. A hole milled to nominal size while hot can close up 0.02–0.03 mm once it reaches room temperature. If your gauge says the bore is small, the inspection may have happened too early.

04

Quotes come back late, or not at all

Many shops avoid nickel alloys because of the cycle time. You send a drawing, wait a week, and get a number with no explanation of how it was built. Ten days lost before a single chip is cut.

How we run the cut

Process Control, Not Heroics

Three things decide whether an Inconel part comes off the machine on size: heat, tool engagement, and how the part is held.

**Option 1 (Concise & Direct):**
Thermal control

Heat Is the First Variable

Inconel conducts heat poorly, so most of the cutting temperature stays in the tool and the workpiece. We run high-pressure coolant directly at the insert, use positive rake geometry with a real edge hone, and take a deep enough axial cut to stay under the hardened layer left by the previous pass.

That combination is why insert changes are measured per shift rather than per part. On a 718 housing we hold the same edge through a full batch instead of stopping every few pieces.

  • 1
    Through-spindle coolantDirected at the cutting edge, not the chip
  • 2
    Ramp entries onlyNo straight-plunge into a work-hardened surface
  • 3
    Depth above the hard layerAvoids cutting the skin the last pass created

Get Instant Quote

**Option 1 (Concise & Direct):**
Geometry and setup

Five Axes Cut the Number of Setups

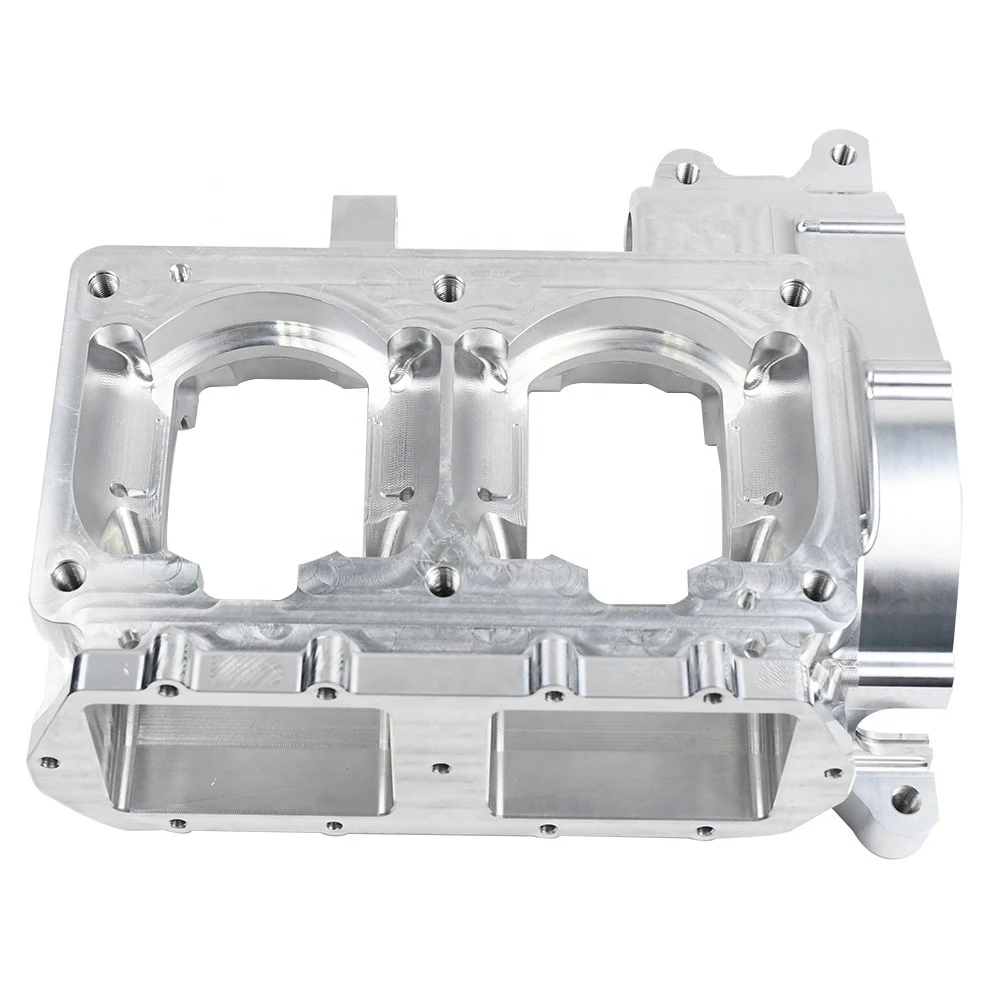
A turbine bracket or a manifold boss usually needs features on four or five faces. Splitting that across three-axis machines means three fixtures, three datums, and three chances to stack error. On a simultaneous five-axis center the part is located once and the tool reaches the rest.

The rotary table is Ø400 mm, and the large-format machines take work up to 4,000 × 400 × 150 mm. For long thin parts, we support the middle and cut in two stages so the released stress does not pull the part out of tolerance after unclamping.

  • 1
    One datum, many facesPosition error stays in a single setup
  • 2
    Ø400 mm rotary tableIndexing for complex prismatic parts
  • 3
    4,000 mm envelopeLong shafts and exhaust sections

Talk to an Engineer

Grade selection

Which Inconel Grade Fits the Job

Pick the grade from the service temperature and the corrosion environment, not from what is in stock.

GradeTypical serviceMachining note
Inconel 625Marine, chemical, exhaustTougher, gummier chips, lower speeds
Inconel 718Turbine, high-stress hot partsAge-hardenable, best strength at 700 °C
Inconel 600Furnace and heat-treat fixturesSofter, but still work-hardens quickly
Inconel 800Boiler and process tubingMachines closer to stainless than 718
What we build

Machining Services for Nickel Alloys

Same shop, same inspection route, whether the order is one prototype or a production run.

01

5-Axis CNC Machining

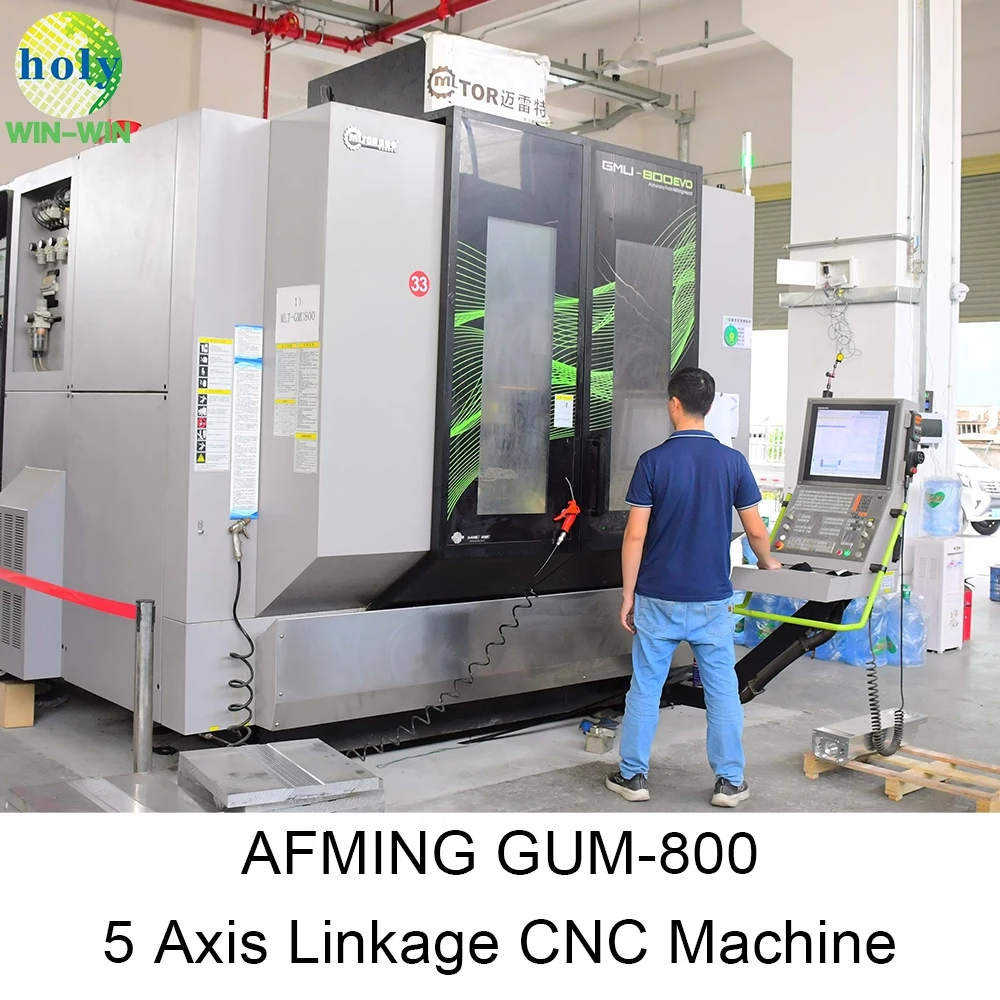
16 simultaneous five-axis centers for impellers, brackets and housings with features on multiple faces. One setup carries the datum through the whole part.

02

4-Axis and 3-Axis Milling

12 four-axis mills and 27 three-axis machines handle prismatic work, plates and fixtures where 5-axis reach is not needed. Lower cost per hour.

03

CNC Turning and Mill-Turn

16 mill-turn centers cut shafts, bushings and valve bodies. Turn and mill in one cycle so concentricity is held between the bore and the outside diameter.

04

Rapid Prototyping

Single-piece Inconel prototypes for fit checks and hot-fire trials. No minimum order quantity, so a one-off is a normal job here.

05

Surface Finishing

Bead blasting, tumbling, brushing and polishing. Laser marking with a minimum character height of 1.5 mm for traceability.

06

Inspection and Reporting

100% inspection before shipment. Raw material check, in-process monitoring, final inspection, with dimensional reports on request.

Capability

Equipment and Tolerances

Numbers you can hold us to.

ItemSpecificationNotes
General tolerance±0.005 mm / ±0.0002 inGrade and feature dependent
Fine finishRa 0.2–0.8 μmAdds cycle time on nickel alloys
High finishRa 0.8–1.6 μmStandard for sealing faces
As-machinedRa 1.6–3.2 μmNon-critical surfaces
Max part size4,000 mmLong shafts and exhaust sections
Rotary tableØ400 mmIndexing on 5-axis centers
Why GreatLight

Six Reasons Shops Send Us Nickel Work

Capacity, process control and paperwork.

15Y

Nickel alloys since 2011

Fifteen years of cutting high-temperature alloys, stainless and titanium. The speeds and feeds are not new to us.

127

High-precision CNC machines

127 machines across three wholly-owned plants in Dongguan and Singapore. Capacity is not the constraint on your lead time.

±0.005

Tolerance we hold

±0.005 mm on critical features, verified by in-process monitoring and final inspection before anything ships.

24 h

Production start

Quote and free DFM analysis within 12 hours. Production can start within 24 hours of approval.

99.99%

Qualification rate

Measured across shipped orders. Reportable on request for your quality file.

<2%

Historical late-delivery rate

Late delivery probability kept below 2% across past orders. Parts typically ship in 3–5 days.

7,600 m²Manufacturing space
150Technicians on staff
3Wholly-owned plants
ISO 9001IATF 16949, ISO 13485, ISO 27001
Industry Fit

What These Sectors Require, and What We Deliver

**Option 1 (Concise & Direct):**

Aerospace

Turbine brackets and hot-side hardware.

  • Inconel 718
  • ±0.005 mm
  • Full inspection report
**Option 1 (Concise & Direct):**

Automotive and EV

Exhaust and thermal-shield components.

  • Inconel 625
  • Ra 0.8–1.6 μm
  • IATF 16949 process
**Option 1 (Concise & Direct):**

Industrial Machinery

Furnace fixtures and high-temp valve bodies.

  • Inconel 600 / 800
  • 1 to 10,000+ parts
  • Material traceability
low volume manufacturing

New Energy

High-temperature process hardware.

  • Single prototype
  • No MOQ
  • 3–5 day shipment
FAQs

Questions Engineers Ask About Inconel

Can you machine Inconel 718 or 625?

Yes. Both grades run regularly on the five-axis and mill-turn centers. We also machine 600 and 800.

Send the grade with the drawing. Speed and feed differ enough between 625 and 718 that the quote changes if the grade is left open.

What tolerance can you hold on nickel alloys?

±0.005 mm (±0.0002 in) on critical features, with Ra 0.8–1.6 μm as the standard machined finish.

Inconel moves after cutting because of residual stress and heat. We hold the tight tolerance by leaving stock, letting the part stabilize, and finishing in a separate pass.

Do you need a minimum order quantity?

No. One prototype and a 10,000-part run go through the same process route.

That matters for nickel work, where the first article usually proves the fixture and the tool path before volume starts.

How fast can I get a quote and parts?

Quote and free DFM analysis come back within 12 hours. Production can start within 24 hours of approval.

Typical parts ship in 3–5 days. Cycle time on thick Inconel sections is longer than aluminum, so we flag that in the quote rather than after the fact.

How do you stop the part from warping?

Roughing leaves stock, the part is allowed to cool and relax, and finishing cuts the remaining material with lighter radial engagement.

On long or thin sections we support the middle and may cut in two stages so unclamping does not pull the part out of tolerance.

Which finishes are available?

Bead blasting, tumbling, brushing and polishing, plus laser marking and engraving with a minimum character height of 1.5 mm.

Electroless nickel and other plating can be arranged where the service environment calls for it. Anodizing does not apply to nickel alloys.

How is the material verified?

Raw material is checked on receipt, milling is monitored in process, and every part is inspected before shipment.

Mill certificates and dimensional reports are available on request for your quality file.

Can you sign an NDA?

Yes. Uploads are handled as confidential and an NDA is available on request before you send drawings.

For aerospace and medical programs we can route the job through the ISO 27001:2022 information-security process.

Send Your Inconel Drawing

Upload a STEP file and get a quote with free DFM analysis within 12 hours. No minimum order quantity, and every part is inspected before it ships.

12-hour quote100% inspectionNo minimum orderNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC