GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

CFRP machining

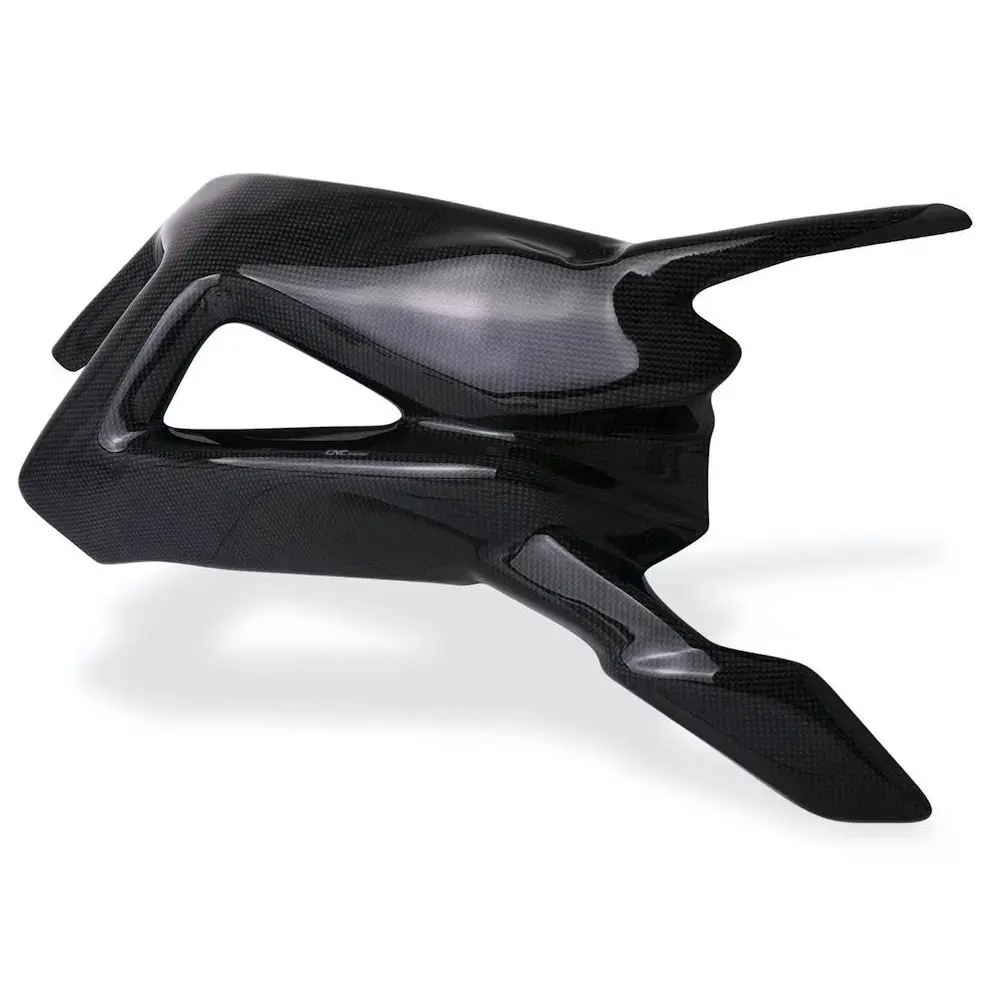
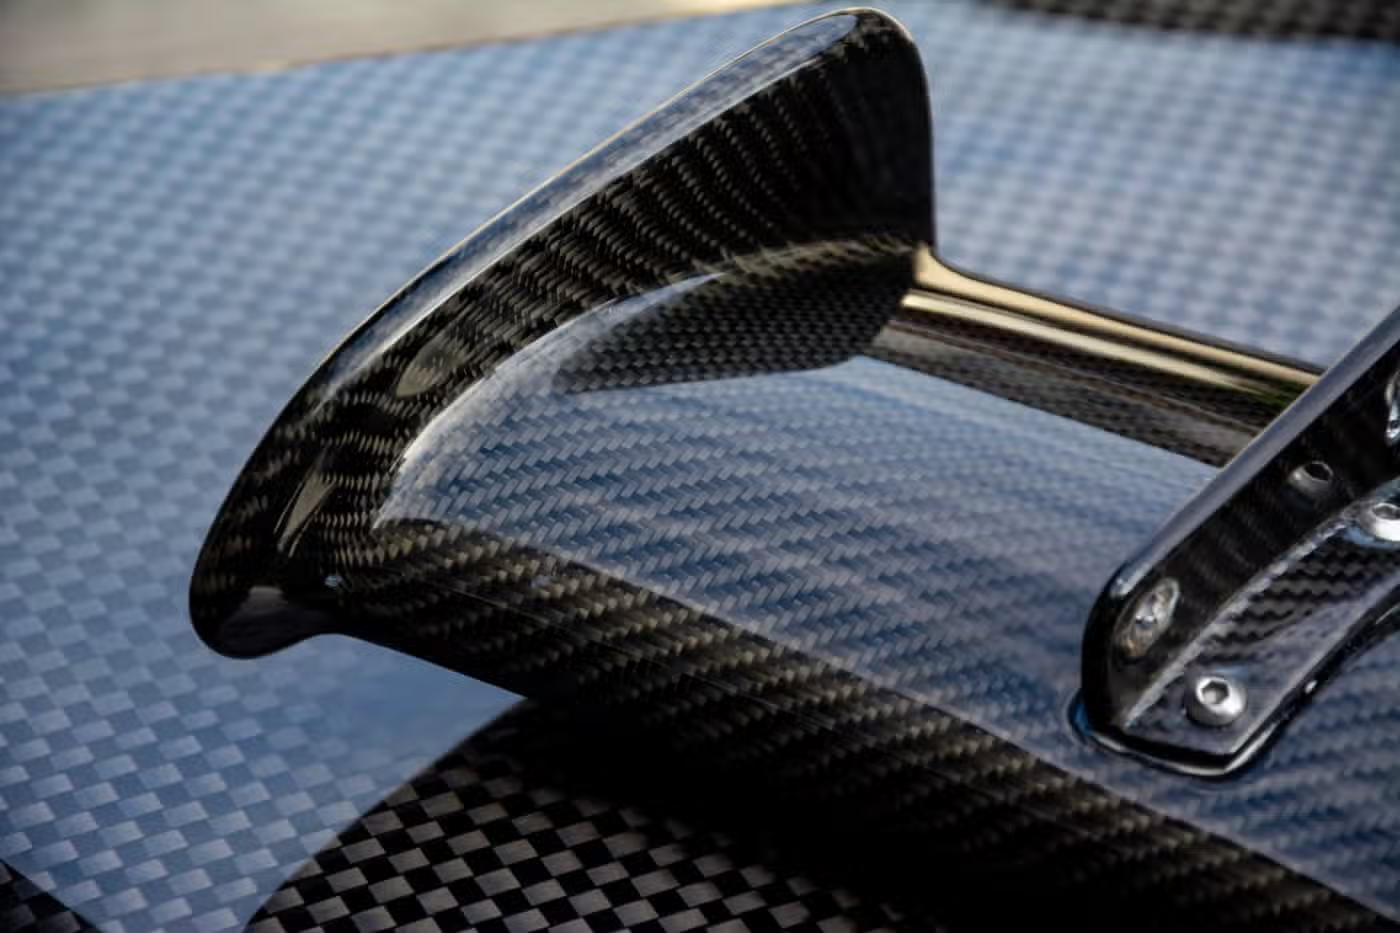
CNC Carbon Fiber Machining for Prototypes and Production

Laminated carbon fiber and CFRP parts machined on 5-axis centers. We hold ±0.005 mm, control dust at the spindle, and inspect every part before it ships. One prototype or a 10,000-piece run.

±0.005 mm tolerance16 five-axis centersUp to 4,000 mm3–5 day shipping
cnc-carbon-fiber
16Simultaneous 5-axis centers
±0.005 mmAchievable tolerance
4,000 mmMaximum part length
99.99%Qualification rate
Where it goes wrong

What Carbon Fiber Does to a Normal Machining Job

CFRP is not aluminium with a different color. It behaves differently at the cutter, and the failure modes show up late.

01

Do your edges come back frayed or delaminated?

A standard 2-flute end mill lifts the outer plies instead of shearing them. The top layer splinters, the bottom layer tears out, and the part fails cosmetic and structural checks. The fix is geometry and feed direction, not more spindle speed.

02

Are your holes drifting out of position after drilling?

Carbon dust is abrasive. It wears the drill margin within a few dozen holes, so hole size creeps and the drill walks. On a bolted joint that shows up as a stack-up error you cannot adjust out at assembly.

03

Is your shop air turning into a health and maintenance problem?

Dry CFRP dust is conductive and it does not settle. It shortens machine way life, clogs filters, and creates an exposure risk for operators. Wet cutting or sealed extraction has to be planned before the first cut, not after.

04

Did a quote come back with no tooling or setup detail?

Carbon work depends on ply orientation, layup thickness, and whether the part is net-shape molded or trimmed from a panel. A price without those assumptions is a number, not a plan. Expect it to move once the drawing is read properly.

How we machine it

Cutting CFRP Without Damaging the Laminate

Two things decide whether a carbon part comes off the machine good: tool geometry and how the dust is handled.

carbon fiber reinforced polymer 2024 material dominance
Tooling and strategy

Diamond-coated tools, climb cuts, and support on both faces

Carbon fiber reinforced polymer is abrasive and anisotropic. Strength runs along the fibers, so the cutter meets a hard matrix in one direction and a soft one in the other. We select diamond-coated end mills and burr-style routers, set climb milling as the default, and keep the part supported on both faces so the exit ply does not blow out.

For thin laminates under 2 mm, we back the part with a sacrificial plate and take light finish passes. For thicker stacks, we rough with lower helix tools and finish with a compression cutter that shears the top and bottom plies at the same time. Feed rates stay conservative. Burning the resin is worse than a slower cycle.

  • 1
    Diamond-coated toolingHolds an edge through abrasive CFRP instead of polishing away in a few parts.
  • 2
    Compression cuttersShear the top and bottom plies together, which limits delamination on both faces.
  • 3
    Climb millingDefault direction on carbon. Pushes the cut into the material rather than lifting plies.

Get Instant Quote

low volume manufacturing
Dust and finish

Extraction at the cut, then sealing the exposed edge

Carbon dust is the part of the job most shops underestimate. It is abrasive, conductive, and fine enough to travel through a shop. We run wet or mist-assisted cutting where the geometry allows, and local extraction at the spindle where it does not. Chips are collected rather than blown into the aisle.

A machined carbon edge leaves bare fibers exposed. They wick moisture and they fray with handling. Where the drawing calls for it, we seal cut edges with a compatible resin or apply a light finish, and we mask surfaces that must stay bondable. If your part bolts to metal, we can also machine isolating sleeves to keep the joint from galvanic corrosion.

  • 1
    Extraction at the spindleCaptures abrasive dust before it reaches ways, filters, or operators.
  • 2
    Edge sealingResin or finish on exposed cut edges to stop fraying and moisture wicking.
  • 3
    Isolation hardwareSleeves and washers that separate carbon from metal in bolted joints.

Get Instant Quote

Choosing a process

When Machining Beats Molding for Carbon Parts

Not every carbon part should be cut from a panel. This is how we usually decide.

SituationRecommended routeWhy
One prototype, complex 3D shape5-axis machining from laminateNo tooling cost, geometry changes are free
Flat bracket, holes and trim only3-axis routing from cured panelFastest and cheapest per part
Hollow or closed sectionMolded shell, then machined interfacesMachining cannot create internal voids
Run above 5,000 identical partsCompression mold with net-shape trimTooling pays back on cycle time
Tolerance under ±0.02 mm on a boreMachine the bore after layupCure shrinkage moves the hole, not the cutter
Cosmetic visible weave surfaceMachine from the back faceKeeps the show surface untouched
What we run

Carbon Fiber and Composite Machining Services

Carbon work sits inside a wider machining shop, so interfaces, hardware, and fixtures can be made in the same plant.

01

5-Axis Carbon Fiber Machining

Contoured trim, angled holes, and compound surfaces cut in one setup on 16 simultaneous 5-axis centers. Fewer setups means fewer chances to chip an edge.

02

3-Axis Routing and Trimming

Flat panels, brackets, and plates routed from cured laminate. The practical choice for simple geometry and short lead times on 27 three-axis machines.

03

CNC Milling and Turning

Metal and plastic hardware that pairs with carbon assemblies: bushings, inserts, spacers, and adapter plates held to the same tolerance.

04

Rapid Prototyping

Machined carbon and composite prototypes for fit checks before you commit to tooling. Quotation and free DFM analysis within 12 hours.

05

Surface Finishing

Edge sealing, bead blasting, and masking for bondable areas. Laser marking available at a minimum character height of 1.5 mm.

06

Fixtures and Tooling

Vacuum fixtures and soft jaws machined in-house, so thin laminates stay flat and supported through the whole cut.

Capability range

Carbon Fiber Machining Specifications

Numbers we can hold on CFRP work. Tighter values are possible on specific features after a drawing review.

ParameterCapabilityNotes
General tolerance±0.005 mmAchievable on machined metal features
Carbon feature tolerance±0.05 mm typicalDepends on layup and cure stability
Maximum part size4,000 mm4,000 × 400 × 150 mm travel
Rotary tableØ400 mmFor angled holes and contoured trim
Surface finishRa 0.8–1.6 μmAs-machined carbon is rougher at cut edges
Laser marking1.5 mm minimumCharacter height, not line width
Inspection100% before shipmentReports on request
Order quantityNo minimumOne prototype to 10,000+ parts
Why GreatLight

What a Carbon Job Needs From the Shop

These are the numbers and habits that decide whether CFRP work goes smoothly.

15Y

Machining since 2011

Fifteen years of prototype and production work across metal, plastic, and composites. Composite jobs sit next to metal jobs, so interfaces get made together.

127

High-precision CNC machines

A mix of 5-axis, 4-axis, 3-axis, and mill-turn centers. The right machine gets picked for the feature, not for whatever is free.

150

Technicians on staff

Programmers, machinists, and inspectors in-house. Carbon work depends on tool choice and setup, so those decisions stay on our floor.

3

Wholly-owned plants

7,600 m² of manufacturing space in Dongguan plus a Singapore factory at No.3 Joo Koon Circle. One point of contact across both.

12h

Quote and DFM turnaround

Quotation and free DFM analysis within 12 hours. Production can start within 24 hours of approval.

4

Quality certifications

ISO 9001:2015, IATF 16949:2016, ISO 13485:2016, and ISO 27001:2022. Uploads are secure and an NDA is available on request.

±0.005 mmAchievable tolerance
7,600 m²Manufacturing space
99.99%Qualification rate
<2%Historical late-delivery rate
Where CFRP is used

Carbon Fiber Parts We Machine by Industry

manufacturing-applications1

Robotics and Automation

Carbon links and arms need mass low and stiffness high. Bores for bearings and harmonic drives have to line up.

  • ±0.005 mm bores
  • 5-axis trim
  • Isolation sleeves
new-energy-industry1

New Energy and EV

Battery enclosures and structural panels in CFRP. Flatness and hole position drive assembly fit.

  • 4,000 mm panels
  • 100% inspection
  • 3–5 day shipping
industrial-machinery1

Industrial Machinery

Carbon gantries and moving frames. Weight reduction only helps if mounting faces stay true after machining.

  • Ra 0.8–1.6 μm
  • Sealed cut edges
  • No minimum order
option-1-concise-good-for-quick-understanding-8

Aerospace and UAV

Ribs, brackets, and control-surface hardware. Ply orientation and hole quality matter more than cycle time.

  • 100% inspection
  • Reports on request
  • NDA on request
FAQs

Carbon Fiber Machining Questions

Can you machine cured carbon fiber laminate, or only mold it?

We machine cured laminate. That covers trimming, drilling, pocketing, and contouring on flat panels and 3D shells.

What we cannot do is create internal geometry. A closed hollow section has to come from a mold first, then we cut the interfaces and mating faces.

What tolerance can you actually hold on CFRP?

Machined metal features on the same assembly can hold ±0.005 mm. Carbon itself is less predictable because cure shrinkage and ply orientation move the part after layup.

On carbon features we typically work around ±0.05 mm, and we machine critical bores after cure rather than before. Send the drawing and we will tell you which features are realistic.

How do you keep cut edges from fraying?

Tool geometry and cut direction do most of the work. Diamond-coated compression cutters, climb milling, and support on both faces of a thin laminate.

After machining, exposed edges can be sealed with a compatible resin where the drawing allows. That stops moisture wicking and limits handling damage.

Is carbon dust a problem for my part or just your shop?

Both. It is abrasive and conductive, so it wears tooling fast and can contaminate nearby assemblies.

We cut wet or with local extraction at the spindle, and we mask bondable surfaces. If your part bolts to metal, we can machine isolating sleeves to avoid galvanic corrosion at the joint.

What is the largest carbon part you can machine?

Up to 4,000 mm on our large-travel machines, with travels of 4,000 × 400 × 150 mm.

For angled holes and contoured trim we use a Ø400 mm rotary table. Long thin panels usually need a vacuum fixture, which we make in-house.

Do you have a minimum order quantity for carbon parts?

No minimum. We run from one prototype up to 10,000+ part runs.

Prototypes usually go on a 3-axis or 5-axis machine with no tooling. Once the design freezes, we quote the production route separately.

How fast can I get a quote and parts?

Quotation and free DFM analysis within 12 hours. Production can start within 24 hours of approval, and parts typically ship in 3–5 days.

That timeline assumes the material is available and the drawing is complete. If a feature needs a fixture, we will say so in the quote.

Can you combine carbon parts with metal hardware in one order?

Yes. Aluminium, stainless, titanium, and engineering plastics are machined in the same plant, so inserts, bushings, and adapter plates ship with the carbon parts.

That keeps interfaces consistent. Tolerances across the assembly can be checked together instead of across two suppliers. Uploads are secure and an NDA is available on request.

Send Us Your Carbon Fiber Part

Upload a drawing or a STEP file. You get a quote, a free DFM review, and a clear answer on which features we can hold.

12-hour quote100% inspectionNo minimum orderNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC