
01
Distortion after quenching
A 4140 shaft held at ±0.01 mm comes back from hardening bowed by 0.08 mm. There is no stock left to straighten it. The part is scrap, and the heat-treat cycle plus freight is already paid for.
We machine 4140, 4340, 4130, 1018 and tool steel into shafts, housings, gears and fixtures. 127 CNC machines, ±0.005 mm tolerance, and a DFM review back to you within 12 hours.
Parts rarely fail because the drawing was hard. They fail because something moved after the cut.
A 4140 shaft held at ±0.01 mm comes back from hardening bowed by 0.08 mm. There is no stock left to straighten it. The part is scrap, and the heat-treat cycle plus freight is already paid for.
4340 at 30 HRC eats carbide edges. On a long bore, a worn insert cuts a taper that only shows up on the CMM. By then the batch is finished and every piece carries the same drift.
A bearing housing with a 3 mm wall rings during boring. The shop slows the feed, the cycle time doubles, and the surface still reads Ra 3.2 μm where the seal needs to sit.
The print calls for 40 HRC and Ra 0.4 μm on the same face. Cut it soft and it tears. Cut it hard and the tool deflects. Someone has to decide the sequence before the first chip.
Two things decide whether an alloy steel part passes: the order of operations, and how the cut behaves on that specific heat lot.

For any 4140 or 4340 part that will be hardened, we rough with 0.5–1.0 mm of stock left on critical faces, send it for stress relief, then finish after the final heat treat. That single change in sequence removes most of the movement people blame on the material.
When the hardness is above 35 HRC we switch to CBN or coated carbide and take lighter depths. Feeds come down, but the geometry stays where the print says it should.
Alloy steel housings and manifolds often have features on four or five faces. Every re-fixture adds error, and on a 20 kg part the setup alone can cost more than the cutting. Our 16 simultaneous 5-axis centers reach those faces in one clamping.
The Ø400 mm rotary table and 4,000 mm travels cover everything from a 30 mm spool valve to a full-length machine bed. For long shafts, the 16 mill-turn centers cut and turn without a second setup.
Pick the grade by the load and the wear surface, not by what is in the rack.
| Grade | Typical use | Machinability |
|---|---|---|
| 1018 | Low-stress brackets, spacers, weldments | Easy, good finish |
| 1045 | Shafts, studs, lightly loaded gears | Moderate, gummy at low speed |
| 4130 | Airframe fittings, thin-wall tubes, weldments | Good, welds cleanly |
| 4140 | Hydraulic rods, mold bases, gears at 28–32 HRC | Good pre-hardened, harder after quench |
| 4340 | High-load shafts, landing gear, connecting rods | Tougher, needs rigid setups |
| A36 | Frames, base plates, non-critical structure | Very easy, poor wear resistance |
| Tool steel | Dies, punches, wear plates, cutting edges | Hard, slow speeds, light depths |
One shop for the cut, the finish and the inspection report.
Sixteen simultaneous 5-axis centers for housings, manifolds and parts with features on five faces. One clamping, one datum.
Twelve four-axis mills for shaft work, cross-drilled parts and anything that needs indexed faces around a centerline.
Twenty-seven three-axis machines and sixteen mill-turn centers cover flat plates, long beds, and turned parts up to Ø400 mm.
Single alloy steel pieces cut from bar or plate. Useful when you need to test a fit before committing to a batch.
Hardening, black oxide, electroless nickel, zinc plating, bead blasting and polishing arranged as one sequence.
Raw material check, in-process monitoring and final inspection. Dimensional reports on request with the shipment.
Numbers to check your part against before you send the file.
| Item | Range | Notes |
|---|---|---|
| Tolerance | ±0.005 mm | On critical bores, journals and bores |
| Surface finish | Ra 0.2–0.8 μm | Fine finish on seal and bearing faces |
| Max part size | 4,000 × 400 × 150 mm | Long beds, rails and base plates |
| Rotary capacity | Ø400 mm table | Indexed and simultaneous work |
| Order quantity | 1 pc to 10,000+ | No minimum order quantity |
| Quote turnaround | 12 hours | With free DFM analysis |
| Production start | Within 24 hours | After drawing release |
| Typical shipping | 3–5 days | For standard alloy steel parts |
Working alloy steel since 2011. The feed and speed tables for 4140 at 30 HRC are already written down, not guessed at.
0.005 mm on critical features, with in-process probing so a drift is caught on the machine, not at final inspection.
Complex housings cut in one setup. Fewer re-fixtures means fewer stacked errors on bolt patterns and bores.
You get a price and a manufacturability note. If a wall is too thin or a corner needs a tool change, we say so before cutting.
Every part, not a sample. Raw material check, in-process monitoring and final inspection with reports on request.
ISO 9001:2015, IATF 16949:2016, ISO 13485:2016 and ISO 27001:2022 cover quality, automotive, medical and data handling.

4130 fittings and brackets where weight and weld quality both matter.

4340 shafts and 4140 housings that run under load and vibration.

Tool steel wear plates, punches and dies held to fit at assembly.
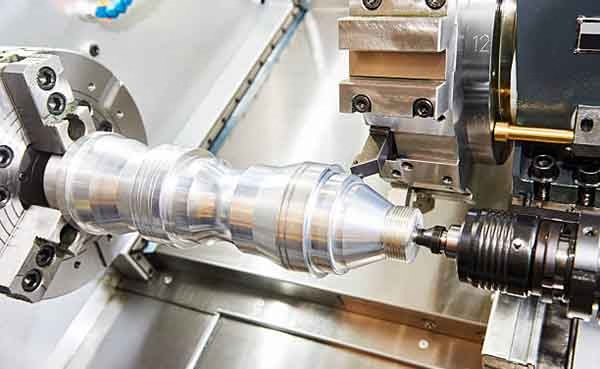
4140 rods and manifolds with deep cross-drilled passages and seals.
If the finished part needs 28–32 HRC and the geometry is simple, pre-hardened stock saves a heat-treat cycle and the distortion that comes with it. We machine it directly and skip the post-quench operation.
When the print calls for 40 HRC or above, start annealed. We rough, you heat treat, we finish. That order keeps the critical dimensions in tolerance.
For 4140 and 4340 going to 40 HRC or higher, we leave 0.5–1.0 mm on critical faces. Thinner stock risks a hard skin that the finish pass cannot clean up.
Long parts move more than short ones. On a shaft over 500 mm we bias the allowance toward the ends, where bowing shows up first.
Yes, on features cut after heat treat. Hard turning with CBN or coated carbide holds that tolerance on bearing journals and seal faces up to about 45 HRC.
Features cut before hardening will not hold it. If the print puts a tight tolerance on a face that gets quenched, we flag it in the DFM review and propose a sequence change.
Ra 0.8–1.6 μm is standard for most turned and milled alloy steel. Sealing faces and bearing journals go to Ra 0.2–0.8 μm with a finishing pass and the right insert geometry.
Harder grades reach a better finish more easily than soft, gummy ones. 1018 at low hardness tends to tear, so we adjust the edge radius and feed instead of chasing the number with speed.
We start by stiffening the setup rather than slowing the cut. Soft jaws, a tailstock or a temporary web across the bore usually removes the ringing.
If the wall is under about 2 mm and the part is long, we may recommend a stress-relief step between roughing and finishing. That is cheaper than fighting the vibration through the finish pass.
Yes. Tool steel, including D2 and similar grades, is cut with lighter depths and slower speeds. It is common for dies, punches and wear plates.
The limit is hardness. Above roughly 45 HRC we recommend grinding or EDM for the final dimensions rather than turning.
There is none. We run from one prototype piece to 10,000-plus part runs. A single alloy steel sample is a normal order for us.
If you are validating a design, send the drawing for one piece first. The DFM notes from that run usually carry over to the production batch.
Uploads are handled as confidential and we work under ISO 27001:2022 for data handling. An NDA is available on request before you send anything.
If your program requires it, tell us at the quote stage and we will have the agreement in place before the files move.
Upload the file and get a price plus a manufacturability note within 12 hours. One piece or ten thousand, the review is the same.
12-hour quote100% inspectionNo minimum order quantityNDA on request
Trusted by engineers and manufacturers worldwide










Upload your 3D model or 2D drawing and get a quotation with a free DFM analysis. Maximum processing size 4,000 mm.
CNC Metals 13 grades
CNC Plastics 10 grades
Machines & processes 12 options
Surface & post-processing 10 options
Material: not selected Machine: not selected Post-process: not selected