GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

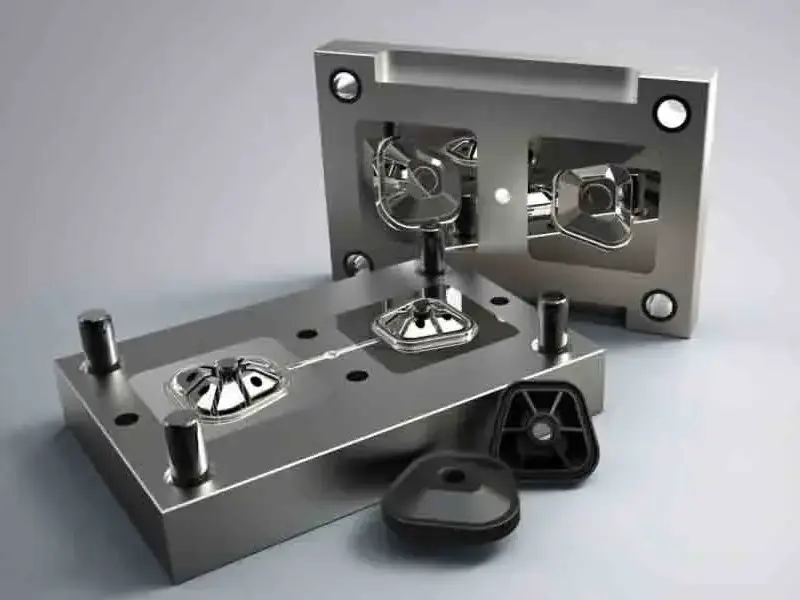
Rapid Tooling

Rapid Tooling Services

We cut aluminum and steel molds for bridge and pilot production. Send a STEP file and get a quote with DFM feedback in 12 hours, then molded samples to check fit and wall thickness.

Aluminum and steel moldsDFM in 12 hoursNo minimum order quantity±0.005 mm mold insertsISO 9001 / IATF 16949NDA on request
rapid-tooling-services-1
15 yearsTooling and machining since 2011
127High-precision CNC machines
12 hoursQuote and DFM analysis
99.99%Qualification rate
Where tooling projects slip

Four problems we see on almost every rush mold

Each one costs days, and usually a second tool modification.

01

“The mold looks fine, but the part does not fit.”

Shrinkage was estimated from a data sheet rather than measured on the actual grade. Warpage appears after the first shots, and the rib or boss that carries the screw no longer lines up. Fixing it means welding steel or cutting a new insert.


02

Weeks lost waiting for a quote

A pilot build is blocked while three suppliers sit on the CAD file. Every day before kickoff is a day added to the launch. Sub-suppliers raise prices in the meantime, and the schedule absorbs the difference.

03

Tool steel chosen for a 300-part run

Hardened H13 works for a million shots. For a bridge order of a few hundred parts, it adds weeks of EDM and polishing. The tool outlives the program, and the cost lands on the prototype budget.

04

Surface finish that fails the first article

A visible Class A surface cannot come off a mold cut with a 6 mm ball nose and no polish step. Sink marks and weld lines show through paint. Rework means pulling the insert out and starting the polish sequence again.

How we build the tool

Mold design, cutting, and first shots under one roof

One team owns the CAD, the toolpath, and the molding trial.

greatlight-cnc-machining-center-11 (1)
DFM before the first cut

We review the part while the steel is still on the shelf

Send the native file or a STEP. Our engineers check draft, wall thickness, gate location, and parting line against the material you plan to run. You get the quote and the DFM notes together in 12 hours.

Most changes are small: a 0.5° draft added to a boss, a rib thinned from 1.2 mm to 0.9 mm, a gate moved off a visible face. Catching them now costs nothing. Catching them after the mold is cut costs an insert.

  • 1
    Gate and runner layoutMatched to part volume and cosmetic requirements, not reused from an old tool.
  • 2
    Draft and wall checkReported per feature, with the material grade and shrinkage assumption listed.
  • 3
    Tolerance reviewCritical dimensions flagged before cutting, so mold dimensions carry the right allowance.

Get Instant Quote

greatlight-cnc-machining-center-11
Cutting the tool

Aluminum for bridge runs, steel where the tool must last

Aluminum molds (6061, 7075, ADC12) cut in days. They handle low-volume runs and let you test a design with real molded parts instead of machined look-alikes. Cycle counts stay modest, and that is usually the right trade for a pilot build.

When the program needs tens of thousands of shots, we move to 4130, 4140, or tool steel with hardened inserts. Both routes run on the same 127 CNC machines, with 16 simultaneous 5-axis centers for deep ribs and contoured cores.

  • 1
    Aluminum toolingFast turnaround, good for bridge production and design validation.
  • 2
    Steel toolingHardened inserts and slides for long production runs.
  • 3
    Insert and core work5-axis and EDM for geometry a 3-axis machine cannot reach.
Choosing a tool material

Aluminum or steel: pick by shot count and part requirement

Numbers below are what we build to, not a general industry rule.

FactorAluminum toolingSteel tooling
Typical shot volumeHundreds to a few thousandTens of thousands and up
Lead time driverCNC cutting onlyCNC plus EDM and heat treat
Mold material6061, 7075, ADC124130, 4140, tool steel
Best fitBridge runs, design validationProduction tooling, abrasive resins
Surface as cutRa 1.6–3.2 μmRa 0.8–1.6 μm before polish
Wear behaviorSofter, edges round overHolds gate and shut-off detail
What we run

Tooling and molding services under one schedule

01

Rapid Mold Making

Aluminum and steel molds cut on 5-axis centers, with inserts, slides, and lifters where the geometry needs them.

02

Rapid Injection Molding

First-shot trials on the tool we cut, so sample parts come from the same cavity that will run your pilot build.

03

CNC Machining

Mold bases, cores, and electrodes, plus machined parts when a molded sample is not the right test.

04

Vacuum Casting

Silicone tools for a handful of parts when a machined mold is more than the batch needs.

05

3D Printing

SLA and similar processes for fit checks and fixtures, before committing to a cut mold.

06

Surface Finishing

Polishing, bead blasting, texture, anodizing, and plating to bring the tool and the part to spec.

Scope and limits

What a rapid tooling order includes

ItemWhat we deliverNotes
Part sizeUp to 4,000 mm processing sizeLarger parts split across inserts
Mold tolerance±0.005 mm on critical mold dimensionsConfirmed against the drawing
Mold materials6061, 7075, ADC12, 4130, 4140, tool steelChosen by shot count
ResinsABS, PC, PMMA, POM, PA, PEEK, PP, HDPECarbon-filled grades on request
InspectionRaw material, in-process, and final checkReports on request
ConfidentialitySecure uploads, NDA availableDesign files stay with the project
Why engineers keep sending us tools

Six numbers that decide the schedule

12 h

Quote and DFM together

Send a STEP file and get pricing plus design feedback in one reply, not two rounds.

24 h

Production can start

Once the design is fixed, cutting starts the next working day.

3–5 d

Parts ship

Molded samples leave the plant in 3–5 days after the trial run is approved.

±0.005 mm

Mold tolerance

Held on critical mold dimensions and verified before the trial.

99.99%

Qualification rate

100% inspection before shipment, with reports on request.

0

Minimum order quantity

One prototype or a 10,000+ part run, on the same process.

15 yearsTooling and machining since 2011
3 plantsWholly-owned, 7,600 m² total
150Technicians on staff
±0.005 mmMold tolerance we hold
Where the tools go

Industries and what each one demands

Experience the GreatLight Advantage in Auto Parts Processing!

Automotive and EV

Housings and brackets that must pass IATF 16949 process control.

  • IATF 16949
  • ±0.005 mm
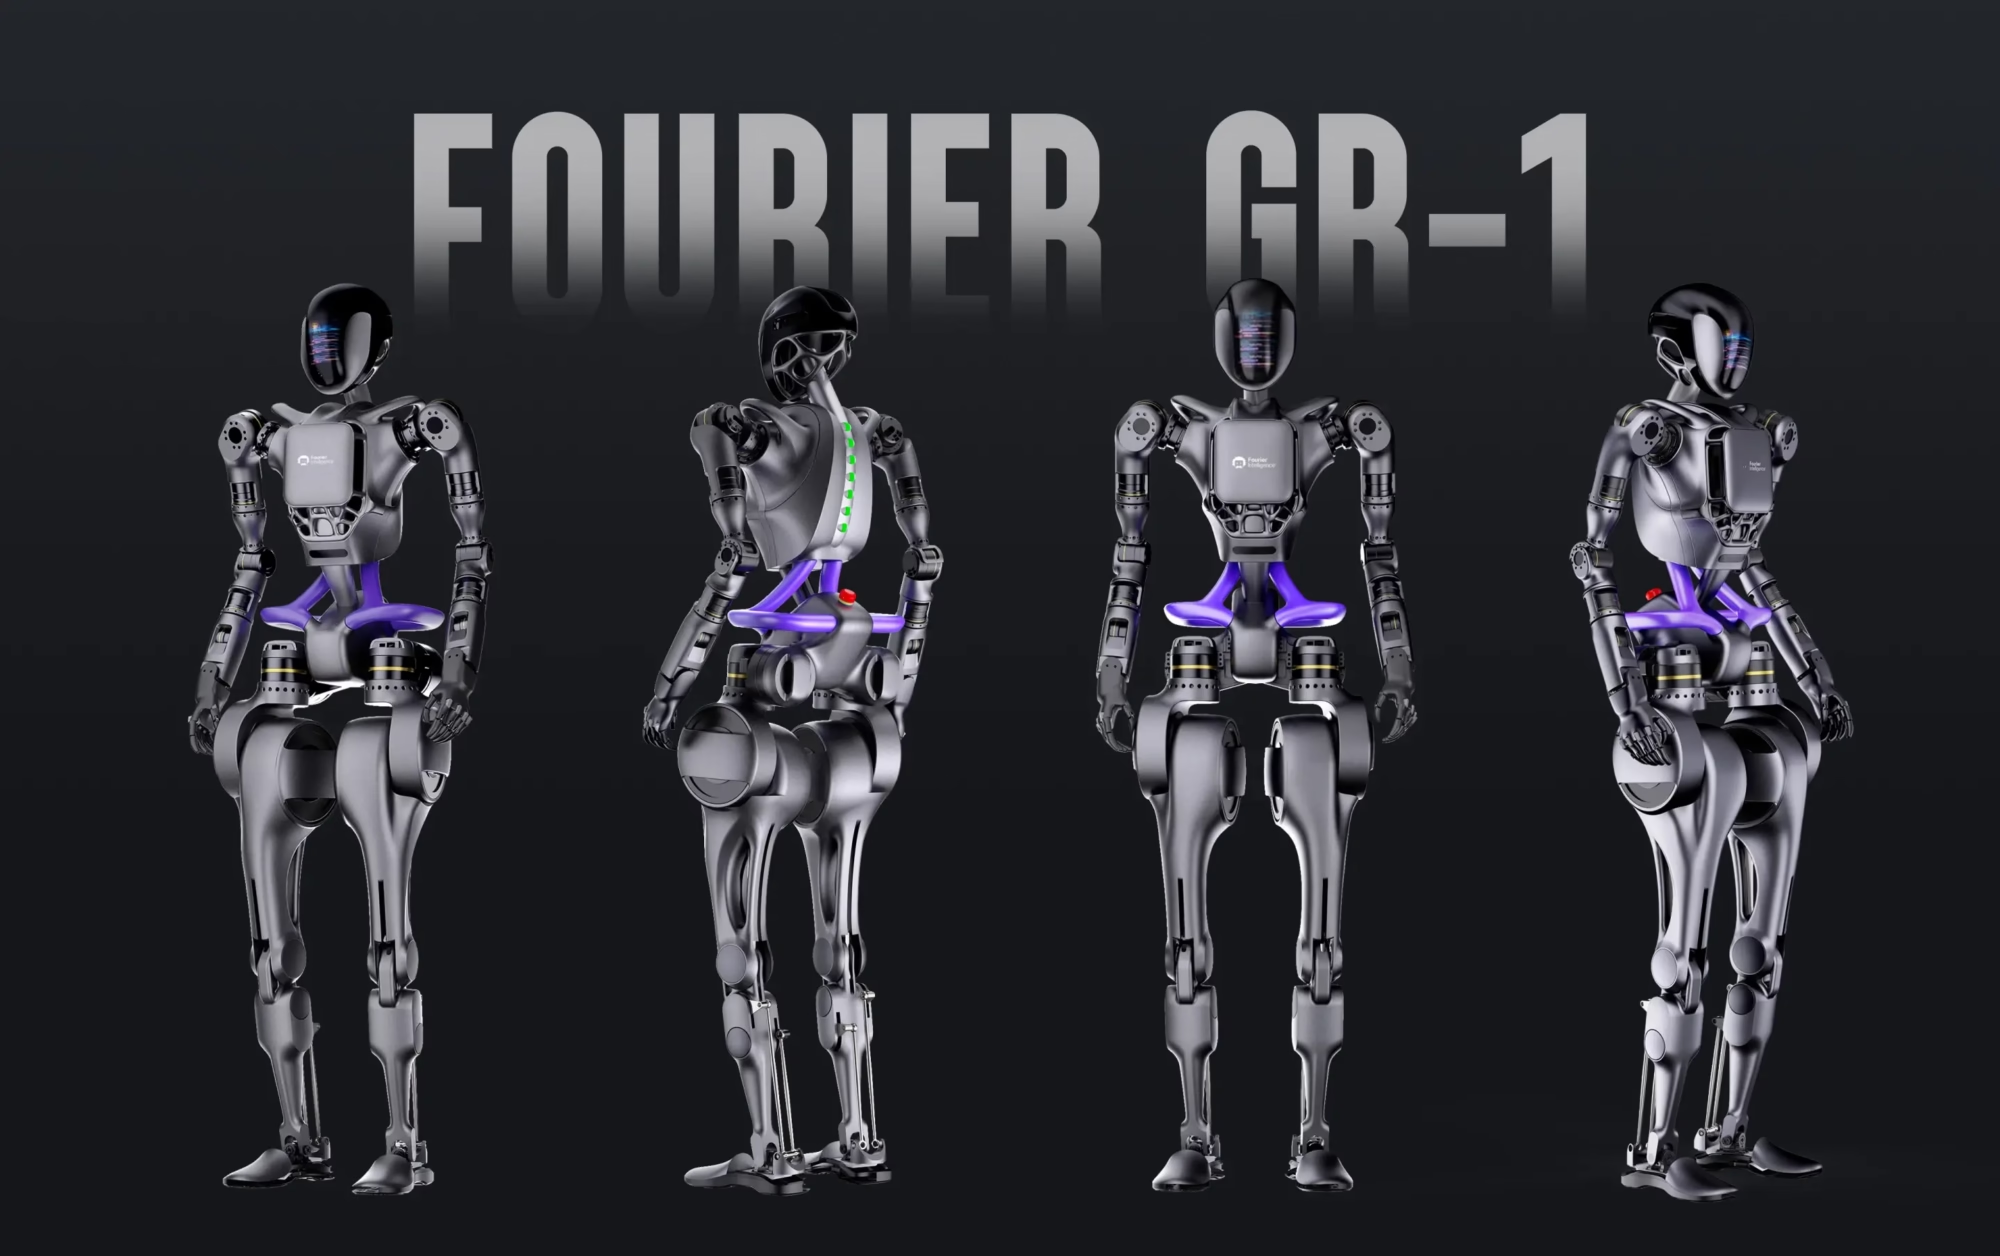
GreatLight Specializing In Humanoid Robot Components

Robotics and automation

Joint covers and gearbox housings where wall thickness drives stiffness.

  • 5-axis cores
  • Ra 0.8–1.6 μm
low volume manufacturing

Low-volume production

Bridge runs that keep a line supplied while the hard tool is being cut.

  • No MOQ
  • 3–5 day ship
GreatLight CNC Machining Compliance Center

Medical and electronics

Enclosures and device housings held to ISO 13485 and ISO 27001 handling.

  • ISO 13485
  • ISO 27001
FAQs

Questions we get before the first cut

What part count makes rapid tooling worth it?

Below roughly 50 parts, machining or vacuum casting is usually cheaper and faster. Between a few hundred and a few thousand parts, an aluminum mold starts to pay off because the cycle time per part drops.

Above that, steel is the better choice. The tool costs more up front, but it holds gate detail and shut-off surfaces through long runs.

Should the mold be aluminum or steel?

Pick aluminum when the part design may still change and you need molded samples quickly. It cuts in days and the tool can be modified or replaced without a large loss.

Pick steel when the resin is abrasive, the cosmetic surface is critical, or the run will exceed tens of thousands of shots. Hardened inserts hold the edge detail that aluminum loses.

How do you handle shrinkage?

We apply a shrinkage allowance per material grade and wall thickness, then check the first shots against the drawing. If dimensions drift, we correct the mold before the pilot run rather than adjusting the part print.

For glass-filled or carbon-filled grades, the allowance differs by flow direction. Tell us the exact grade and we will factor the anisotropy in.

Can you mold a part with undercuts or internal threads?

Yes, but it costs tool complexity. Undercuts need slides or lifters, and internal threads need a rotating core or a hand-loaded insert. Both add machining steps.

If the undercut is small and the resin is flexible, we sometimes strip the part off a straight core instead. We will tell you which route is cheaper for your geometry.

What file formats do you accept?

STEP, STP, IGES, X_T, SAT, SLDPRT, IPT, PRT, CATPART, OBJ, and STL. STEP is the safest for mold work because it carries the solid geometry without translation loss.

Send the native CAD file when you have it. It makes DFM faster and lets us check feature history if a surface is ambiguous.

How do you protect our design?

Uploads are handled as confidential. We can sign an NDA before you send files, and the design stays with the project team.

ISO 27001:2022 certification covers how we handle information internally, not just the mold itself.

What happens if the first shots do not match the drawing?

We measure the samples, compare them to the print, and identify whether the cause is shrinkage, warpage, or a mold dimension. Then we correct the tool and run again.

Corrections found during the trial are part of the tool build. We do not ship samples that fail the critical dimensions.

Can you run the pilot production too?

Yes. The same tool that produced the samples can run the bridge order, so the parts your team approves are the parts you receive.

There is no minimum order quantity. A run can be one part or 10,000+, and we machine a second steel tool in parallel if the volume grows.

Send the part file and get a tooling plan

Quote and DFM feedback in 12 hours, no minimum order quantity, 100% inspection before shipment.

12-hour quoteNo MOQ100% inspectionNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC