
How to Cut Wood With a CNC Machine
A working guide for engineers and buyers who need repeatable wood parts, not a hobby demo. We cover tool choice, feeds and speeds, workholding, test cuts and finishing, plus where routing stops making sense.
In this article
- 1
- 2
- 3
- 4
- 5
- 6
- 7
- 8
Key takeaways
What to prepare before you cut wood with a cnc machine
Routing wood rewards preparation. A machine that holds ±0.005 mm in aluminium will still produce fuzzy edges in oak if the blank moves or the cutter is dull. Before any program runs, decide three things: which wood, which face stays visible, and how the part will be held. Those answers drive tool geometry, feed rate and fixture design.
Wood is not a homogeneous block. Earlywood and latewood cut differently, and grain direction flips from face grain to end grain across a single contour. A cutter that leaves a clean edge along the grain can lift fibres when it crosses the end grain. That is why the same program can pass on one blank and fail on the next.
Moisture content matters more than most shops admit. Kiln-dried hardwood at 6–8% moisture machines cleanly and stays stable after cutting. Material straight off a truck at 12–15% will move after the clamps come off, and the part may twist within days. Let the blank acclimate in the shop before you commit to a tolerance callout.
Decide the tolerance you actually need. Wood moves with humidity, so ±0.1 mm is realistic for a routed hardwood part, while ±0.005 mm belongs to metal work. Telling the shop the real requirement keeps the process honest and the price sane.
Pick the cutter before you pick the speed
The cutter decides chip evacuation and which face survives. A two-flute spiral up-cut pulls chips upward and leaves a clean top surface, which suits through-cut parts where the top face is cosmetic. A down-cut pushes chips down, protecting the top face but packing dust into the kerf on deep passes.
Compression spirals combine both: up-cut geometry at the tip, down-cut at the shank. They are the standard choice for plywood and melamine, where both faces must stay clean. They cost more and need a deeper first pass to engage both zones, so they are a poor fit for 3 mm sheet.
Flush trim and template bits follow an existing profile. Use them when a part is nested against a jig or when you are trimming veneer after glue-up. Their bearing or shank rubs the template, so the template has to be harder than the workpiece, typically MDF sealed with lacquer or a phenolic sheet.
Solid carbide lasts far longer than high-speed steel in abrasive species such as teak or MDF. Coated cutters help in MDF and particle board, where resin builds heat. For most hardwoods and softwoods, an uncoated two-flute carbide spiral between Ø3 mm and Ø12 mm covers the majority of work.
Feeds, speeds and depth of cut for wood
Start from chip load, not from a feed number copied off the internet. Chip load is the thickness of material each cutting edge removes per revolution. For a Ø6 mm two-flute carbide cutter in hardwood, a chip load of 0.1–0.2 mm per tooth keeps heat down and produces a clean edge.
Feed rate follows from chip load: feed = chip load × flutes × RPM. At 18,000 rpm with two flutes and 0.15 mm chip load, the feed lands near 5,400 mm/min. If the machine or the fixture cannot hold that speed, reduce RPM instead of dropping the chip load too far, or the cutter will rub and burn.
Depth of cut should be conservative on the first pass. A common starting point is one times the cutter diameter for softwood and half the diameter for dense hardwood, with a finishing pass of 0.3–0.5 mm left on the walls. Full-depth single passes work in foam and soft pine but chatter in maple.
Ramp or helix into the cut rather than plunging straight down. A vertical plunge in hardwood loads the centre of the cutter where surface speed is lowest, and the tool will heat and dull. A 2–3° ramp angle spreads the load and keeps the chip load stable through entry.
Workholding and dust control decide the result
A wood part that moves during the cut is scrap, no matter how good the program is. Vacuum tables hold full sheets well but lose grip as soon as you cut the perimeter and break the vacuum seal. Plan tabs or leave an onion skin of 0.3–0.5 mm so the part stays attached until the last operation.
For smaller blanks, screw the workpiece to a sacrificial MDF spoilboard from underneath, outside the finished profile. Double-sided tape works for thin panels when the tape covers most of the underside, but it releases with heat, so keep spindle speed and feed in a range that does not scorch the surface.
Clamps reach only the edges of the blank. On a 600 × 600 mm part, the middle can lift under cutter pressure even when the corners are tight. Add a mid-span hold-down or reduce depth of cut in the centre region. Listen for a change in pitch: it usually means the part has started to move.
Dust extraction is a safety and quality item, not an accessory. Airborne fine dust from MDF and hardwood is a health hazard, and chips left in the kerf are re-cut, which dulls the tool and burns the edge. A 100 mm hose at the shoe plus a downdraft table covers most routing setups.
When wood routing is the wrong process
Routing stops making sense when the drawing demands metal-level tolerance on a wood part. A ±0.05 mm callout on a 400 mm oak rail will fail on humidity alone, even if the machine holds the number on the day of cutting. If the function needs that tolerance, switch the material or redesign the joint.
Deep narrow pockets are another limit. A pocket 40 mm deep and 6 mm wide needs a long, thin cutter, and wood has little stiffness to resist deflection. The tool will bend, the wall will taper, and the finish will burn. Either open up the pocket or split the part.
Very small batches of flat panels are often faster on a panel saw or a waterjet-cut template. Routing wins when the part has contours, pockets, 3D relief or repeated features where one program replaces many manual setups.
Finally, some species machine badly. Highly abrasive tropical hardwoods dull carbide quickly, and resinous softwoods gum up cutters. In those cases, plan shorter tool life into the quote rather than assuming the same cutter will run all day.
Step by step: cutting wood on a CNC machine
- 11. Inspect and flatten the blankCheck moisture at 6–8% with a pin meter. Face the top on the machine with a Ø25–50 mm surfacing bit, 0.5 mm depth, 40–60% stepover, until the surface is flat and clean.
- 22. Set the zero point on the stock, not the tableTouch off Z on the highest point of the blank, not the spoilboard. Wood thickness varies by 0.2–0.5 mm across a sheet, and a Z zero taken from the table will cut through thin areas.
- 33. Load the program and simulateRun the CAM simulation and check for holder collisions, rapid moves through the part, and any pass deeper than one cutter diameter. Fix the program before the spindle starts.
- 44. Cut a test piece in the same woodRun the exact toolpath on a scrap offcut from the same board. Inspect edge quality, measure the wall, and adjust feed by 10–15% before touching the production blank.
- 55. Rough with a larger cutter, finish with a smaller oneRough at 1× diameter depth with a Ø6–12 mm cutter, leave 0.3–0.5 mm on walls and floor, then finish with a Ø3–6 mm cutter at 0.3 mm stepover for a smoother surface.
- 66. Monitor the first 30 seconds of every passListen for chatter and watch the chip color. Light, dry chips mean the feed is right. Brown chips or smoke mean the cutter is rubbing; raise feed or lower RPM immediately.
- 77. Cut tabs last and break them by handLeave 0.3–0.5 mm onion skin or 4–6 tabs of 3 mm width. Cut them with a flush trim bit or a hand saw, then sand flush. Never snap a tab that is thicker than 1 mm.
- 88. Deburr, sand and sealSand cut edges at 180 then 240 grit, break sharp corners, and apply sealer within 24 hours to slow moisture exchange and reduce movement.
Cutter and parameter guide for common wood work
Starting points only. Confirm with a test cut on the same board.
| Cutter | Best for | Chip load | Depth of cut |
|---|---|---|---|
| Ø6 mm 2-flute up-cut | Through cuts, top face visible | 0.1–0.2 mm/tooth | 1× diameter (softwood) |
| Ø6 mm 2-flute down-cut | Pockets, top face cosmetic | 0.1–0.15 mm/tooth | 0.5× diameter (hardwood) |
| Ø6 mm compression | Plywood, melamine, both faces | 0.1–0.2 mm/tooth | Deeper than 1× diameter |
| Ø3 mm 2-flute up-cut | Small radii, fine detail | 0.05–0.1 mm/tooth | 0.5–1.0 mm finishing |
| Ø12 mm 3-flute up-cut | Fast roughing, softwood | 0.2–0.3 mm/tooth | 1–1.5× diameter |
| Flush trim with bearing | Trimming to a template | By hand feed | Full profile, 1 pass |
Questions engineers ask about wood on a CNC
Can a metal CNC machine cut wood?
Yes, with the right spindle speed and dust control. A machining centre that reaches 15,000–24,000 rpm handles wood well. The limits are usually vacuum workholding and chip extraction rather than the machine frame.
Below roughly 8,000 rpm, surface speed at the cutter is too low for clean wood edges. If your spindle tops out there, expect more sanding after the cut.
What spindle speed should I use in hardwood?
Most Ø3–12 mm carbide cutters in hardwood run between 16,000 and 20,000 rpm. Set the feed from chip load rather than lowering RPM to match a feed you already have.
If you hear a high-pitched scream, the cutter is rubbing. Raise the feed 10–15% and listen again.
How do I stop tear-out on plywood?
Use a compression spiral, or cut with a down-cut tool and accept slower chip evacuation. Score the top veneer with a shallow 0.3 mm pass before the full-depth cut.
Sharp tooling matters more than any parameter change. A dull compression bit tears plywood regardless of feeds and speeds.
Do I need a vacuum table for wood?
Not always. Screwing to a spoilboard or using tape works for one-off parts and dense hardwoods. Vacuum pays off on nested sheet work and thin panels where screws would mark the surface.
If you use vacuum, plan onion skin or tabs. Cutting the full perimeter releases the seal and the part will shift.
How much material should I leave for finishing?
Leave 0.3–0.5 mm on walls and floor for the finishing pass. That is enough to remove the marks from roughing without loading the cutter.
On end grain, take two light finishing passes instead of one. End grain lifts fibres easily and a second pass at the same depth cleans them up.
Can GreatLight machine wood parts alongside metal parts?
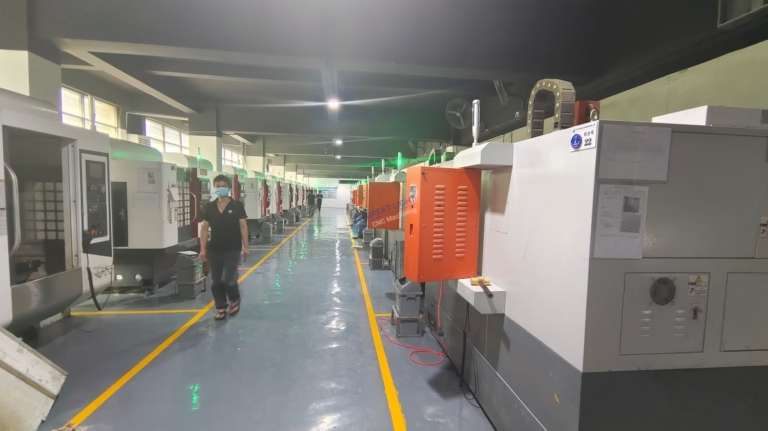
We run 127 high-precision CNC machines across three plants in Dongguan and Singapore, with 16 simultaneous 5-axis centres and a 4,000 mm maximum processing size. Metal work holds ±0.005 mm; wood work is quoted to the tolerance the material can actually hold.
No minimum order quantity, from one prototype upward. Upload a drawing and we return a quotation with a free DFM analysis within 12 hours.
Send your wood part drawing for a DFM check
Upload a STEP or DXF file and we will tell you which features route cleanly in wood and which ones should change. Quotation and free DFM analysis within 12 hours.
12-hour quoteNo minimum order quantityNDA on request
More machining notes
We publish setup notes, tooling trials and inspection data from the factory floor.











