
Rapid Tooling Inc Quality Parts: What Actually Separates Them
When a drawing calls for rapid tooling inc quality parts, the requirement is not speed alone. It is tooling-grade precision delivered on a short schedule. This page explains where the quality comes from, which part features suit the process, and when rapid tooling is the wrong call.
In this article
- 1
- 2
- 3
- 4
- 5
- 6
- 7
- 8
What rapid tooling inc quality parts really means on the shop floor
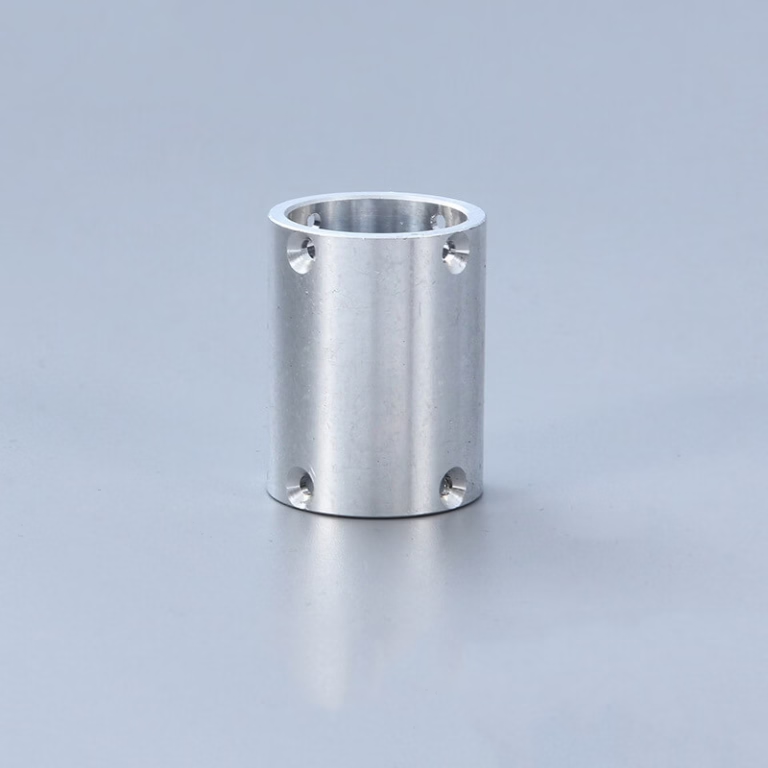
The phrase pulls together two demands that normally fight each other. Tooling implies hard, accurate, long-life geometry. Rapid implies a short calendar. On the floor, that means inserts, bridge tools, jigs and low-volume production parts cut from solid stock or cast blanks, then finished and inspected in days rather than months.
Quality here is not a marketing word. It is a set of measurable outcomes: dimensional conformity to the drawing, repeatability between the first and last part, surface integrity that survives handling, and paperwork that matches the physical parts. If any one of those is missing, the tool is not a quality part no matter how fast it shipped.
So the starting question is not which supplier is cheapest or fastest. It is which part features drive the cost and risk. A deep rib, a thin wall, a tight true position callout, a cosmetic face — each one changes the process plan. Engineers who understand that usually get better quotes and fewer surprises.
Keep one boundary in mind. Rapid tooling is a bridge, not a high-volume die. If the program will run hundreds of thousands of parts, a hardened production tool is still the right answer. Rapid tooling covers the gap between prototype and that tool.
- 1Tooling-grade geometryInserts, bridge tools and functional parts with real tolerances.
- 2Short calendarMachined and finished in days, not tooling lead times.
- 3Measurable qualityDrawing conformity, repeatability, surface integrity, paperwork.
Where machining precision comes from: setup count and machine choice
Every setup adds a new datum, and every new datum adds error. A part machined in five setups accumulates five chances for a fixture to sit slightly wrong. Machining it in two setups removes most of that stack. This is the single biggest lever on geometric tolerance, and it is decided at the quoting stage.
Simultaneous 5-axis machining is how that lever gets pulled. With a Ø400 mm rotary table and a trunnion, the tool can reach five faces of a part without the operator reopening the vise. Features that are dimensioned to each other — a bore pattern, a face and a perpendicular slot — stay in one coordinate frame for the whole cycle.
Machine size matters too. A 4,000 × 400 × 150 mm travel envelope handles long base plates and rails. Medium frames around 750 × 1,150 × 550 mm and 600 × 600 × 600 mm cover most housing and bracket work. Compact 500 × 500 × 450 mm and 500 × 310 × 200 mm machines suit small, high-count parts where spindle speed and tool change time dominate.
The machine alone does not hold ±0.005 mm. Constant chip load, controlled tool deflection and attention to thermal growth do. On a thin-wall aluminium insert, the programmer may rough, let the part cool, then take light finishing passes. That pause costs cycle time and saves the part.
- 1Fewer setupsCumulative fixture error drops with each orientation removed.
- 2Right envelopeLong rails on 4,000 mm travel, small parts on compact frames.
- 3Thermal controlRough, cool, then finish thin-wall sections.
Tolerance, surface finish and the features that are hard to hold
A blanket tolerance on a drawing is a trap. The shop will quote the tightest callout it sees, and you pay for it everywhere. Better practice: keep critical fits at ±0.005 mm and let non-functional edges sit at general tolerance. Cost follows the tightest dimension, not the average one.
Surface finish behaves the same way. As-machined at Ra 1.6–3.2 μm is fine for brackets and internal plates. Sealing faces and bearing bores usually want Ra 0.8–1.6 μm. Optical and fluid-contact surfaces may need Ra 0.2–0.8 μm, which means slower passes, finer tools and often a finishing operation after heat treatment.
Some features resist even good processes. Deep pockets with a small corner radius need long, slender tools that deflect. Sharp internal corners cannot be milled at all — they need EDM or a design change to a corner radius. Thin floors under 1 mm will chatter unless they are supported or left thick and skimmed.
Text and engraving have their own limit. Laser marking holds a minimum character height of 1.5 mm. Below that, characters fill in and become unreadable. If a part number must be legible after anodizing, size it up and place it on a flat, non-cosmetic face.
- 1Tolerance zoningTight only where it functions; general elsewhere.
- 2Finish by functionRa 1.6–3.2 μm general, 0.8–1.6 μm sealing, 0.2–0.8 μm optical.
- 3Design limitsSharp internal corners need EDM or a radius change.
Finishing, inspection and certification as one system
A dimensionally perfect part can still fail at the customer. The usual cause is handling and finishing. If anodizing, plating or powder coating is sent to an outside shop with no agreed process sheet, colour and thickness vary between lots, and masked areas get coated anyway. Keeping finishing under one quality system removes that variable.
Inspection has to be planned, not improvised. A workable sequence is raw material verification, in-process checks at each setup, and a final inspection before shipment. For a tooling insert, that final step may include a CMM report on the critical callouts. Reports are available on request; the point is that the measurement happens on every part, not just the first one.
Certification tells you whether the system behind the parts is audited. ISO 9001:2015 covers general quality management. IATF 16949:2016 applies to automotive work. ISO 13485:2016 covers medical devices. ISO 27001:2022 covers information security, which matters when your CAD files leave your network.
None of these certificates makes a bad part good. What they do is shorten the conversation. If a supplier holds the certificate your industry requires and can show inspection records, you spend less time auditing and more time building.
- 1In-house finishingAnodizing, plating, powder coating, laser marking under one roof.
- 2Planned inspectionMaterial check, in-process checks, final check before shipment.
- 3Certificates as filtersISO 9001, IATF 16949, ISO 13485, ISO 27001.
Material choice and how it changes the process plan
Aluminium is the default for rapid tooling parts. Grades like 6061-T6, 7075 and 6082 machine fast, hold tight tolerances and take anodizing well. 7075 gives higher strength for jigs and fixtures, though it is less corrosion resistant and needs a coating in humid service.
Steels change the picture. 1018 and 1045 are straightforward. 4140 and 4340 need more conservative cutting data and may be pre-hardened, which slows the cycle. Tool steel for an insert is often machined soft, then hardened and ground. If the drawing needs ±0.005 mm after hardening, plan for a finishing pass after heat treatment, not before.
Stainless grades such as 303, 304, 316L and 17-4PH work harden, so the tool must keep moving. A dwell in the cut raises local hardness and kills the next pass. Titanium TC4 and Inconel push this further: low cutting speeds, rigid setups and plenty of coolant. These are not impossible on a 5-axis center, but cycle times are longer and the quote should reflect that.
Plastics behave differently again. POM and PEEK hold dimensions well. ABS and PP move with temperature and need light finishing passes. Carbon fibre is abrasive, so tool life drops and the dust needs extraction. Material choice is a process decision, not just a strength decision.
- 1Aluminium first6061-T6, 7075, 6082 for most tooling and fixture work.
- 2Steel and hardeningPlan a post-hardening finishing pass for tight final tolerances.
- 3Work-hardening gradesKeep the tool moving in 304, 316L, 17-4PH, TC4.
Common pitfalls when buying rapid tooling inc quality parts
The first pitfall is quoting from a PDF. A 2D drawing hides the datum structure and the sequence of operations. Send the native CAD file so the shop can check wall thickness, tool reach and fixture access before pricing. A free DFM review within 12 hours catches most of these before metal is cut.
The second is treating inspection as optional. If the purchase order does not name the callouts that need a report, the shop may check only what is easy. Say which dimensions are critical, and ask for the measurement method. A number without a method is not evidence.
The third is forgetting handling and packaging. A finished, anodized face can be scratched in transit by a carelessly placed clamp. For cosmetic parts, agree on protection before shipment. This is a small cost that prevents a large argument.
The fourth is choosing on price alone. The cheapest quote often assumes loose tolerances, outsourced finishing and no inspection report. Compare total cost: rework, sorting, late delivery and the engineering time spent chasing. A part that arrives right the first time is the cheaper part.
- 1Send CAD, not just PDFNative files allow real DFM before quoting.
- 2Name the critical calloutsSay which dimensions need a report and how to measure them.
- 3Protect cosmetic facesAgree packaging for finished, visible surfaces.
Six checks before you place a rapid tooling order
Each check can be answered in one short exchange.
- 1Ask for the setup planHow many orientations will the part be machined in? Two or fewer is a good sign for tight geometry.
- 2Confirm the tolerance you actually needSend the drawing and ask which callouts drive the price. Expect a split between critical and general tolerance.
- 3Ask what is inspected and howRequest the inspection sequence and whether a report is available on request.
- 4Check where finishing happensAnodizing, plating and coating should sit under the same quality system, or be tightly controlled.
- 5Match certificates to your industryISO 9001 for general work, IATF 16949 for automotive, ISO 13485 for medical, ISO 27001 for file security.
- 6Ask about the schedule riskRequest a quotation and DFM analysis within 12 hours and confirm when production can start.
Which process fits which rapid tooling part
Use this to narrow the process before you request a quote.
| Part situation | Preferred process | Why |
|---|---|---|
| Insert or bridge tool, tight true position | 5-axis machining | One setup holds related features together |
| Long rail or base plate | 3-axis on 4,000 mm travel | Envelope handles length without repositioning |
| Turned shaft with cross holes | Mill-turn center | Turning and milling in one cycle |
| Thin-wall housing, cosmetic face | 5-axis plus hand finishing | Control deflection, then blend surfaces |
| Sharp internal corner, hardened steel | EDM after machining | Milling cannot produce a zero-radius corner |
| Simple bracket, loose tolerance | 3-axis machining | No need to pay for extra axes |
| Concept form check, no tolerance | 3D printing or vacuum casting | Fastest route when fit is not critical |
The verdict
If your part has tight true position and a short deadline, choose a shop that machines it in one or two 5-axis setups and controls finishing in-house. If the program will run hundreds of thousands of pieces, stop and buy a hardened production tool instead.
Questions engineers ask before ordering
How tight a tolerance can rapid tooling parts actually hold?
On a stable part with the right process plan, ±0.005 mm is achievable on critical features. The limit is usually the part, not the machine. Thin walls, long slender tools and unsupported floors move under cutting force, so those features may need a looser callout or a design change.
Ask for tolerance zoning. Keep the functional fits tight and let everything else sit at general tolerance. That keeps both the price and the risk under control.
Is rapid tooling suitable for production volumes?
It suits bridge production and low-volume runs, from a single prototype up to runs of a few thousand parts. Beyond that, tool wear and cycle time make a hardened production tool cheaper per part.
The decision point is the tooling cost divided by the number of parts. When the program is uncertain, rapid tooling lets you start shipping while the hard tool is being built.
What file formats do you need for a quote?
Native CAD is best, plus a PDF drawing with the critical callouts marked. STEP files work when native files are not available. Include material, finish, quantity and any inspection requirements in the request.
Uploads are handled as confidential, and an NDA is available on request. A quotation and DFM analysis come back within 12 hours.
Which materials are common for tooling inserts?
Aluminium grades such as 6061-T6, 7075 and 6082 cover most inserts and fixtures. Pre-hardened 4140 and 4340 are used where more wear resistance is needed. Tool steel is machined soft, then hardened and finished.
For work-hardening grades like 304, 316L, 17-4PH and TC4, expect longer cycle times. The cutting data has to keep the tool moving through the material.
How does finishing affect lead time?
Machining is usually the fast part. Anodizing, plating or powder coating adds calendar time, and outsourced finishing adds the most because the parts leave the building. Keeping finishing in-house shortens the loop and reduces handling damage.
If a cosmetic face matters, agree on how the part is protected after finishing. Scratches in transit are the most common reason a good part gets rejected.
What happens if the first articles are out of tolerance?
The right response is to measure, compare against the setup plan and correct the process, not to hand-blend the part. If a critical dimension is out, the shop should tell you before shipment, not after.
That is why inspection is planned at each setup. Catching a drift at setup three is far cheaper than catching it after finishing.
Send the CAD file and get a real process plan
Upload your model and drawing. We return a quotation and free DFM analysis within 12 hours, then start production within 24 hours when the design is ready.
12-hour quote100% inspectionNo MOQNDA on request
More machining notes
We publish setup notes, tooling trials and inspection data from the factory floor.











