
Cast Zinc Material Properties Guide
This guide covers the actual cast zinc material properties engineers need before releasing a drawing: density, tensile and impact behavior, creep, and how Zamak 3, Zamak 5, Zamak 7, ZA-8 and ZA-27 differ. It is written for design and sourcing engineers who must decide whether a zinc alloy fits a part, and it shows where zinc should not be used.
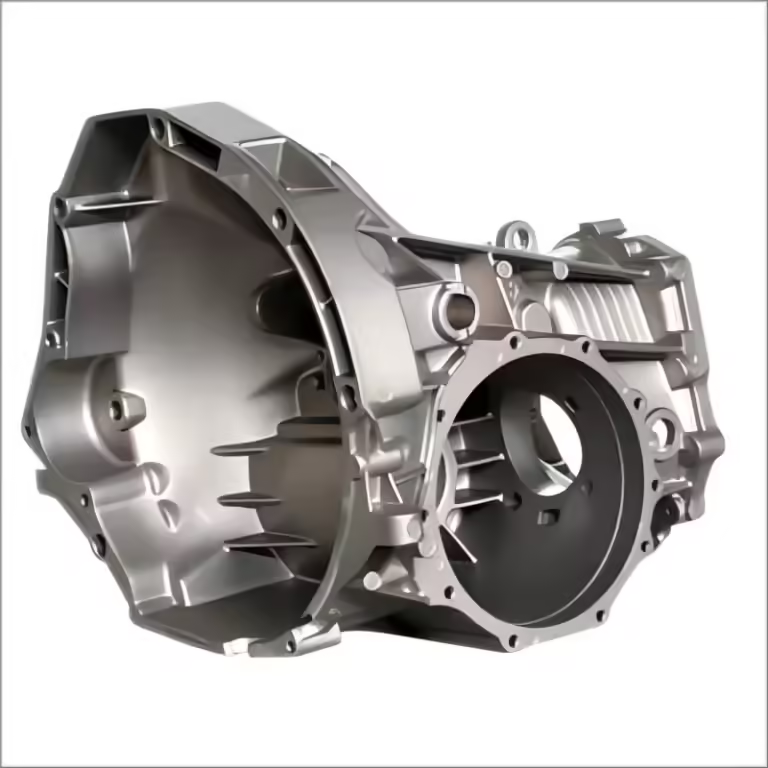
What Zinc Casting Alloys Actually Are
Die casting grades are not pure zinc. The alloying elements decide strength, creep resistance, and machinability.
Base Metal and Alloying Elements
Die casting grades are almost never pure zinc. Commercial alloys sit between roughly 3.5% and 27% aluminum by weight, with copper, magnesium, and small amounts of iron and lead controlled tightly. Aluminum raises strength and hardness. Copper improves creep resistance and wear behavior but slows the casting cycle. Magnesium controls grain growth and limits intergranular corrosion. Iron keeps the melt from attacking the die steel, and lead, tin, and cadmium are held very low because they cause intergranular corrosion and dimensional growth over time.
That balance matters more than the base metal. A 4% aluminum alloy with 3% copper behaves very differently from a 4% aluminum alloy with almost no copper. The first resists creep under a sustained load. The second is cheaper, casts faster, and machines more easily, but it will slowly deform in a warm, loaded application.
Typical as-cast density lands near 6.6 g/cm³ for the Zamak family and closer to 5.0 g/cm³ for the high-aluminum ZA-27. Compare that with 2.7 g/cm³ for aluminum and 7.8 g/cm³ for steel. The mass penalty versus aluminum is real, and it is often the first reason a project moves away from zinc.
- 1AluminumRaises strength and hardness, lowers ductility as content climbs.
- 2CopperImproves creep resistance and wear; slows cycle time.
- 3MagnesiumRefines grain structure, limits intergranular corrosion.
- 4Lead, tin, cadmiumHeld very low. They cause corrosion and dimensional growth.
Cast Zinc Material Properties That Drive Design
The useful properties cluster in a way that suits small, thin-walled, detailed parts. Zinc melts around 380–390 °C, far below aluminum at roughly 660 °C. That lower melting point means less thermal shock to the die, longer die life, and thinner walls. Walls down to 0.5 mm are common in Zamak 3, and 0.25 mm is achievable in short sections. Aluminum die casting usually cannot go below about 1 mm without trouble.
As-cast tensile strength for Zamak 3 is about 283 MPa, and Zamak 5 reaches roughly 328 MPa. ZA-27 pushes past 400 MPa. Elongation for Zamak 3 is around 10%, which gives it enough ductility to survive crimping and staking without cracking. Impact resistance is modest compared with brass or steel, so parts that take direct hits need a thicker section or a different material.
Thermal conductivity sits near 113 W/m·K for Zamak 3, about ten times that of stainless steel. That is why zinc housings often double as heat spreaders for small electronics. Electrical conductivity is roughly 27% IACS, enough for shielding and grounding but not for current-carrying conductors.
Machining behavior is a genuine strength. Zinc chips break cleanly, cutting speeds are high, and the as-cast surface can be finished to Ra 0.8–1.6 μm without a lot of effort. On our 5-axis centers we hold ±0.005 mm on zinc parts when the fixture supports the thin sections. The metal is soft, so clamping pressure has to be watched or the part will deform before the cutter touches it.
- 1Melting point380–390 °C, roughly 270 °C below aluminum.
- 2Minimum wall0.5 mm typical, 0.25 mm in short sections.
- 3As-cast tensile283 MPa for Zamak 3, 328 MPa for Zamak 5.
- 4Thermal conductivityAbout 113 W/m·K for Zamak 3.
Zamak and ZA Alloy Comparison
Typical as-cast values. Confirm against the supplier datasheet for a given heat.
| Alloy | Al / Cu content | Tensile strength | Creep resistance |
|---|---|---|---|
| Zamak 3 | 4% Al, low Cu | About 283 MPa | Moderate |
| Zamak 5 | 4% Al, 1% Cu | About 328 MPa | Good |
| Zamak 7 | 4% Al, low Cu, Mg | About 283 MPa | Moderate, better ductility |
| ZA-8 | 8% Al, 1% Cu | About 374 MPa | Good |
| ZA-27 | 27% Al, 2% Cu | About 425 MPa | Best in the family |
Choosing Between Zamak and ZA Alloys
Zamak 3 is the default for a reason. It casts easily, plates well, and has the best combination of ductility and surface finish in the family. If a part is a decorative housing, a connector shell, a zipper pull, or a bracket that sees no sustained load, Zamak 3 will usually be the cheapest correct answer.
Zamak 5 trades a little ductility for strength and creep resistance. The 1% copper addition makes it the standard choice for automotive hardware, lock components, and parts that carry a load for years. Zamak 7 is the low-magnesium version, used when the part must be plated or when thin walls need extra fluidity in the die.
The ZA alloys enter when loads rise. ZA-8 is a drop-in upgrade for Zamak 5 in many bearing and bushing applications because its higher aluminum content gives it better wear resistance at elevated temperature. ZA-27 has the highest strength and the best creep behavior, but it also has the lowest density in the group, the highest melting point, and a sharper casting window. It is harder on tooling and needs more careful gate design.
A practical rule: start with Zamak 3. Move to Zamak 5 or ZA-8 only when the load case demands it. Pick ZA-27 when you need strength and creep resistance together and you can accept the tooling cost. If the part is large, thin, and heavily loaded all at once, zinc is probably the wrong family and you should be looking at aluminum or steel.
- 1Zamak 3Default for housings, brackets, plated parts.
- 2Zamak 5Automotive hardware, lock parts, sustained loads.
- 3ZA-8Bearings and bushings running warm.
- 4ZA-27Highest strength and creep resistance, tighter process.
Creep: The Failure Mode Engineers Miss
Creep is slow deformation under a constant load at a temperature well below the melting point. In zinc it becomes measurable above about 60 °C and accelerates sharply past 100 °C. A bolt boss that holds a 200 N load at 80 °C may look fine on day one and be visibly shorter after two years. Nothing cracks. The part just moves.
The mechanism is grain boundary sliding. At higher temperatures, zinc grains slide past each other and the alloy deforms without any increase in stress. Copper additions pin those boundaries, which is why Zamak 5 and ZA-27 outperform Zamak 3 under sustained load. Aluminum content helps too, but copper is the stronger lever.
Design against creep with geometry, not just alloy choice. Increase section thickness at the load path. Add ribs so the stress spreads over a larger area. Avoid long unsupported spans that carry a steady load. If the joint is bolted, use a washer or a steel insert to spread the clamp force. Where the service temperature stays above 100 °C, treat zinc as a candidate only after a creep check, and consider aluminum instead.
Fasteners are a common trap. A threaded zinc boss that is torqued once and left alone will relax over time. A through-bolt with a steel nut and washer on the far side removes the creep path entirely. When the design allows it, that is the cheaper fix.
- 1Below 60 °CCreep is negligible for most Zamak parts.
- 260–100 °CMeasure it. Copper content matters most here.
- 3Above 100 °CAvoid sustained loads or switch material.
- 4Bolted jointsUse washers or steel inserts to spread clamp load.
Where Zinc Fits and Where It Does Not
Electronics use zinc for shielding cans, connector housings, and heat-spreading enclosures. The high thermal conductivity and the ability to cast thin walls make it a good match for small devices that need both structure and heat paths. EMI shielding benefits from the 27% IACS conductivity, and the as-cast surface takes plating and powder coating without much prep.
Automotive and EV applications lean on Zamak 5 and ZA-8 for lock bodies, seat hardware, sensor housings, and brackets that see vibration but modest temperature. Zinc handles vibration well because of its damping capacity. The limits show up near exhaust components, motor windings, and underhood areas that soak above 100 °C.
Consumer products use zinc where feel and finish matter: knobs, buckles, housings, and decorative hardware. The weight is part of the appeal. A zinc knob feels solid in a way that a plastic one does not, and it can be polished, brushed, or plated to a wide range of finishes.
Zinc is the wrong choice for large structural parts, high-temperature service, and anything that must be welded. It is also a poor fit for parts that need very high impact toughness, such as safety-critical brackets. For those, aluminum or steel is the better path, and we will say so during the DFM review.
- 1Good fitThin housings, connectors, knobs, lock hardware.
- 2WorkableBrackets and bushings below 100 °C.
- 3Poor fitHigh-temperature, welded, or high-impact parts.
Common Questions
Is cast zinc strong enough for structural brackets?
For small brackets under moderate load, yes. Zamak 5 at about 328 MPa tensile handles sensor mounts, lock plates, and similar parts well.
For safety-critical or highly loaded brackets, zinc is usually not the right call. Impact toughness is modest, and creep becomes a factor above 60 °C. Aluminum or steel is the safer choice there.
How does zinc compare with aluminum for die casting?
Zinc melts about 270 °C lower, so dies last longer and walls can be thinner. Surface finish is better as-cast, and machining is faster.
Aluminum wins on weight and high-temperature strength. At 2.7 g/cm³ versus 6.6 g/cm³, an aluminum part is roughly 60% lighter for the same volume.
Can zinc die castings be machined to tight tolerances?
Yes. Zinc machines cleanly at high cutting speeds. On our 5-axis centers we hold ±0.005 mm on zinc parts when the fixture supports the thin sections.
The risk is clamping, not cutting. Zinc is soft, so heavy clamping pressure deforms thin walls before the tool engages. Light passes and proper support solve most of it.
What temperature limit should I design to for zinc?
Keep sustained loads below 60 °C where possible. Between 60 °C and 100 °C, run a creep check and favor Zamak 5 or ZA alloys with copper.
Above 100 °C, treat zinc as a candidate only after analysis. For continuous service near or above that range, aluminum is usually the better material.
Why does lead content matter so much in zinc alloys?
Lead, tin, and cadmium sit at the grain boundaries and cause intergranular corrosion. The part can grow dimensionally or crack, sometimes months after assembly.
Specification grades hold these elements very low. Buying to a named alloy such as Zamak 3 or Zamak 5, rather than a generic zinc ingot, is the simple way to avoid the problem.
Can zinc parts be plated or coated?
Yes. Zinc die castings take electroplating, powder coating, and painting well. The as-cast surface is smooth enough that pre-polishing is often minimal.
We run anodizing, electroless nickel, zinc and other plating, powder coating, black oxide, bead blasting, and laser marking on zinc parts. Laser marking needs a minimum character height of 1.5 mm.
Send Us Your Zinc Part Drawing
We will review the geometry, flag creep and wall-thickness risks, and return a quotation with free DFM analysis within 12 hours. No minimum order quantity, from one prototype to 10,000+ parts.
12-hour quote±0.005 mm tolerance100% inspectionNDA on request









