CNC machining cast iron parts: what the graphite actually does
This page explains how the graphite structure inside gray, ductile and nodular iron changes cutting behavior, chip formation, damping and the tolerances you can hold. It is written for design engineers and buyers who need to decide whether a cast iron part should be machined, and how to specify it without surprises.
In this article
- 1
- 2
- 3
- 4
- 5
- 6
- 7
- 8
Key takeaways
What graphite does inside cast iron
Cast iron is not one material. It is a family of iron-carbon-silicon alloys where carbon sits mostly as free graphite rather than dissolved in the matrix. That single fact drives everything about how the metal cuts, how it damps vibration, and how it fails. The graphite forms either as flakes, as in gray iron, or as nodules, as in ductile iron.
In gray iron the flakes are sharp and interconnected. They interrupt the metal matrix on a microscopic scale, so a cutting edge never faces a continuous wall of steel. Chips break into short segments instead of forming long strings. That is why gray iron machines cleanly at high surface speeds with modest cutting forces.
Ductile iron behaves differently. Magnesium or cerium additions spheroidize the graphite, so the matrix stays continuous and the alloy reaches tensile strengths that gray iron cannot. The trade-off is that ductile grades resist the cutting edge more and generate longer chips. Tool selection and feed rates need to shift accordingly.
Silicon content matters too, typically 1.8–3.0% in gray iron. Higher silicon promotes graphitization and improves machinability, but it also raises hardness at the edges of a thick section. A part cast at 40 mm wall thickness will not machine the same as one at 8 mm.
- 1Gray iron (flake graphite)Best machinability, highest damping, lower tensile strength.
- 2Ductile iron (nodular graphite)Higher strength and elongation, more tool pressure, longer chips.
- 3Malleable and compacted graphiteIntermediate behavior; confirm the grade before quoting cycle time.
Speeds, feeds and tool life on cast iron
The common claim that cast iron is easy to machine is half true. It cuts at high surface speed, often 150–250 m/min with coated carbide, and it produces a good finish without much effort. What wears tools is abrasion. Graphite flakes and residual sand from the mold act like a fine grinding compound on the flank face.
For gray iron, uncoated or TiAlN-coated carbide inserts work well. Depths of cut around 1–3 mm per pass on roughing, with feed rates near 0.15–0.3 mm per tooth, keep the insert cool and the chip short. Running too light a feed rubs the edge and accelerates wear.
Ductile iron pushes you toward tougher substrates and slightly lower speeds, roughly 100–180 m/min. Cutting forces are higher, so rigidity in the setup matters more than spindle speed. A 4,000 mm maximum processing size machine with a Ø400 mm rotary table handles large housings, but the fixture must be as stiff as the casting.
Coolant is a decision point. Many shops run cast iron dry or with air blast because the graphite dust turns coolant into a sludge that clogs filters and stains the machine. Mist or high-pressure air through the spindle clears chips and keeps the work area manageable. Flood coolant is still used on ductile iron where heat builds.
- 1Surface speed150–250 m/min for gray iron, 100–180 m/min for ductile.
- 2Feed per tooth0.15–0.3 mm; avoid very light passes that rub the edge.
- 3CoolingAir blast or mist is usually enough; flood only when heat demands it.
Tolerances, datums and features worth machining
Machining is applied selectively to a casting. Foundries hold as-cast tolerances around ±0.5 mm on small features and looser on large ones, so a machined casting usually starts with 1–3 mm of stock on critical faces. Machining brings those faces to ±0.005 mm where the drawing requires it and leaves the rest as cast.
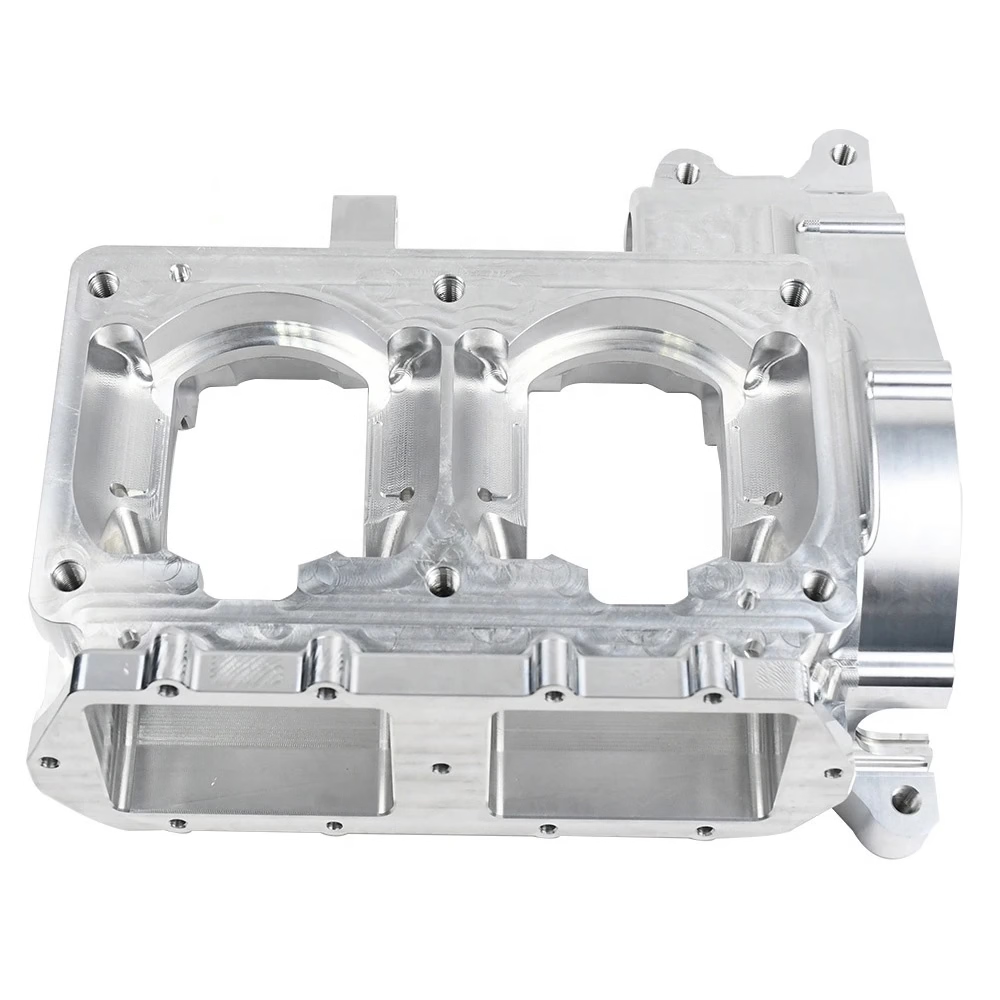
The datum question comes first. Castings have draft angles and parting lines, so a raw surface is a poor reference. We pick machined datums, usually a primary face and two locating holes, and fixture from those. Everything else is measured back to them. This is standard practice on housings, bearing caps and machine bases.
Not every surface should be machined. Adding a machined face costs setup time and can break through a thin wall. If a surface only needs to look clean, bead blasting may be the better answer. Machining earns its cost on sealing faces, bearing bores, bolt patterns and any feature that must locate another part.
Wall thickness is the practical limit. A casting with 4 mm walls will deflect under clamping pressure before the tool touches it. We check wall thickness from the model or a section scan before promising a tolerance, and we recommend adding ribs or bosses rather than chasing a number the casting cannot hold.
- 1Machine theseSealing faces, bearing bores, bolt circles, datum pads.
- 2Leave as castNon-critical outer surfaces, cosmetic faces, deep pockets.
- 3Check firstWall thickness, draft angle, parting line location, core shift.
Measuring and verifying machined castings
A machined casting has two error sources that stack: the casting itself and the machining. Core shift can move an internal bore by 0.3 mm without any tool error. If we measure only the finished feature, the cause of a deviation stays hidden. So inspection starts with the raw casting.
We check incoming castings for hardness, wall thickness at selected points, and surface defects before any setup. Hardness spots above the drawing range are the usual reason a batch machines differently from the last one, even with identical programs.
During machining, in-process probing catches drift on long runs. Final inspection covers every part before shipment, with dimensional reports available on request. For sealing faces and bearing bores we report flatness and roundness rather than a single diameter, because those are what the assembly actually feels.
If a feature is out of tolerance, the useful question is which side moved. A bore that is round but displaced points to core shift. A bore that is on center but oval points to clamping distortion. The fix is different in each case, so the measurement report should separate them.
- 1IncomingHardness, wall thickness, visual defects.
- 2In processProbe key datums on long production runs.
- 3Final100% dimensional check; reports on request.
Surface finish and secondary operations
Cast iron finishes well. A sharp insert at the right feed produces Ra 0.8–1.6 μm on a machined face without polishing. Pushing toward Ra 0.2–0.8 μm is possible on bearing bores, but it takes a finishing pass with a wiper insert and a rigid setup. Chasing that number across a whole part usually costs more than it returns.
Castings have a skin. The outer millimeter contains sand, oxides and chilled iron that is harder than the core. The first pass removes it, and tool life improves noticeably after that. On heavily scaled parts we take a deeper first cut rather than several light ones, so the edge spends less time in the abrasive skin.
For appearance, bead blasting gives a uniform matte gray and hides small surface defects. Powder coating and black oxide both bond well to a blasted surface. Masking matters: threads, bores and datum faces must stay clean, and masking adds a step to the process plan.
Laser marking works on cast iron with a minimum character height of 1.5 mm. Smaller text fills in because the graphite surface scatters the beam. If a part number must be legible after painting, mark it before coating or increase the character size.
- 1As machinedRa 1.6–3.2 μm, fine for non-sealing surfaces.
- 2Fine finishRa 0.8–1.6 μm with a wiper insert; Ra 0.2–0.8 μm on bores.
- 3AppearanceBead blasting, then powder coat, black oxide or paint.
When machining a casting beats machining from solid
The decision is volume and geometry. Cutting a complex housing from a 200 kg steel block wastes most of the material and hours of spindle time. A near-net casting arrives at 30 kg with the internal passages already formed, and machining only touches the critical faces.
Below roughly 50 parts, the pattern and tooling cost can outweigh the saving. Above that, castings usually win on cost per part and on lead time, because less metal has to be removed. Thin ribs, internal cavities and non-machinable geometry are possible only as cast features.
The counter-case is strength and consistency. A wrought or forged blank has no porosity, no core shift and a known grain direction. For a part that sees fatigue loading or must hold a tight tolerance across a thin section, machining from solid bar or plate is often the safer route, even at higher cost.
There is a middle path. We can machine from a casting and verify the result, or start from solid stock and keep the design simple enough to avoid casting defects. Both routes are quoted side by side when the geometry allows it, so the comparison is based on your drawing rather than a rule of thumb.
- 1Choose a castingComplex internal form, high volume, large size, vibration damping needed.
- 2Choose solid stockLow volume, thin walls, fatigue-critical, tight tolerance on thin sections.
- 3Ask for bothWe quote casting and solid routes when geometry permits.
Gray iron vs ductile iron for machined parts
Ranges reflect typical practice, not a guarantee for every grade.
| Factor | Gray iron | Ductile iron | Practical note |
|---|---|---|---|
| Graphite form | Flakes | Nodules | Drives chip shape and damping |
| Typical hardness | 150–220 HB | 170–250 HB | Abrasion is the wear driver |
| Damping capacity | Highest | Moderate | Matters on machine bases |
| Tensile strength | Lower | Higher | Ductile carries shock loads |
| Chip behavior | Short, broken | Longer, stringy | Peck cycles on ductile |
| Surface speed | 150–250 m/min | 100–180 m/min | Adjust for tool coating |
| Best use | Housings, bases | Gears, cranks, shock parts | Match grade to load case |
Which route to pick
If the part is a large housing with internal passages and you need damping, machine a casting. If it is thin-walled, low volume or fatigue-critical, machine from solid. Send the drawing and we will price both and tell you which one holds tolerance more reliably.
Common questions
Does cast iron need coolant when machining?
Usually not. Gray iron cuts well dry or with an air blast, and dry cutting keeps graphite dust out of the coolant tank. Ductile iron generates more heat, so mist or flood coolant helps on heavier cuts.
The exception is deep holes and fine finishes, where chip evacuation and heat control matter more than dust. We decide per operation, not per material.
Can you hold ±0.005 mm on a machined casting?
Yes, on machined features that are fixtured from a machined datum. The tolerance applies to the feature we cut, not to the raw casting surface.
Castings move slightly after cooling and after stress relief. If a tight tolerance sits on a thin wall, we check wall thickness first and may recommend a design change.
What causes porosity to show up after machining?
Porosity sits below the surface and only appears when the cut reaches it. Gas holes, shrinkage voids and sand inclusions all behave this way.
The fix is usually a casting process change, not a machining change. If a bore must be pressure-tight, we can machine a test cut and inspect before running the batch.
How do you handle clamping distortion?
Castings are less stiff than steel, so over-tightening a vise bows the part and the bore comes out oval. We use soft jaws, minimal clamping force and support under the wall.
On thin housings we sometimes rough, release the clamps, then finish in a second setup. It costs one extra operation and removes most of the distortion.
Can machined castings be plated or coated?
Yes. Electroless nickel, zinc plating, powder coating and black oxide all work on cast iron. Bead blasting first gives better adhesion and a more even color.
Graphite at the surface can cause small pits in some plating baths. If appearance is critical, tell us the coating before we plan the finishing pass.
What lead time should we plan for?
Quotation and DFM feedback come back within 12 hours, and production can start within 24 hours once the drawing and stock are confirmed. Machined parts typically ship in 3–5 days.
Casting supply is separate. If the casting is not already available, add the foundry lead time to that number, and we will flag it at quoting.
Send your casting drawing
Tell us the grade, the critical features and the tolerance that matters. We will confirm machinability, flag core shift or thin-wall risks, and quote the machined features within 12 hours.
12-hour quote100% inspectionNo minimum order quantityNDA on request
More from the shop floor
We publish setup notes, tooling trials and inspection data from the factory floor.