GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Motorcycle Parts · Precision Machining

CNC Machining for IVC Customer Motorcycle Parts

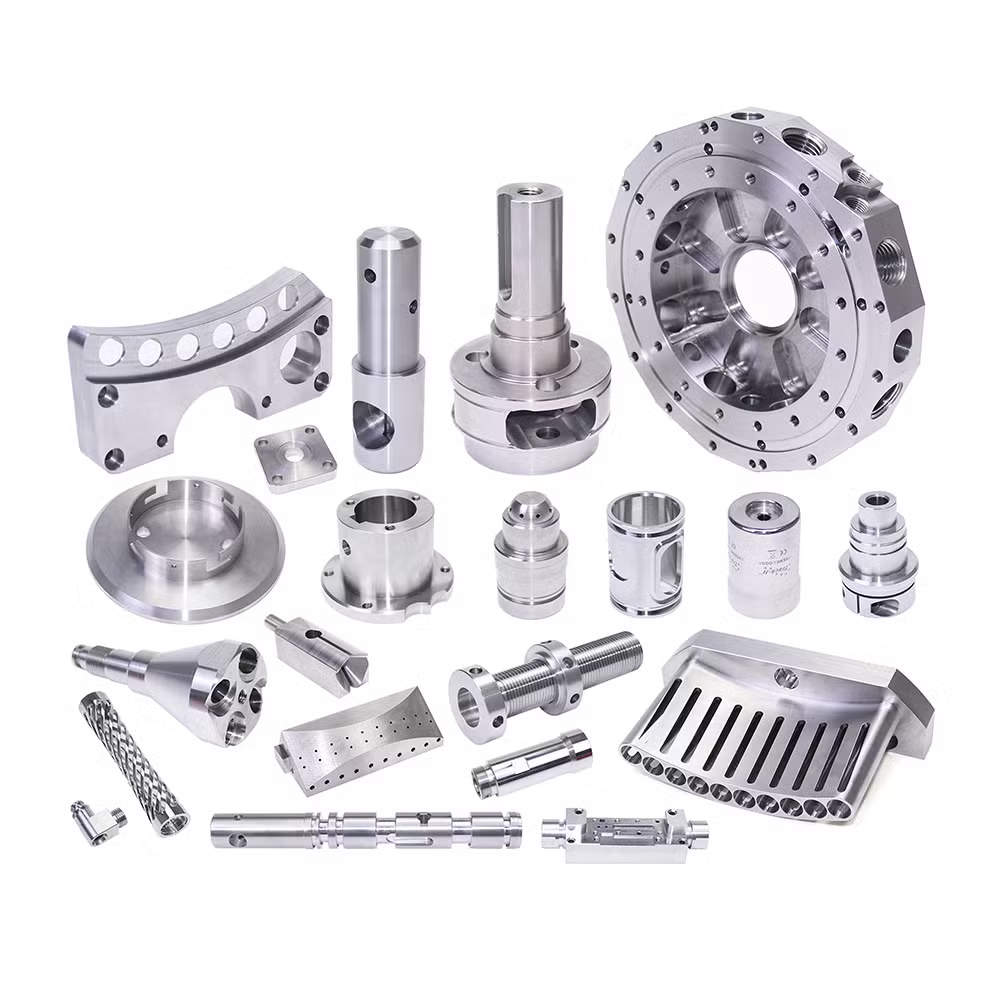
We machine IVC customer motorcycle parts from your 3D model and 2D drawing: triple clamps, fork caps, linkage plates, engine covers. 5-axis milling and turning in aluminium and stainless steel, held to ±0.005 mm, with 100% inspection before shipment.

±0.005 mm tolerance16 five-axis centersNo minimum order quantityQuote in 12 hoursIATF 16949:20163–5 day shipping
low volume manufacturing
16Simultaneous 5-axis centers
±0.005 mmMachining tolerance
99.99%Qualification rate
150Technicians on the floor
Why rebuilds go wrong

Four problems we see on IVC customer motorcycle part orders

Most of these show up after the parts arrive, not on the drawing.

01

Fork caps that do not seat

A 0.05 mm error on a fork cap thread means the cap bottoms out before the O-ring seals. Oil weeps past the threads, damping changes, and the rider feels it in the first lap. We hold thread fits to ±0.005 mm and check pitch diameter with thread gauges before the parts leave the floor.

02

Triple clamps with uneven clamping load

If the fork bore and the steerer bore are not coaxial, the clamp pinches the fork tube on one side. The fork binds, and stiction rises. We bore both features in one setup on a 5-axis center so the center distance stays true from the first part to the last.

03

Linkage plates that ovalize under load

A linkage plate as-machined from 6061-T6 can look fine on the bench and still flex on the track. We check wall thickness against your load direction and suggest 7075-T6 or a ribbed section when the plate is asked to carry more than the drawing implies.

04

Engine covers that crack at the bolt holes

Sharp internal corners at bolt bosses concentrate stress. A small fillet and a change in the spot-face depth often removes the failure. Our free DFM analysis flags these before cutting metal, so you are not paying for a second run.

How we machine motorcycle parts

One setup for concentric features, held to ±0.005 mm

Two capabilities do most of the work on IVC customer motorcycle parts.

cnc machining
5-axis milling

Complex geometry in one setup

Triple clamps, fork lugs, and linkage plates carry bores and faces on several planes. If each face is cut in its own setup, each setup adds its own error. We run these parts on 16 simultaneous 5-axis machining centers, so the fork bore, steerer bore, and caliper mounts come off the same zero.

Our rotary table is Ø400 mm, and the largest travel is 4,000 × 400 × 150 mm. That covers a full triple clamp, a swingarm section, or a set of matching brackets in one batch. Small runs are fine: no minimum order quantity, from one prototype to 10,000+ parts.

  • 1
    Concentric boresFork and steerer bores cut in one setup, so center distance holds.
  • 2
    Thin wallsLight finishing passes and support where the wall is under 2 mm.
  • 3
    UndercutsTilted tool access reaches faces a 3-axis machine cannot.

Get Instant Quote

cnc machining
Turning and mill-turn

Round parts with cross features finished in one cycle

Axle spacers, fork caps, and shock-eye bushings are turned parts until they are not. A cross hole, a flat, or a slot usually means a second operation on a mill, and that is where runout creeps in. Our 16 mill-turn centers cut the OD, the thread, and the cross features in one cycle.

Thread fits on fork caps and axle nuts are checked with go/no-go gauges. Surface finish lands at Ra 0.8–1.6 μm on sealing diameters, and we can push to Ra 0.2–0.8 μm when a fork tube or a shock shaft needs it.

  • 1
    One-cycle partsOD, thread, and cross holes finished without re-chucking.
  • 2
    Thread controlPitch diameter gauged on every batch, not sampled.
  • 3
    Sealing surfacesRa 0.8–1.6 μm standard, finer on request.
Material and finish choices

What we recommend for common motorcycle parts

PartMaterialFinish
Triple clamp7075-T6 or 6061-T6Hardcoat anodize, black
Fork cap6061-T6Clear anodize
Linkage plate7075-T6Bead blast, clear anodize
Engine cover6061-T6Powder coat or anodize
Axle spacer304 or 316 stainlessAs machined or tumble
Shock eye bushingBronze C93200As machined
Exhaust bracket304 stainlessBrushed
Master cylinder cap6061-T6Hardcoat anodize
What we do

Services behind a motorcycle part order

You can place the whole job, prototype through production, with one supplier.

01

5-Axis Machining

Complex parts with bores and faces on multiple planes, cut in one setup to ±0.005 mm.

02

4-Axis and 3-Axis Machining

Prismatic brackets, plates, and covers where a single index is enough and cost matters.

03

CNC Milling & Turning

Round parts with cross features finished in one cycle on mill-turn centers.

04

Rapid Prototyping

Fit checks and track tests before you commit to a production run.

05

Surface Finishing

Anodize, plating, powder coat, bead blast, and laser marking.

06

Sheet Metal & Casting

Brackets, guards, and housings when machining from billet is not the right call.

Scope and limits

What a typical motorcycle part order includes

ItemWhat we deliver
Drawing reviewFree DFM analysis and quote within 12 hours
Tolerance±0.005 mm on critical features, tighter on request
Surface finishRa 1.6–3.2 μm as machined, Ra 0.2–0.8 μm when needed
Inspection100% before shipment, reports on request
DocumentsMaterial certs and inspection reports available
ConfidentialityNDA available on request, uploads kept secure
Lead timeProduction can start within 24 hours
ShippingParts ship in 3–5 days after completion
Why GreatLight

Numbers behind the parts we ship

These are the figures that decide whether a run goes smoothly.

15Y

Machining since 2011

Fifteen years of production work, with 3 wholly-owned plants and 7,600 m² of manufacturing space in Dongguan and Singapore.

127

High-precision CNC machines

16 simultaneous 5-axis centers, 12 four-axis mills, 27 three-axis machines, and 16 mill-turn centers under one roof.

±0.005 mm

Held on critical features

Bores, threads, and sealing diameters checked with gauges and CMM reports on request.

99.99%

Qualification rate

Raw material check, in-process monitoring, and final inspection on every order.

12 h

Quote and DFM analysis

Send a 3D model and 2D drawing, and we return a cost estimate and lead time.

4,000 mm

Maximum part size

Travel up to 4,000 × 400 × 150 mm, plus a Ø400 mm rotary table for indexed work.

15 yearsMachining experience
7,600 m²Manufacturing space
3Wholly-owned plants
150Technicians
Sector requirements

What motorcycle work demands, and what we deliver

cnc machining

Suspension and chassis

Triple clamps and linkage plates need concentric bores and stable wall sections. We cut both bores in one setup and check center distance before shipment.

  • ±0.005 mm
  • One-setup bores
  • 100% inspection
cnc machining

Engine and drivetrain

Covers and housings need flat gasket faces and clean bolt-hole edges. We machine the gasket face and the bolt pattern on the same zero, then deburr every hole.

  • Flatness held
  • Deburred edges
  • IATF 16949:2016
cnc machining

Custom and one-off builds

One-off brackets and adapters are quoted the same way as production runs. No minimum order quantity, and the file set carries over when the design is ready for a run.

  • No MOQ
  • 3–5 day shipping
  • 12-hour quote
FAQs

Questions we get on IVC customer motorcycle part orders

What files do you need for a quote?

A 3D model in STEP or IGES plus a 2D drawing with tolerances, material, and finish. If you only have a model, we can work from that and flag the features that need a tolerance call.

Mark which dimensions are critical. That lets us plan the setup and the inspection around the features that actually matter.

Can you machine a single prototype part?

Yes. There is no minimum order quantity, so one part and a 10,000-part run go through the same process.

For prototypes we often start from billet and skip hard tooling. When the design is frozen, the same file set moves to the production run.

Which aluminium should I use for a triple clamp?

7075-T6 when stiffness and strength matter most, and the part will be anodized. 6061-T6 when you want easier machining, better weldability, or lower cost.

Both machine well. The choice comes down to load path and how the part is finished.

How do you hold ±0.005 mm on a thin-walled part?

Light finishing passes, sharp tooling, and support on the unsupported side. We also leave stock so the part does not move while it is being cut.

If a wall is under 2 mm, we may suggest a small design change. A rib or a slightly thicker section often costs less than chasing the tolerance.

What surface finishes are available?

Anodizing in clear, colour, hardcoat, and conductive grades. Electroless nickel, zinc, silver, and gold plating. Powder coating and black oxide.

Bead blasting, tumbling, brushing, and polishing. Laser marking with a minimum character height of 1.5 mm.

Can you inspect parts and send reports?

Every order gets a raw material check, in-process monitoring, and a final inspection. That is 100% inspection before shipment, not sampling.

Dimensional reports, material certificates, and CMM results are available on request.

How do you keep my design confidential?

Uploads are kept secure, and we sign an NDA on request before files are shared.

Only the people who need the files to quote or machine the part see them.

What is the lead time for a motorcycle part order?

Quote and free DFM analysis come back within 12 hours. Production can start within 24 hours of approval, and parts ship in 3–5 days after completion.

The exact schedule depends on part count and finishing. We confirm it with the quote.

Send your motorcycle part files for a quote

Upload a 3D model and 2D drawing. You get a cost estimate and DFM analysis within 12 hours, and every part is inspected before it ships.

12-hour quote100% inspectionNo minimum order quantity

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC