
5 Essential 3D Milling Secrets to Boost Precision and Slash Machining Costs
This guide is for engineers and buyers who need contoured, curved and sculpted parts held to tight tolerances without paying for rework. It covers five decisions that let 3D milling boost precision while removing cost from the cycle: toolpath strategy, cutter selection, machine and fixture rigidity, material behavior, and how a shop structures its process. Read it and you can tell whether a quoted process will hold your tolerance or quietly drift.
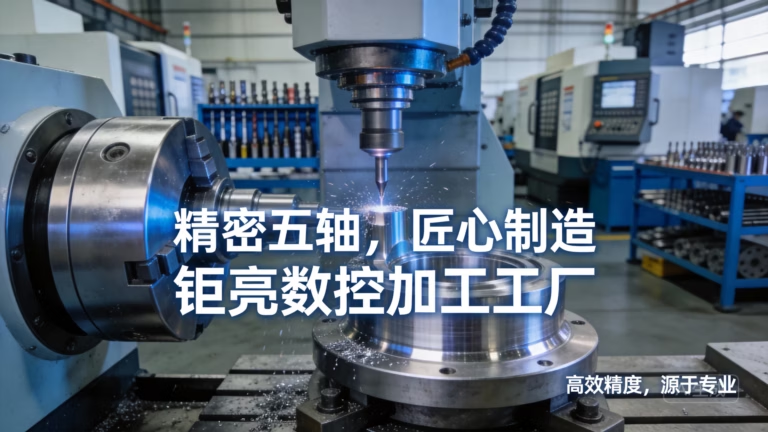
Precision and cost are set before the spindle starts
Five areas decide whether a contoured part comes off the machine in tolerance, and how many hours it takes to get there.
Toolpath logic: keep the cutter engaged and the load steady
Treating 3D milling as 2.5-axis work with one extra axis is the most common reason a contoured part runs long and drifts out of tolerance. The advantage of simultaneous five-axis and well-planned three-axis toolpaths is constant tool engagement. When the cutter stays in contact with a consistent radial and axial depth, the cutting force stays predictable, deflection stays small, and the finishing pass removes a uniform chip instead of scraping through peaks and valleys left by a rougher.
Sharp internal corners are where this breaks down. A tool forced into a corner sees its engagement angle spike, chip thickness climbs, and the tool pushes off the wall. The shop reacts by slowing the feed, which adds cycle time, or by leaving extra stock for a second finish pass, which adds more. Neither fixes the root cause. A trochoidal or constant-engagement roughing path keeps the load even and lets the same tool run faster without chatter.
On sculpted surfaces, a barrel cutter with a large radius and a tilted tool axis changes the arithmetic. The effective contact area is wider, so fewer passes cover the same surface, and the form error from scallop height drops. This is where 3D milling can boost precision and cut time at once, because fewer passes means less tool wear and fewer opportunities for the machine to drift.
Simulation earns its keep here. Verifying stock removal, holder clearance and axis travel in CAM before the part is on the table catches collisions and over-travel that would otherwise cost a setup. For parts with deep pockets or undercuts, that check is faster than a trial cut in aluminium.
- 1Constant engagementKeeps radial and axial load steady, so feed rates stay high and deflection stays low.
- 2Barrel cuttersWide contact patch on curved faces; fewer passes, lower scallop height.
- 3Simulation firstCheck holder and axis clearance in CAM before the first cut.
The cutter is a process variable, not a consumable
A cutter chosen by price alone will cost more in the long run. Geometry decides what the tool can do: variable helix and unequal flute spacing break the harmonic that causes chatter, a relieved neck lets the tool reach into a deep pocket without rubbing, and a corner radius spreads load across the tip instead of concentrating it at a sharp point. For finishing a curved surface, the nose radius and the stepover together set the scallop height that a customer can measure.
Tool life is not a single number. Heat, abrasion and built-up edge each wear a tool differently, and the coating has to match the material. TiAlN coatings hold up in dry or near-dry cutting of steels and stainless, while uncoated or DLC-coated tools suit aluminium where built-up edge is the main failure mode. Running a tool past its wear limit changes the effective diameter, and that shows up as a dimension that drifts across a batch.
A practical rule: measure the finished surface if the tolerance is tight. A worn 6 mm ball nose can lose enough material at the tip to move a profile by more than the tolerance band. Changing tools on a schedule based on cut time or removed volume, not on the sound of the cut, keeps the last part as good as the first.
- 1Variable helixBreaks chatter harmonics in deep pockets and thin walls.
- 2Coating matchTiAlN for steel and stainless; DLC or uncoated for aluminium.
- 3Change on scheduleWear shifts effective diameter; time-based swaps beat sound-based.
Invisible flex and thermal drift are tolerance killers
A machine that is rigid on paper can still flex in the cut. The chain runs from the tool holder through the spindle, the column, the fixture and the table. Any soft link shows up as a dimension that changes with depth of cut. Shrink-fit or hydraulic holders reduce runout compared with a worn collet, and a fixture that supports the part close to the cutting zone limits the deflection that no toolpath can compensate for.
Thermal growth is the quieter problem. A spindle running for hours warms and extends; chips carry heat into the workpiece; the shop warms in the morning. On a 500 mm feature, a 20 °C swing on aluminium can move the part by more than 0.02 mm. Shops that hold ±0.005 mm manage this with warm-up cycles, coolant temperature control and finishing passes run after the machine has reached steady state.
The measurement side matters just as much. A part measured hot on the machine will read differently on a granite plate an hour later. If the drawing tolerance is ±0.005 mm, the inspection temperature and the machine temperature should be close, and the report should say what they were.
- 1Holder runoutShrink-fit or hydraulic holders cut runout versus worn collets.
- 2Fixture supportSupport near the cut limits part deflection the toolpath cannot fix.
- 3Thermal steady stateWarm-up cycles and coolant control keep dimensions stable.
When each material and process choice fits
Use this to judge which route suits a part before asking for a quote.
| Material | Typical 3D milling use | Watch point |
|---|---|---|
| 6061-T6 aluminium | Prototypes, housings, brackets | Built-up edge; keep coolant and sharp flutes |
| 7075 aluminium | Aerospace ribs, high-strength frames | More prone to chatter; lighter depths of cut |
| 316L stainless | Medical and food-contact parts | Work hardens; avoid dwelling in the cut |
| Ti-6Al-4V | Implants, aerospace fittings | Low thermal conductivity; heat stays in the tool |
| 17-4PH (SUS630) | Valve bodies, shafts | Condition affects machinability; confirm temper |
| PEEK / POM | Insulators, seals, light parts | Clamp gently; plastic deflects under load |
| Inconel | Hot-section and high-temp parts | Very low speeds; tool wear drives cost |
Pick the stock form before you pick the cutter
The starting stock shape sets how much metal the machine has to remove, and removal is where the hours go. A part machined from a solid billet may take three times the cycle of the same part cut from a near-net forging or casting. The trade is real: near-net stock costs more up front, needs a first-article check for stock condition, and can hide porosity. For low volume the billet usually wins; for a run of hundreds the near-net route often pays back in cycle time and tool life.
Material choice also moves the achievable finish. Aluminium and brass cut cleanly and reach Ra 0.8–1.6 μm without a separate operation. Titanium and Inconel hold that finish only with slower passes and fresh tools. If the drawing calls for Ra 0.2–0.8 μm, plan a finishing pass with a small stepover or a separate polishing step rather than asking a roughing tool to do two jobs.
Wall thickness is the other constraint. Thin walls deflect under cutting force, so the toolpath has to balance material removal on both sides. Where a wall is under about 1 mm, the fixture and the pass order matter more than the cutter. This is a good place to talk to the shop early, because moving a rib or adding a temporary support feature can turn an unstable part into a straightforward one.
- 1Billet vs near-netBillet suits low volume; near-net pays off on longer runs.
- 2Finish by materialAluminium and brass finish easily; titanium needs slower passes.
- 3Thin wallsBelow ~1 mm the fixture and pass order dominate the result.
Match the shop's process architecture to your tolerance
A quote tells you the price. It does not tell you whether the shop can hold the tolerance on the last part of the run. Ask what machines the part will run on, how the fixture is planned, and how the first article is checked. A shop with simultaneous five-axis centers, a Ø400 mm rotary table and 4,000 mm travel can machine a part in one setup that would need three on a three-axis machine, and each removed setup removes a source of stacked error.
Inspection is the other half. In-process monitoring catches a drift before the batch is finished; a final check on a granite plate or CMM confirms it. Ask for the report if the part is critical. For medical and automotive work, the quality system matters as much as the machine: ISO 9001:2015 and IATF 16949:2016 cover process control, and ISO 13485:2016 covers medical devices.
GreatLight runs 127 high-precision CNC machines across three plants, including 16 simultaneous 5-axis centers and 16 mill-turn centers, with tolerance held to ±0.005 mm and 100% inspection before shipment. Quotation and a free DFM analysis come back within 12 hours, production can start within 24 hours, and uploads stay confidential with an NDA available on request.
- 1One setup, fewer errorsFive-axis work removes stacked setup error from the tolerance chain.
- 2Check the first articleConfirm how the shop verifies the first part before the run.
- 3Ask for the reportInspection data on request for critical dimensions.
Common questions on 3D milling precision and cost
What tolerance can 3D milling realistically hold?
On a rigid machine with the right fixture, ±0.005 mm is achievable on critical features in aluminium and steel, and ±0.0002 in for those who work in imperial units. The limit is usually the part, not the machine: thin walls, long tools and deep pockets all reduce what the process can hold.
If a feature needs tighter than that, the answer is often a different process or a secondary operation, not a slower cut on the same setup.
When is five-axis 3D milling worth the extra cost over three-axis?
When the part has undercuts, contoured faces that would need multiple setups, or deep pockets that a three-axis spindle cannot reach without a long, flexible tool. Five-axis lets the shop tilt the tool and use a shorter, stiffer cutter.
For flat parts with holes and simple pockets, three-axis is cheaper and just as accurate.
How do I reduce machining cost without losing precision?
Start with the stock form and the tolerances on the drawing. Relaxing a non-critical tolerance from ±0.005 mm to ±0.05 mm can remove a finishing pass. Choosing near-net stock on a longer run cuts cycle time. And designing so the part can be machined in fewer setups removes both time and stacked error.
None of these changes touch the features that actually matter.
Why does my part measure differently on the CMM than on the machine?
Temperature is the usual cause. The machine, the part and the chips are warmer than the inspection room. On aluminium, a 20 °C difference can move a 500 mm feature by more than 0.02 mm.
Let the part stabilize at inspection temperature, and confirm that the machine and the CMM agree on the datum.
Which materials machine well with 3D milling?
Aluminium grades such as 6061, 7075 and 6082 cut fast and finish cleanly. Brass and copper alloys machine well too. Stainless and titanium are machinable but slower, and tool wear drives the cost more than the machine time.
Plastics like POM, PEEK and ABS machine cleanly if the fixture supports them and the clamps do not crush the part.
How is chatter fixed on a contoured surface?
Chatter is a stiffness problem, not a feed problem. Shorten the tool overhang, use a holder with low runout, support the part closer to the cut, and switch to a variable-helix cutter if the wall is thin.
Lowering the feed can hide it, but it does not remove the vibration, and it adds cycle time.
Send your 3D milling part for a process review
Upload a STEP file and we will return a quotation with a free DFM analysis within 12 hours.
12-hour quote±0.005 mm tolerance100% inspectionNo minimum order quantity









