GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

CNC Turned Parts

CNC Turned Parts Manufacturer Serving Georgia

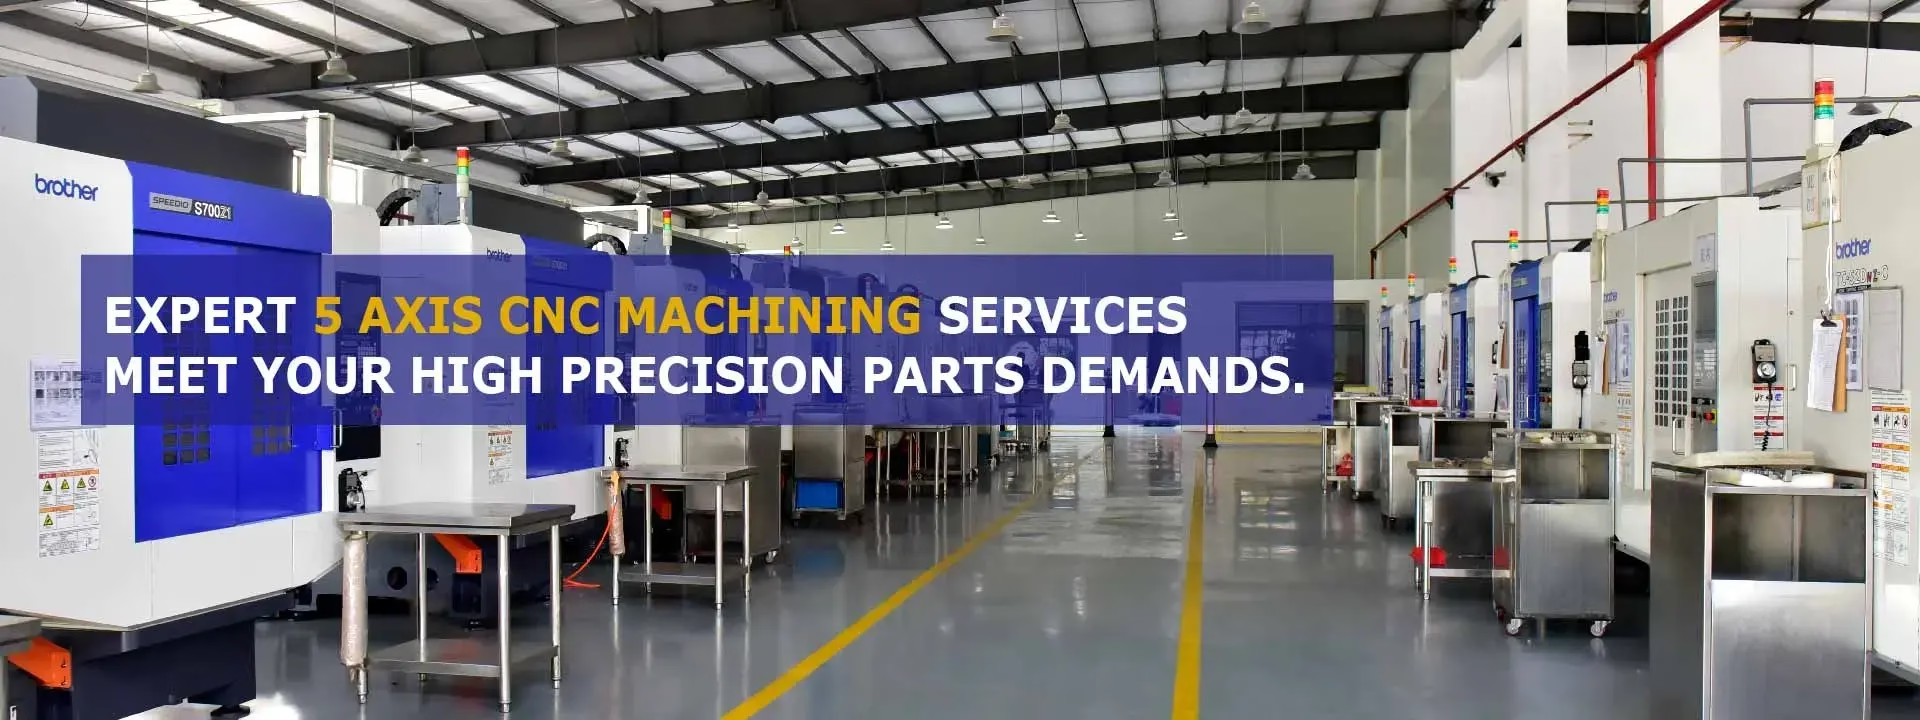
GreatLight turns shafts, bushings, fittings, pins and threaded parts from bar stock on 127 CNC machines, with 16 mill-turn centers for parts that need turning and milling in one setup. Tolerances to ±0.005 mm, 100% inspection before shipment.

Ø1–Ø400 mm turned parts±0.005 mm toleranceRa 0.2–0.8 μm finishNo minimum order quantitySteel, stainless, brass, titanium12-hour quote + DFM
greatlight-cnc-machining-center-11 (1)
16Mill-turn centers for one-setup parts
±0.005 mmTurning tolerance on qualified jobs
99.99%Qualification rate before shipment
3–5 daysTypical time from release to shipping
Where turned parts go wrong

Four Problems Georgia Buyers Bring Us

Most of these show up after the first article is approved, not before.

01

Concentricity drifts after the second setup

A shaft turned in two operations and then milled on a separate machine picks up runout from re-chucking. If the drawing calls 0.010 mm TIR and the process stacks three setups, the second lot will not hold it. Runout is the most common reason a turned part fails incoming inspection.

02

Lead time stretches while the shop re-quotes

Bar stock gets ordered late, a second supplier is pulled in, and the release date slides by weeks. Every extra handoff adds a week. Production lines in Georgia do not have that buffer when a change order lands on Friday.

03

Threads and finishes do not match the drawing

Rolled threads on a turned pin can measure oversize on pitch diameter even when the major diameter looks right. A callout of 6g class within a few tenths needs gauging, not a caliper check. Plating adds thickness too, and the drawing may not account for it.

04

Documentation does not survive an audit

Medical and automotive buyers need material certs, inspection reports and traceability tied to the lot. When the shop cannot produce them, the parts sit in quarantine. Re-inspection and paperwork alone can hold a shipment for weeks.

How we turn parts

One Shop from Bar Stock to Finished Turned Part

Turning, milling, finishing and inspection under one roof, so the setup count stays low.

5-axis-cnc-machining-services
Core capability 1

Mill-Turn Centers Cut the Setup Count

Most turned parts that fail are not hard to cut. They are hard to hold across setups. Our 16 mill-turn centers turn and mill in the same spindle, so a cross-hole, flat or slot does not require re-chucking on a second machine.

That matters on shafts with a keyway and a threaded end, or on valve bodies with an off-axis port. One clamping means one datum. Runout stays where the drawing puts it.

  • 1
    Ø400 mm rotary tableMulti-face work without repositioning the part between operations.
  • 2
    Bar feed to 4,000 mmLong shafts and tie rods turned in a single pass.
  • 3
    Live toolingCross-drilling, slotting and threading after the OD is turned.

Get Instant Quote

2c6f2510-rectangle-625
Core capability 2

Tight Tolerance Without a Second Vendor

Turning to ±0.005 mm is a process question, not a machine spec. It depends on tool wear tracking, thermal stability and a gauge that reads finer than the tolerance. We run in-process checks on the floor and a final dimensional pass on CMM before parts are packed.

If a part needs a ground finish or a specific Ra, we do not ship it out and wait. Bead blasting, tumbling, brushing, polishing, anodizing, plating and laser marking all run in-house. Laser marking holds a minimum character height of 1.5 mm.

  • 1
    Ra 0.2–0.8 μm availableFine turned or polished surfaces for sealing faces.
  • 2
    In-process CMM checksDimensional verification while the lot is still running.
  • 3
    100% inspection before shipmentRaw material check, in-process monitoring, final inspection.
Selection guide

Which Process Fits Your Turned Part

Use this to decide before you send the file.

Part featureProcess choiceWhy
Simple round shaft, one diameterSingle-spindle turningOne setup, fastest cycle
Shaft with keyway or cross-holeMill-turn centerHolds runout across both features
Valve body with off-axis portMill-turn or 5-axisOne datum, no re-chuck error
Long tie rod over 1,000 mmBar feed turningAvoids secondary straightening
Thin-wall bushingTurning with soft jawsControls ovality and wall thickness
Hardened pin over 45 HRCTurn soft, then grindTurning alone will not hold size
What we run

Turning and Support Services

One card, one process, one reason to use it.

01

CNC Turning

Bar-fed and chucked work from Ø1 mm to Ø400 mm for shafts, pins, spacers and fittings. Roundness and concentricity controlled in the same setup where the drawing allows it.

02

Mill-Turn Machining

16 mill-turn centers handle turned parts that need flats, cross-holes, slots or threads off the main axis. No second machine, no second datum.

03

4-Axis and 5-Axis Milling

12 four-axis mills and 16 simultaneous 5-axis centers cover prismatic features, angled faces and contoured geometry that a lathe cannot reach.

04

Rapid Prototyping

One-off turned prototypes before tooling or production release. Same machines and same inspection as the production run, so the prototype predicts the lot.

05

Surface Finishing

Anodizing, electroless nickel, zinc, silver and gold plating, powder coating, black oxide, bead blasting, tumbling, brushing and polishing in-house.

06

Inspection and Reporting

Material certificates, in-process CMM data and final dimensional reports on request, tied to the lot number for traceability.


Capability range

Turning Capability at a Glance

Numbers from our own equipment list, not a brochure range.

ItemRangeNotes
Turning diameterØ1 mm to Ø400 mmRotary table Ø400 mm available
Maximum part length4,000 mmBar feed and long-shaft turning
Tolerance±0.005 mm (0.0002 in)On qualified turning jobs
Surface finishRa 0.2–0.8 μm fineRa 0.8–1.6 μm standard
MaterialsSteel, stainless, brass, copperTitanium, Inconel, magnesium
Minimum orderOne prototypeRuns to 10,000+ parts
Quote turnaround12 hoursIncludes free DFM analysis
Production start24 hours after releaseSubject to material stock
Why GreatLight

Six Reasons Buyers Stay

Fifteen years in turning, three plants, one quality system.

15Y

Fifteen Years Turning

Founded in 2011, GreatLight has run turned work for aerospace, automotive, medical, robotics and industrial machinery programs since before mill-turn was standard in the shop.

127

High-Precision CNC Machines

127 machines across three wholly-owned plants in Dongguan and Singapore. Lathes, mills, mill-turn, 5-axis and finishing equipment in the same organization.

±0.005 mm

Held Tolerance

Turning tolerance to ±0.005 mm with gauge checks run in process, not only at final inspection. Reports available on request.

99.99%

Qualification Rate

Parts that pass full dimensional and visual inspection before shipment. 100% inspection, not sampling.

4

Certifications

ISO 9001:2015, IATF 16949:2016, ISO 13485:2016 and ISO 27001:2022 cover quality, automotive, medical and information security.

0

Minimum Order Quantity

From one prototype to 10,000+ part runs. No tooling charge to start, because turned parts need no mold.

7,600 m²Manufacturing space
150Technicians on staff
3Wholly-owned plants
<2%Historical late-delivery rate
Industry fit

What Each Industry Requires, and How We Meet It

CNC Machining Prototype Service Georgia

Automotive and EV Turning

Shafts, sensor housings and fittings machined to automotive drawing standards, with IATF 16949 process control and full lot traceability.

  • IATF 16949:2016
  • ±0.005 mm
  • Lot traceability
cnc-machining-hdpe

Industrial Machinery and Robotics

Bushings, pins, spacers and drive components turned from steel, brass and aluminum, sized for repeat assembly without hand fitting.

  • Steel and brass
  • Ra 0.8–1.6 μm
  • 100% inspection
option-1-concise-seo-focused

Medical Device Components

Turned stainless and titanium parts with documented material certificates and inspection records that hold up in a design-history review.

  • ISO 13485:2016
  • Material certs
  • Inspection reports
FAQs

Questions Georgia Buyers Ask Before Ordering

What is the smallest turned part you can quote?

We turn from Ø1 mm upward. Below Ø3 mm the limiting factor is usually the gauge, not the tool, because a tolerance of ±0.005 mm on a tiny pin needs a measuring method that reads finer than the tolerance.

Send the drawing and we will say whether the feature is measurable. If it is not, we will tell you before quoting.

Should my part be turned or milled?

If the shape is mostly round and the features sit on the centerline, turning is faster and cheaper. Flats, slots and cross-holes off the axis point to a mill-turn center, which does both in one setup.

Purely prismatic parts with no round feature belong on a mill. We will suggest the cheaper route when both work.

How do you hold concentricity on a multi-feature shaft?

We keep the part in one clamping wherever possible, using mill-turn centers with live tooling. When a second setup is unavoidable, we use soft jaws cut to the finished diameter so the re-chuck repeats.

Concentricity is checked in process, not only on the final part, so a drift is caught while the lot is still running.

Which materials do you turn most often?

Aluminum 6061, 6061-T6, 2024, 6082 and 7075; stainless 303, 304, 316, 316L, 17-4PH; steel 1018, 1045, 4140 and 4340; brass C36000 and C27400; titanium TC4.

Brass and free-machining stainless turn cleanest. Titanium and Inconel need slower speeds and more tool changes, which affects the quote.

Can you handle the finishing as well as the turning?

Yes. Anodizing, electroless nickel, zinc, silver and gold plating, powder coating, black oxide, bead blasting, tumbling, brushing, polishing and laser marking all run in-house.

Laser marking needs a minimum character height of 1.5 mm to be legible and repeatable.

What documentation comes with the parts?

Material certificates, in-process inspection data and a final dimensional report are available on request, tied to the production lot. For automotive programs we work to the IATF 16949 process controls.

If your audit needs a specific format, send the template with the order and we will fill it in.

How fast can you quote and ship?

Quotation with a free DFM analysis comes back within 12 hours. Production can start within 24 hours of release, and parts typically ship in 3–5 days, depending on material and finishing.

Our historical late-delivery probability is below 2%. We do not promise dates we cannot hold, so the schedule is confirmed after the material check.

Is there a minimum order quantity?

No minimum. We run from a single prototype to 10,000+ part runs on the same machines and the same inspection routine.

Turned parts require no tooling, so there is no reason to force a large first order.

How do you protect our design?

Uploads are handled as secure and confidential. An NDA is available on request before you send files, and we hold ISO 27001:2022 for information security.

Your designs are not shared with other customers or used outside your project.

Send Your Turned Part Drawing

Upload a STEP or PDF and get a quote with DFM feedback within 12 hours. No minimum order quantity, 100% inspection before shipment.

12-hour quote100% inspectionNo minimum orderNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC