
CNC machining nylon guide
Nylon machines fast, but it moves. This guide explains why PA parts grow, bow and burr, and which settings keep them in tolerance. Written for engineers who need to decide between PA6, PA66 and PA12 before the tool hits the stock.
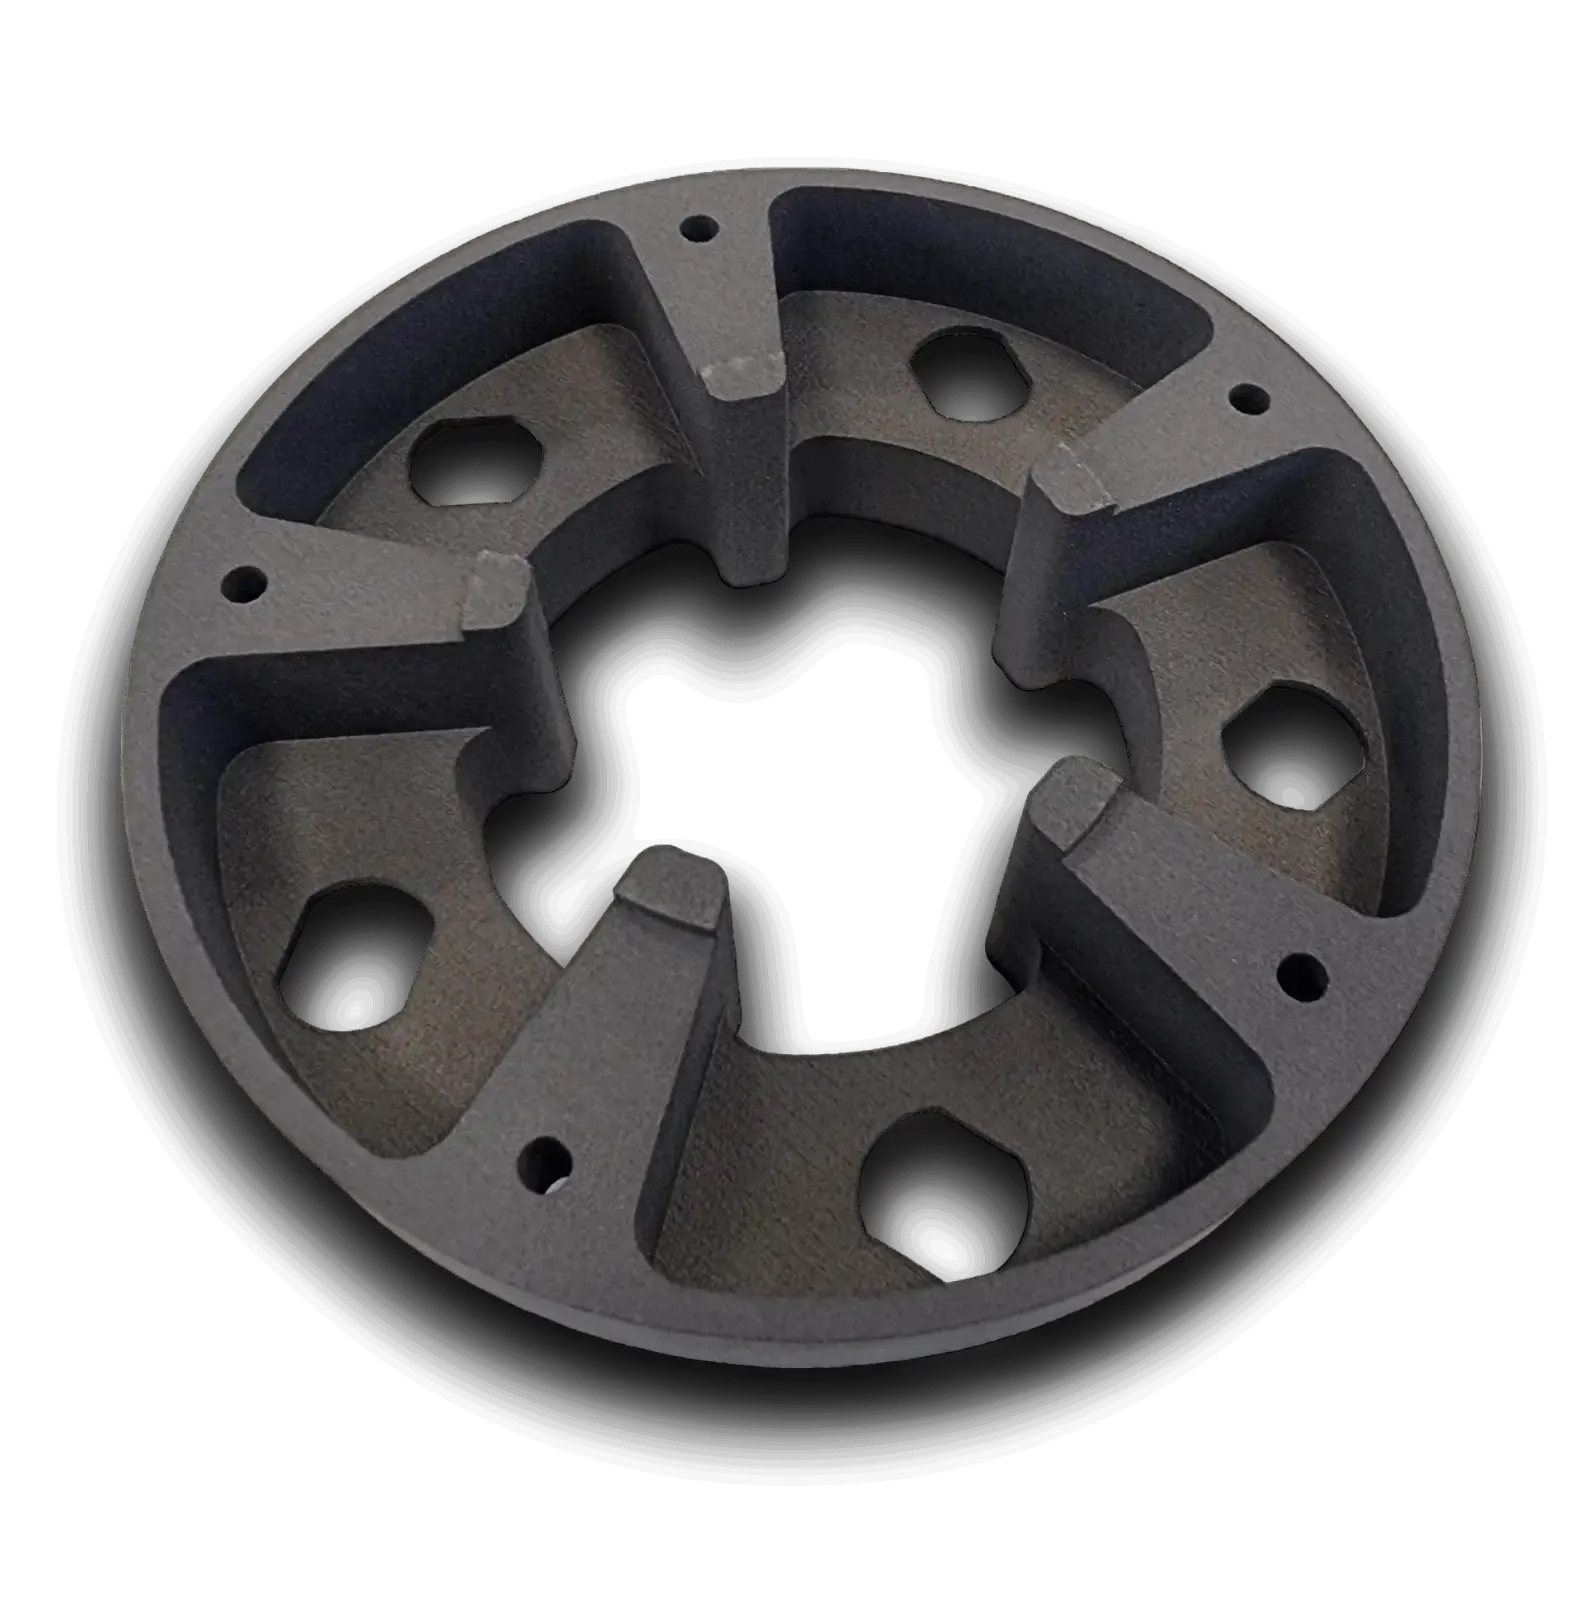
Why nylon behaves differently from metal
Polyamide is a semi-crystalline thermoplastic. Half of it is ordered crystal, half is loose amorphous chain. That split explains almost everything you see at the spindle: good stiffness in thin walls, poor stiffness everywhere else, and a springy chip that wraps the tool instead of breaking.
The amorphous half absorbs water from the air. PA6 can take up 2.5–3% of its own weight in moisture at 50% relative humidity; PA66 sits slightly lower and PA12 stays under 1%. Water molecules push the chains apart, so the part swells. A 100 mm PA6 bar can grow 0.2–0.3 mm across that range. No machine accuracy fixes that after the fact.
Heat is the second problem. Nylon has low thermal conductivity, roughly 0.25 W/m·K, so cutting heat stays at the edge. Above about 80 °C the material softens, smears and drags. You get melted burrs, a cloudy surface, and a dimension that shrinks back as the part cools.
Add internal stress from the extrusion process itself. Billet that was quenched after extrusion holds locked-in stress. Remove 3 mm from one side and the part bows. This is not tool deflection. It is the material finding a new balance.
Choosing between PA6, PA66 and PA12
PA6 is the workhorse. It has the highest impact strength of the three and the best wear resistance, so it suits bushings, wear pads, rollers and gears that see shock. Its downside is moisture. If the part runs dry and the drawing calls for tight tolerance, PA6 will fight you all year.
PA66 is stiffer and has a higher melting point, around 255 °C against 220 °C for PA6. That matters for parts near a motor or a heat source. It is also more creep-resistant under sustained load. It still absorbs moisture, just a little less, and it is noticeably harder on tooling than PA6.
PA12 is the dimensional one. Water uptake under 1% means a PA12 part holds size across seasons and shipping routes. It also machines to the cleanest finish. The trade-off is price and lower mechanical strength, so it belongs on precision spacers, fluid manifolds and parts that must stay on a CMM print.
Cast nylon, often sold as MC nylon, is a fourth option. It has higher crystallinity than extruded stock, so it is harder and wears longer, but it is only available in thick sections and machines with more internal stress. For thin plates and small turned parts, extruded stock is the safer pick.
- 1Pick PA6Impact loads, wear surfaces, cost-sensitive runs.
- 2Pick PA66Higher service temperature and creep resistance needed.
- 3Pick PA12Tight tolerance across humidity and long shipping cycles.
- 4Skip nylonContinuous UV exposure or sustained load above 90 °C.
Feeds, speeds and tooling that work on PA
Use sharp, polished, uncoated carbide. A mirror-flute geometry lifts the chip instead of rubbing it. Two flutes for slotting and deep pockets so the chip has room to clear; three flutes for finishing passes where you want a smoother surface. Avoid heavy TiAlN coatings, which add edge radius and generate heat on plastic.
Run surface speed in the 200–500 m/min range. That sounds fast for plastic, but nylon needs the edge to slice, not to push. A slow spindle with a heavy chip load rubs the material, heats it, and produces the stringy melt you see on a bad part. Feed per tooth of 0.05–0.15 mm keeps the cut cool.
Keep radial engagement modest, 20–40% of tool diameter, and use climb milling. Conventional milling on nylon pulls the workpiece into the cutter and leaves a fuzzy edge. Axial depth of cut of 0.5–1.5 × tool diameter is safe on rigid setups; reduce it in thin walls where the part deflects.
Air blast beats flood coolant on PA. Compressed air clears chips and carries heat away without adding moisture. If you must use coolant, use a synthetic or oil-based type. Water-based flood coolant is the wrong choice because the part absorbs it and changes size after the vise is released.
What tolerance is realistic on nylon parts
On a conditioned PA12 part measured in a 20 °C room, ±0.05 mm is routine and ±0.02 mm is achievable on a stable feature. Pushing to ±0.005 mm on nylon is possible on a short, thick-walled feature with the right grade and a stress-relieved billet, but it is not a blanket callout. Put the tight tolerance only where the function needs it.
Thin walls are the trap. A 1.5 mm PA6 wall in a 100 mm part will move more than any cutting strategy can control. If the design allows, thicken the wall or add a rib. Stiffness scales with the cube of wall thickness, so 2.5 mm instead of 1.5 mm changes the picture completely.
Measure after stabilization, not off the machine. A part that reads 50.02 mm hot can read 49.95 mm the next morning. We inspect 100% before shipment, but we schedule the inspection after the part has had time to equalize with the shop atmosphere.
Surface finish follows the same logic. Ra 0.8–1.6 μm is normal on a finished PA face. Ra 0.2–0.8 μm is reachable with a light finishing pass and a sharp tool, though the surface whitens if you push too hard. A cloudy white patch means heat, not a better finish.
Step by step: from billet to finished PA part
Six steps that cover most nylon jobs we quote.
- 1Dry the stockHold PA pellets or billet at 80 °C for 3–4 hours in a desiccant dryer, or store billet in a sealed bag with desiccant. Target moisture below 0.2% before the first cut.
- 2Stress-relieveFor parts with tight flatness, anneal the billet at 150–160 °C for 2 hours, then cool at no more than 20 °C per hour. This releases extrusion stress before you remove material.
- 3Rough with stock onLeave 0.8–1.5 mm of radial stock on all faces. Rough at 200–350 m/min, 0.08–0.12 mm per tooth, air blast on.
- 4Rest before finishingLet the roughed part sit for 4–12 hours so it can absorb ambient moisture and settle. Finishing a hot part guarantees it moves after inspection.
- 5Finish lightTake 0.15–0.4 mm radial passes at 300–500 m/min. Climb mill, sharp uncoated tool, air blast. Measure with a light touch; vernier pressure deforms PA.
- 6Deburr and packScrape edges with a sharp blade rather than a file. Bag the part with desiccant the same day so it arrives at the same moisture state you measured.
Nylon grades and process choices compared
Match the grade and cutting method to the job, not to habit.
| Grade / method | Best for | Moisture uptake | Watch out for |
|---|---|---|---|
| PA6 extruded | Wear pads, rollers, impact parts | About 2.5–3% | Size change over seasons |
| PA66 extruded | Stiffer parts near heat | About 1.5–2.5% | Harder on tool edges |
| PA12 extruded | Precision spacers, manifolds | Under 1% | Higher material cost |
| Cast MC nylon | Thick wear plates | About 2–3% | More internal stress |
| Air blast cooling | All grades, most jobs | No added moisture | Needs good chip extraction |
| Water-based coolant | Not recommended | Absorbed by part | Post-cut growth, stains |
When nylon is the right call
Choose PA12 when the part must hold tolerance through humidity and shipping. Choose PA6 or cast nylon when wear and impact matter more than a few hundredths of a millimeter. Choose metal when the part runs hot, sits in sunlight, or carries a sustained structural load. Nylon wins on weight, cost and sliding wear. It loses on thermal and dimensional stability, every time.
Nylon machining questions we get weekly
Can you hold ±0.005 mm on nylon parts?
On a short, rigid feature in PA12 with a stress-relieved billet, yes. Our general machining tolerance is ±0.005 mm, and we hold it on metal parts every day.
On long or thin-walled PA6 features, that number is not honest. We will tell you which callouts are realistic and which need a design change.
Do you anneal nylon parts after machining?
When the drawing calls for flatness or tight bore tolerance, we anneal before machining at 150–160 °C, and sometimes run a second low-temperature cycle after roughing.
Annealing after final machining is rare because it can shift the finished size. We prefer to relieve stress before the finishing passes.
What surface finish should I expect on a machined PA surface?
As-machined faces land around Ra 1.6–3.2 μm. A proper finishing pass with a sharp uncoated tool gets Ra 0.8–1.6 μm.
Going below Ra 0.8 μm on nylon is possible but the surface can whiten. If you need a glossy look, polishing is a better route than chasing a lower Ra number.
Can nylon parts be painted, laser marked or bonded?
Laser marking works well; we set minimum character height at 1.5 mm so the mark stays legible on a slightly fuzzy plastic surface.
Painting and bonding need a surface preparation step because polyamide has low surface energy. Tell us the requirement and we will plan the process before cutting.
How do I keep a PA6 part from growing after shipment?
Specify PA12, or accept the growth and design the fit with clearance. There is no coating that stops moisture uptake in a polyamide.
We dry and bag parts with desiccant, but a humid warehouse will still move a PA6 part over months. Design for that reality.
What is the smallest quantity you will machine in nylon?
One part. We have no minimum order quantity, so a single prototype and a 10,000-part run both go through the same process control.
Uploads are secure and confidential, and we can sign an NDA before you send drawings.
Send us your nylon part drawing
We review the geometry, the grade and the tolerance stack, then send a quotation with free DFM analysis within 12 hours.
12-hour quoteNo minimum order quantity100% inspectionNDA on request
More on materials and machining
We publish setup notes, tooling trials and inspection data from the factory floor.











