
01
Thickness drifts across the lot
Parts arrive at 1.08 mm on one end of the box and 0.94 mm on the other. Your press shims change every run and the assembly height moves. Sorting 10,000 pieces by hand costs more than the parts.
GreatLight machines the 25mmx1mm metal slug into finished components on 127 CNC machines in Dongguan. Tolerance ±0.005 mm, 100% inspection before shipment, and runs from one piece to 10,000+ parts.

A 25 mm disc that is 0.05 mm thick or 0.1 mm oval will not sit flat in your fixture.
Parts arrive at 1.08 mm on one end of the box and 0.94 mm on the other. Your press shims change every run and the assembly height moves. Sorting 10,000 pieces by hand costs more than the parts.
A rolled edge stops the slug from seating flat. Operators spend time filing each disc, or the part sits proud and the stack tilts. Deburring has to be in the process, not an afterthought.
If the Ø25 mm circle turns out 0.08 mm out of round, an automatic feeder jams. The machine stops. Someone clears it. This repeats all shift.
Your customer asks for 304 or 6061 traceability and the supplier sends a packing slip. Without a mill cert and inspection report, the batch cannot ship.
One page, one part family: flat round blanks near Ø25 × 1 mm, machined to your drawing.

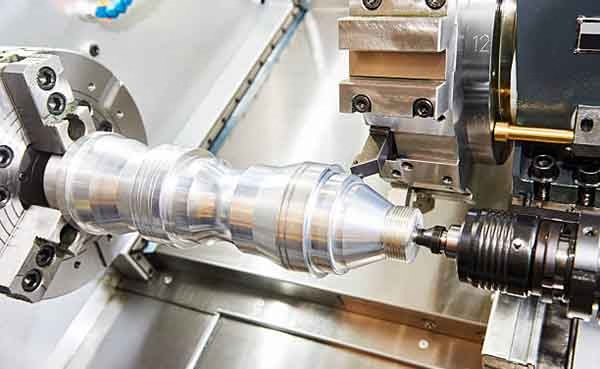
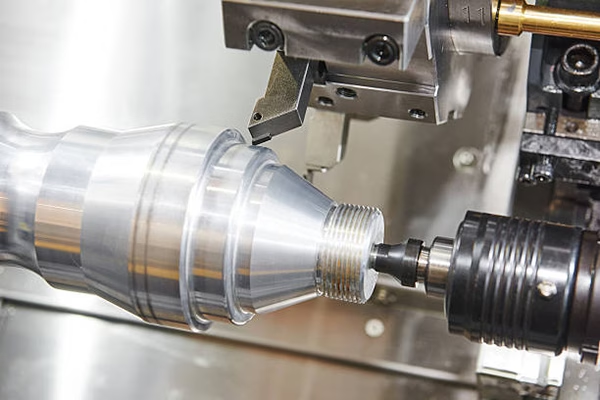
We start from bar, plate, or pre-cut slug stock and face both sides on a lathe or mill-turn center. Holding a 1 mm thick disc flat is the whole problem. Thin parts deflect under clamping pressure and spring back when you release them. We use soft jaws, vacuum fixturing, or a sacrificial carrier plate depending on the feature pattern.
Once the blank is stable, we machine the OD, any bore, chamfers, and face features in the same setup where possible. Fewer setups means fewer chances for the part to move between operations.

The slug goes onto a 3-axis, 4-axis, or 5-axis mill depending on the feature count. A single hole and chamfer is a 3-axis job. A ring of holes on a bolt circle, or features on both faces, belongs on a 4-axis or 5-axis machine so the part is not re-clamped. Our shop runs 16 simultaneous 5-axis centers and 16 mill-turn centers for exactly this kind of small, near-net part.
Inspection is not a final step only. We check the raw material certificate on arrival, monitor thickness and diameter in process, and inspect 100% of parts before shipment. Reports are available on request.
Pick by feature count and volume, not by habit.
| Situation | Recommended process | Why |
|---|---|---|
| Plain disc, tight thickness | CNC turning or mill-turn | Faces come parallel in one setup |
| One center hole and chamfer | 3-axis milling | Short cycle, simple fixture |
| Bolt circle or side features | 4-axis or 5-axis milling | No re-clamping between faces |
| Thin disc, tight flatness | Vacuum fixture on 5-axis | Even clamping, less deflection |
| Prototype, 1 to 20 pcs | Mill or lathe, no tooling | No minimum order quantity |
| Volume 10,000+ pcs | Mill-turn with bar feeder | Lower cost per part |
The same shop floor handles the slug and everything around it.
16 simultaneous 5-axis centers. Multi-face features on one part without moving the datum. Fits slugs with holes on more than one face.
3-axis, 4-axis, and mill-turn capacity. Ø400 mm rotary table for bolt circles. Turning for round slugs with a bore.
One to twenty pieces, no tooling charge. Good for checking fit before committing to a 10,000 piece run.
Anodizing, electroless nickel, zinc plating, black oxide, bead blasting, and laser marking from 1.5 mm character height.
For flat parts that start as sheet rather than bar. Bending, punching, and hardware insertion.
When the slug becomes a housing or bracket at higher volume, we can quote casting plus machining.
Numbers you can plan a purchase order around.
| Item | Range | Notes |
|---|---|---|
| Maximum part size | 4,000 mm | Larger travels on select machines |
| Achievable tolerance | ±0.005 mm | ±0.0002 in |
| Surface finish | Ra 0.2–3.2 μm | As-machined to fine |
| Aluminum | 6061, 6082, 7075, 2024 | Plus 5052, 5083, 6063, ADC12 |
| Stainless | 303, 304, 316L, 17-4PH | Plus 420, 430, 440C |
| Copper and brass | C101, C110, C36000 | Beryllium copper available |
| Titanium and special | TC4, Inconel, AZ31B | TA1, TA2, AZ91D |
| Plastics | POM, PEEK, PA, HDPE | ABS, PC, PMMA, PP |
We quote the tolerance we can hold across the lot, not the best single part off the machine. If your drawing needs tighter than that, we say so before the run starts.
Send a drawing and we return a quotation plus a free DFM analysis within 12 hours. Production can start within 24 hours of approval.
Raw material check, in-process monitoring, and 100% final inspection before shipment. Reports on request, not on request only after a problem.
ISO 9001:2015, IATF 16949:2016, ISO 13485:2016, and ISO 27001:2022. Your drawings stay under NDA on request.
One prototype and a 10,000 piece run use the same process sheet. No tooling charge for the first small batch.
Three wholly-owned plants in Dongguan and a factory in Singapore. 150 technicians on the floor.
Sensor shims and spacer discs that must repeat run to run. IATF 16949 process control applies.
Flat discs for instrument assemblies. Material traceability and clean deburring matter more than speed.
Contact discs and heat-spreader blanks in copper and aluminum. Flatness drives thermal contact.
Feeder and gripper discs where an oval OD jams the line. Diameter consistency is the whole spec.
It describes a flat round blank roughly Ø25 mm across and 1 mm thick. That is a common starting size, not a fixed standard.
If your part is 24.6 mm or 25.4 mm, we machine to your drawing. Send the dimension and tolerance you actually need and we quote against that.
Yes, on thickness, diameter, and machined features, provided the fixture controls deflection. Thin parts move when clamping pressure is uneven.
That is why we use soft jaws, vacuum plates, or a carrier plate. If the geometry makes ±0.005 mm unrealistic, we tell you before the run, not after.
Aluminum 6061, 6082, 7075, and 2024; stainless 303, 304, 316L, and 17-4PH; copper and brass including C110 and C36000; titanium TC4; and plastics such as POM and PEEK.
Beryllium copper and Inconel are also available. Tell us the material on the drawing and we confirm stock before quoting.
No. We run from one prototype to 10,000+ piece runs on the same process sheet.
Small batches go on the mill or lathe without tooling. Higher volumes move to mill-turn with bar feeding to cut cost per part.
Deburring is planned into the process, not added at the end. We control the chamfer or edge break in the cut where the geometry allows.
For softer materials we follow with tumbling or bead blasting. Every part is checked for a rolled edge before packing.
Raw material certificates are checked on arrival. Thickness and diameter are monitored in process, and 100% of parts are inspected before shipment.
Dimensional reports, material certificates, and first article inspection reports are available on request.
Quotation and free DFM analysis come back within 12 hours. Production can start within 24 hours of approval, and parts typically ship in 3–5 days.
Lead time depends on material availability and finishing. Anodizing or plating adds a step outside the machine shop.
Yes. We sign an NDA on request, and uploads are kept secure and confidential by default.
We hold ISO 27001:2022 for information security, which covers how we store and handle customer files.
Upload the file and we return a quotation with DFM feedback within 12 hours. No minimum order quantity, no tooling charge for the first batch.
12-hour quote100% inspectionNo MOQNDA on request
Trusted by engineers and manufacturers worldwide










Upload your 3D model or 2D drawing and get a quotation with a free DFM analysis. Maximum processing size 4,000 mm.
CNC Metals 13 grades
CNC Plastics 10 grades
Machines & processes 12 options
Surface & post-processing 10 options
Material: not selected Machine: not selected Post-process: not selected
Fill in this short form and we'll open WhatsApp with your message ready to send. We only use these details to reply to you.
Nothing is sent until you press send inside WhatsApp.