
Cheap Bulk 4 Axis CNC Machining Wholesale
This page is for engineers and buyers who need volume 4-axis milled parts and want to know where the cost actually comes from. It covers fixtures, materials, process integration and the quoting signals that separate a low unit price from a low total cost.
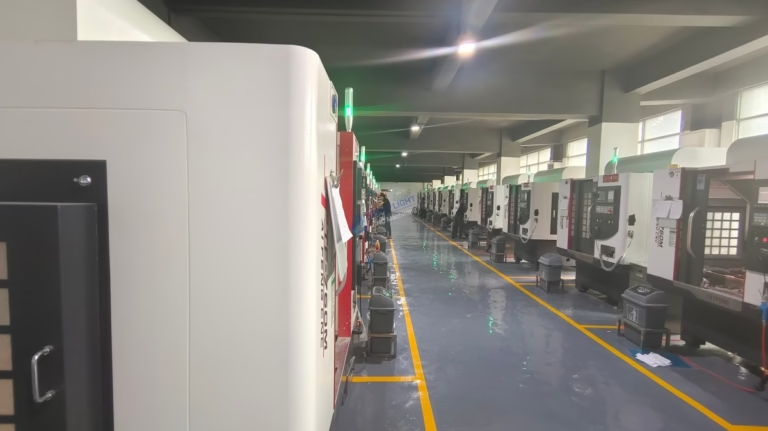
What Drives Unit Cost Down at Volume
Price per part is mostly a fixture and programming story. The machine hour rate matters far less than how many times a part gets touched.
Why the Fourth Axis Pays for Itself in Bulk
On a 3-axis mill the workpiece stays on the table and the tool moves in X, Y and Z. Any feature on the side or the back of the part means you unclamp, rotate or flip the block, clamp again, re-zero, and cut. Across a 10-part prototype run that is annoying. Across a 2,000-part run it is the dominant cost, because every extra setup multiplies against every part.
A 4-axis machine holds the part in one fixture and indexes it with a rotary table, so faces that would need separate operations come off in the same cycle. Fewer clamps means less labour per part, less scrap from re-datum errors, and a shorter queue at the machine. Setup reduction is the single largest lever on bulk unit price.
Tolerance also gets easier to hold. When the part never leaves the fixture, the datum does not move between operations, so concentricity and angular position between faces stay inside ±0.005 mm without hand work. That matters on parts with bores and slots on more than one face, where a re-clamp error of 0.02 mm is enough to fail a gauge.
Where a fourth axis does not help is a flat plate with features on one face only, or a part so large it fills the whole travel. In those cases a 3-axis machine with a good fixture is cheaper and just as accurate.
- 1Good fitBores, slots or flats on 2-4 faces of one part
- 2Good fitRuns of 100 to 10,000+ identical parts with one fixture
- 3Poor fitSingle-face plates and very large weldments
- 4Poor fitOne-off parts where fixture cost cannot be spread
Design for Fixturing Before You Ask for a Quote
A bulk price is only as stable as the fixture that holds the part. If the model has no flat face to sit on, no repeatable edge to locate against, or walls that flex under 8 bar coolant, the shop has to build something soft and slow. That cost lands in every unit.
Give the shop one clean primary datum and a second feature for rotation. Add a boss, a web or a thicker wall where the vise jaws or a collet will grip. A 1 mm increase in wall thickness around a clamping zone often removes a support operation entirely.
Threads and small holes deserve attention too. A tapped hole that lands on a curved surface needs a spot face, and a spot face on a 3-axis machine is another setup. If the hole can sit on a flat, the fourth axis drills and taps it in the same index.
We run DFM on every file before quoting, so fixture problems surface before the first chip. Send a STEP file and you get the fixture notes back with the price, not after the first article.
- 1One datumPick a face that stays flat through all operations
- 2Grip zoneAdd material where the fixture will clamp
- 3Rotary clearanceCheck that the part clears the table through 360°
Material Choice and Its Effect on Bulk Cost
Same geometry, four different materials. Tool life and cycle time move more than the raw stock price does.
| Material | Typical use | Machining note |
|---|---|---|
| Aluminum 6061-T6 | Brackets, housings, heatsinks | Fast, low tool wear, holds ±0.005 mm easily |
| Aluminum 7075 | High-strength structural parts | Stiffer, slightly tougher on cutters than 6061 |
| Stainless 304 / 316L | Food, medical, marine parts | Work hardens; needs slower feeds and sharp tools |
| Stainless 17-4PH | Shafts, valve bodies | Often machined in condition H1025 or annealed |
| Steel 4140 | Gears, tooling, load-bearing parts | Pre-hardened stock cuts slower than mild steel |
| POM / PEEK | Insulators, bushings, seals | Low cutting force; watch thermal growth on PEEK |
| Titanium Ti-6Al-4V | Aerospace and medical | Roughly 3-5× the cycle time of aluminum 6061 |
Reading a Bulk Quote: What the Numbers Hide
A low unit price on a 4-axis part usually means one of three things. The shop has a fixture already running, the volume break is real and tied to a setup amortised over thousands of parts, or the quote has left something out. The third case is the expensive one.
Ask what is included. A transparent bulk quotation lists the material grade and stock form, the number of setups, the fixture cost and whether it is charged once or per run, the finish and its masking, inspection level, packaging, and the incoterm. If a line is missing, assume it will appear later as a change order.
Volume breaks should step down where the real cost steps down. If the price drops 30% between 100 and 1,000 parts, the setup must have been a large share of the first quote. That is normal and healthy. A flat price from one part to 10,000 parts usually means the small quantity was quoted high to protect the shop.
Tolerance is the other hidden line. A drawing that calls ±0.005 mm on every dimension in the title block will be quoted as a fully inspected part, even where only two features need it. Mark the critical dimensions and let the rest run to general tolerance. The cycle time does not change. The inspection time does.
Lead time claims deserve the same reading. Anyone can promise a date in an email. Ask how the schedule is tracked and what happens when a machine goes down. We keep a historical late-delivery probability below 2% by scheduling the fourth-axis cells ahead of the finishing queue, not by promising faster.
- 1CheckMaterial grade and stock form listed by name
- 2CheckFixture cost shown once, not hidden in unit price
- 3CheckCritical dimensions marked separately from general tolerance
- 4CheckIncoterm, packaging and inspection level stated
Process Integration and Where It Stops Being Worth It
Bulk affordability comes from finishing the part in as few places as possible. A 4-axis cell that mills, drills, taps and chamfers in one cycle removes transport, queue time and a second setup error. Add deburring at the machine and the part goes straight to finishing.
Integration has a limit. Hardened steel parts may need heat treatment between roughing and finishing, and that means two machining operations with a furnace in the middle. Anodizing, plating and powder coating are separate lines regardless of how the part was cut. The question is whether those steps are planned into the route or bolted on afterwards.
Surface finish follows the same logic. As-machined at Ra 1.6-3.2 μm comes off the cutter. Ra 0.8-1.6 μm usually needs a finishing pass with a smaller stepover. Ra 0.2-0.8 μm on a bulk run needs a deliberate plan, because hand polishing does not scale and its cost is linear with quantity.
Our three plants cover milling, turning, finishing and inspection under one roof, which is why a 4-axis batch can move from raw bar to packed carton without an outside vendor adding a week to the route.
Inspection That Catches Errors While the Spindle Is Still Turning
Final inspection finds bad parts. In-process measurement stops making them. On a bulk 4-axis run the difference is a few thousand scrap parts versus a few dozen.
A workable plan starts with the raw material certificate, then a first-article check against the drawing before the run is released. From there the operator gauges critical features at a fixed interval, and the CMM verifies the same features at the end. If a dimension drifts, the offset is corrected at the machine.
Certification matters as a floor, not a selling point. ISO 9001:2015 shows a documented system. IATF 16949:2016 applies to automotive work, ISO 13485:2016 to medical devices. If your part needs one of those, the supplier either holds it or does not.
Every part is inspected before shipment at GreatLight, and inspection reports go out on request with the batch. That is a documented routine, not an upsell.
- 1Raw materialCertificate checked against the specified grade
- 2First articleFull drawing check before the run is released
- 3In processOperator gauging at set intervals on critical features
- 4FinalCMM verification and report on request
Questions Buyers Ask Before a Bulk 4-Axis Run
How many parts do I need before 4-axis machining is cheaper than 3-axis?
It depends on the fixture, not the quantity alone. If a part has features on three or four faces, the fourth axis wins as soon as the fixture cost is spread over the run, often by a few hundred parts.
For a part with features on one face, 3-axis stays cheaper at any volume. Send the model and we will quote both routes so you can compare.
Can you keep ±0.005 mm across a 10,000-part run?
Yes, on features that are machined in one fixture without a re-clamp. Thermal drift and tool wear are the two things that move a dimension over a long run.
We control both with in-process gauging at fixed intervals and cutter compensation offsets at the machine.
What is the smallest and largest part you can run on a 4-axis mill?
Our 4-axis cells handle parts down to a few millimetres and up to 4,000 mm in length, with a Ø400 mm rotary table on the indexing side.
Very small parts are usually better on a mill-turn center, where the bar feed removes handling. We will say so if that is the case.
Do you charge for the fixture, and who owns it?
Fixtures are quoted as a one-time line item, separate from the unit price. That keeps the volume break honest and makes it clear what you are paying for.
Storage and ownership terms are agreed before the run starts. For repeat orders the fixture is already built, so the second run quotes lower.
What finishes can be applied without leaving the plant?
Anodizing in clear, colour, hardcoat and conductive types, electroless nickel and zinc plating, powder coating, black oxide, bead blasting, tumbling, brushing and polishing.
Laser marking is available down to 1.5 mm character height. Heavier coatings can affect tight tolerances, so masking is planned in the DFM step.
How do you handle confidentiality on a bulk program?
Uploads are kept secure and confidential, and we sign an NDA on request before any file review.
Drawings are shared only with the engineers and operators assigned to the job.
Send the Model, Get a Bulk 4-Axis Price
Upload your STEP file and get a quotation with DFM notes within 12 hours. No minimum order quantity, from one prototype to 10,000+ parts.
12-hour quote100% inspectionNo MOQNDA on request









